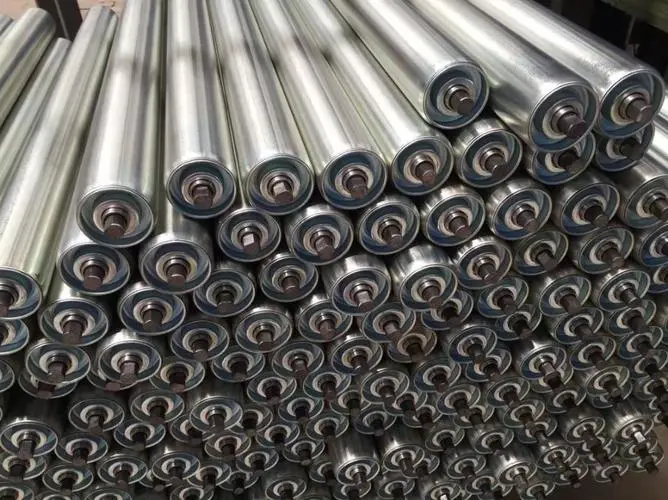
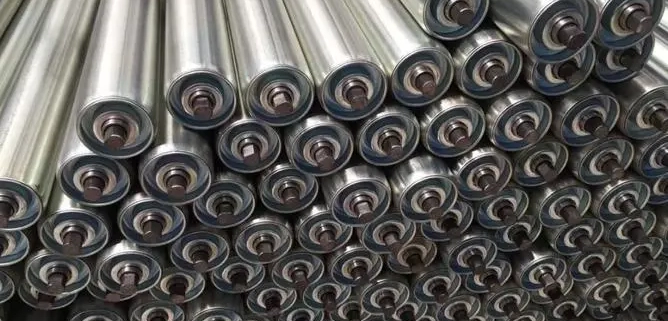
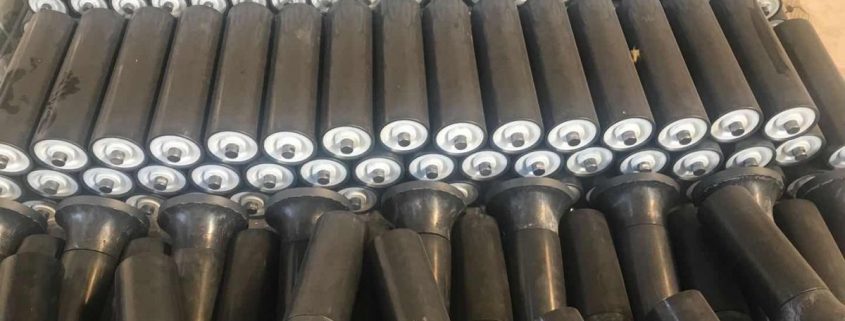
Steel conveyor rollers stacked with bearing ends and shaft interfaces visible

A pile of removed carrying rollers can look like a useful sample until nobody can say which unit came from the centre of a station and which came from an inclined wing. For a contractor replacing worn supports, the first task is preserving those positions. A belt conveyor carrying rollers supplier needs the retained station arrangement, the roller’s actual location and its mounting relationship before offering a replacement. Start with GRAM’s conveyor roller range, then separate the material and working-surface choices for each position.

The order should describe rollers for the conveyor that will receive them. It should not assume that every roller removed from the same belt is interchangeable. An ordinary carrying position, a loading position and a suspended linked group can require different supplied constructions even when the outside bodies appear similar.

Carrying roller positions must survive removal from the station

Identify the position before a removed roller becomes an anonymous workshop sample. The centre support and wing supports have different relationships to the belt and retained brackets. A photograph of the whole station, accompanied by a clear location reference, is more useful than several unlabelled close-ups of individual cylinders.

  1. Identify the conveyor and station in the plant’s existing equipment references.
  2. Mark the removed unit’s centre or wing location and the viewing direction used.
  3. Keep that location attached to the relevant dimensions and mounting details.

This key is not a new naming standard. Its purpose is to prevent the supplier and installer from assigning the same description to different physical positions. Use the plant’s established references where they are clear, adding a simple sketch where the existing record is incomplete.

The centre carrying roller belongs to the retained cross-section

The centre roller’s working length and shaft ends need to fit the actual supports that remain in service. Its position also contributes to the belt’s cross-sectional support. A replacement that fits between two brackets still needs to correspond to the intended carrying arrangement; bracket fit alone does not describe the whole station.

If the centre roller has been removed from a modified frame, record the modification instead of relying solely on an old general drawing. The supplier should receive the current accepted arrangement. Keep any disagreement between the drawing and measured retained equipment visible until it is resolved.

Wing roller descriptions need a clear side and viewing direction

An inclined wing roller can be misidentified when “left” and “right” are written from different viewpoints. Specify the orientation used in the sketch rather than expect the supplier to guess. Where the retained station uses identical wing units, that equivalence should come from its accepted construction, not from their similar appearance in a photograph.

A contractor should keep the ends of each sample identifiable as well. If an end feature or bracket relationship differs, rotating a sample for the photograph can conceal that difference. The separate discussion of roller locating dimensions helps define functional endpoints; the position record explains where that defined roller belongs.

A carrying rollers supplier should separate body material from station identity

Once the locations are clear, compare the actual body and end constructions offered for them. GRAM has steel and polymer roller routes, but a shared carrying role does not establish an identical assembly. An alternative material should remain a distinguishable proposal tied to the same retained position.

Steel carrying rollers retain a body, bearing and shaft relationship

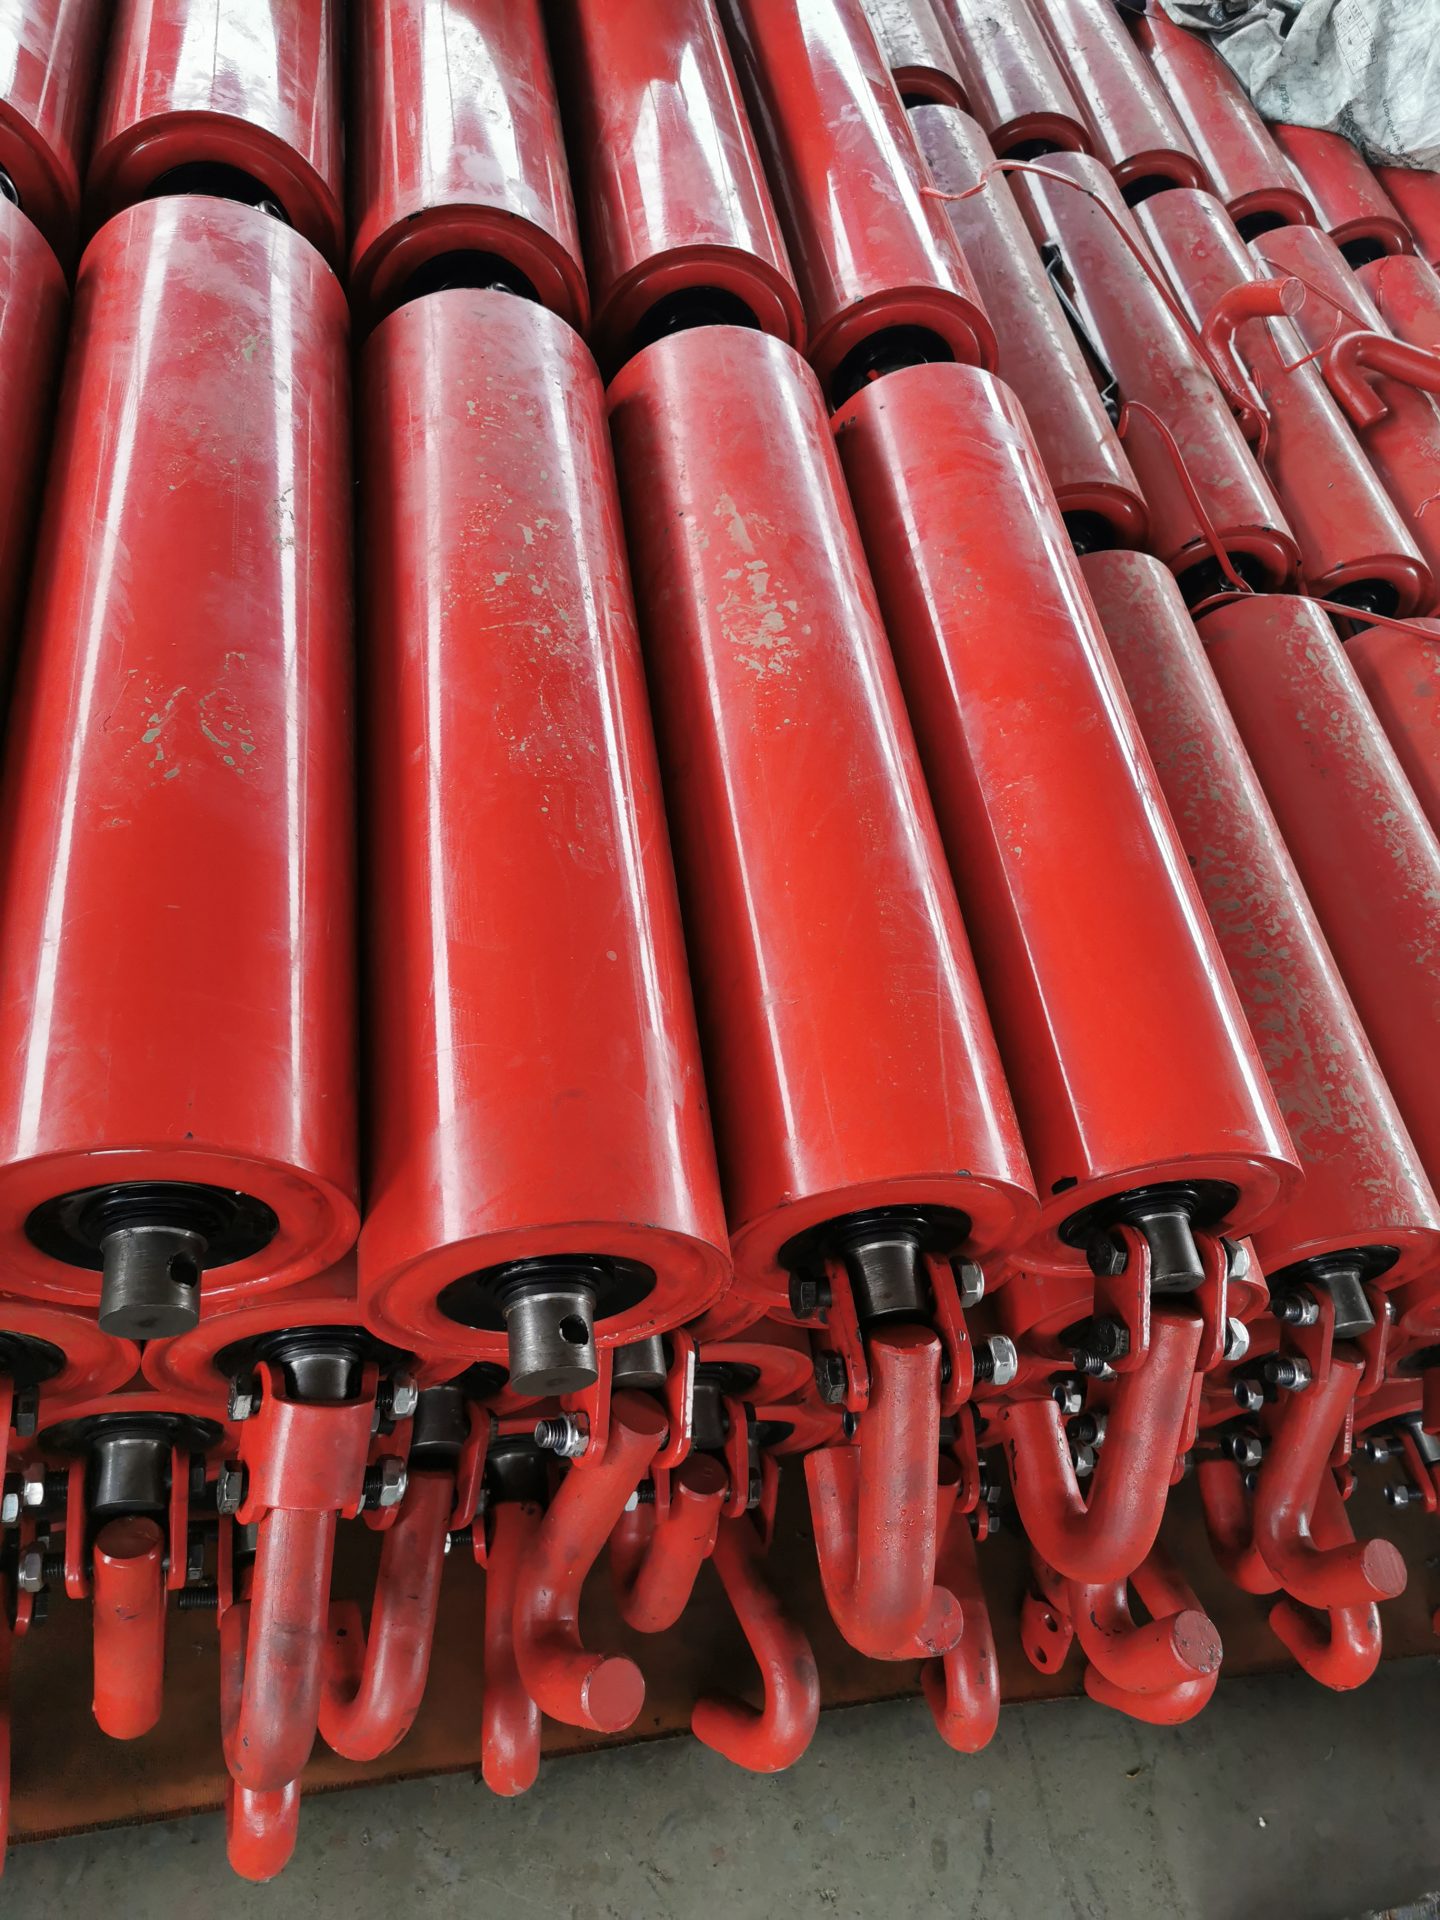
GRAM steel conveyor rollers use a cylindrical steel body rotating around a central axle, with bearings toward the ends and projecting shaft interfaces. Those are relevant construction details for a retained carrying position. They do not supply a universal load rating or an automatic match to every frame.

Specify the working body and the mounting ends as separate parts of the replacement description. A similar tube length can conceal different overall shaft dimensions. Conversely, matching shaft ends does not prove that the working body gives the intended belt support. The accepted offer needs both relationships.

GRAM polymer rollers showing a separate body material route for identified carrying positions
A material alternative should keep the retained position and mounting basis identifiable.

Polymer carrying rollers require an accepted complete alternative

The GRAM polymer roller description includes a machined polymer tube or solid bar, sealed precision bearings, non-contact rubber seals and metal end caps. These details help define what changes when the buyer considers a polymer body. They do not establish that every part of the assembled roller has the same environmental resistance as its body.

For a plant considering polymer wing rollers beside retained steel centre units, preserve the proposed mixed arrangement explicitly. Ask which positions the alternative covers and which remain unchanged. Do not infer a complete station approval from one material description, or assume that a lighter-looking body can replace a selected steel assembly without a position-specific review.

External descriptions of upper carrying and troughing arrangements illustrate why rollers and their support layout are considered together. That general engineering distinction is useful here; another manufacturer’s angles, frames and ratings are not specifications for the GRAM offer.

Loading-zone carrying positions need a separate working-surface decision

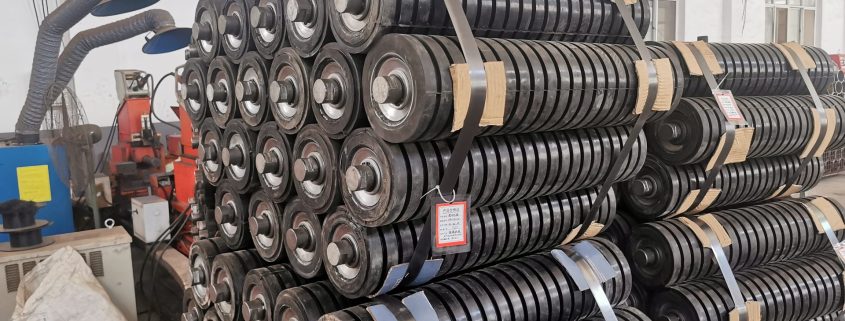
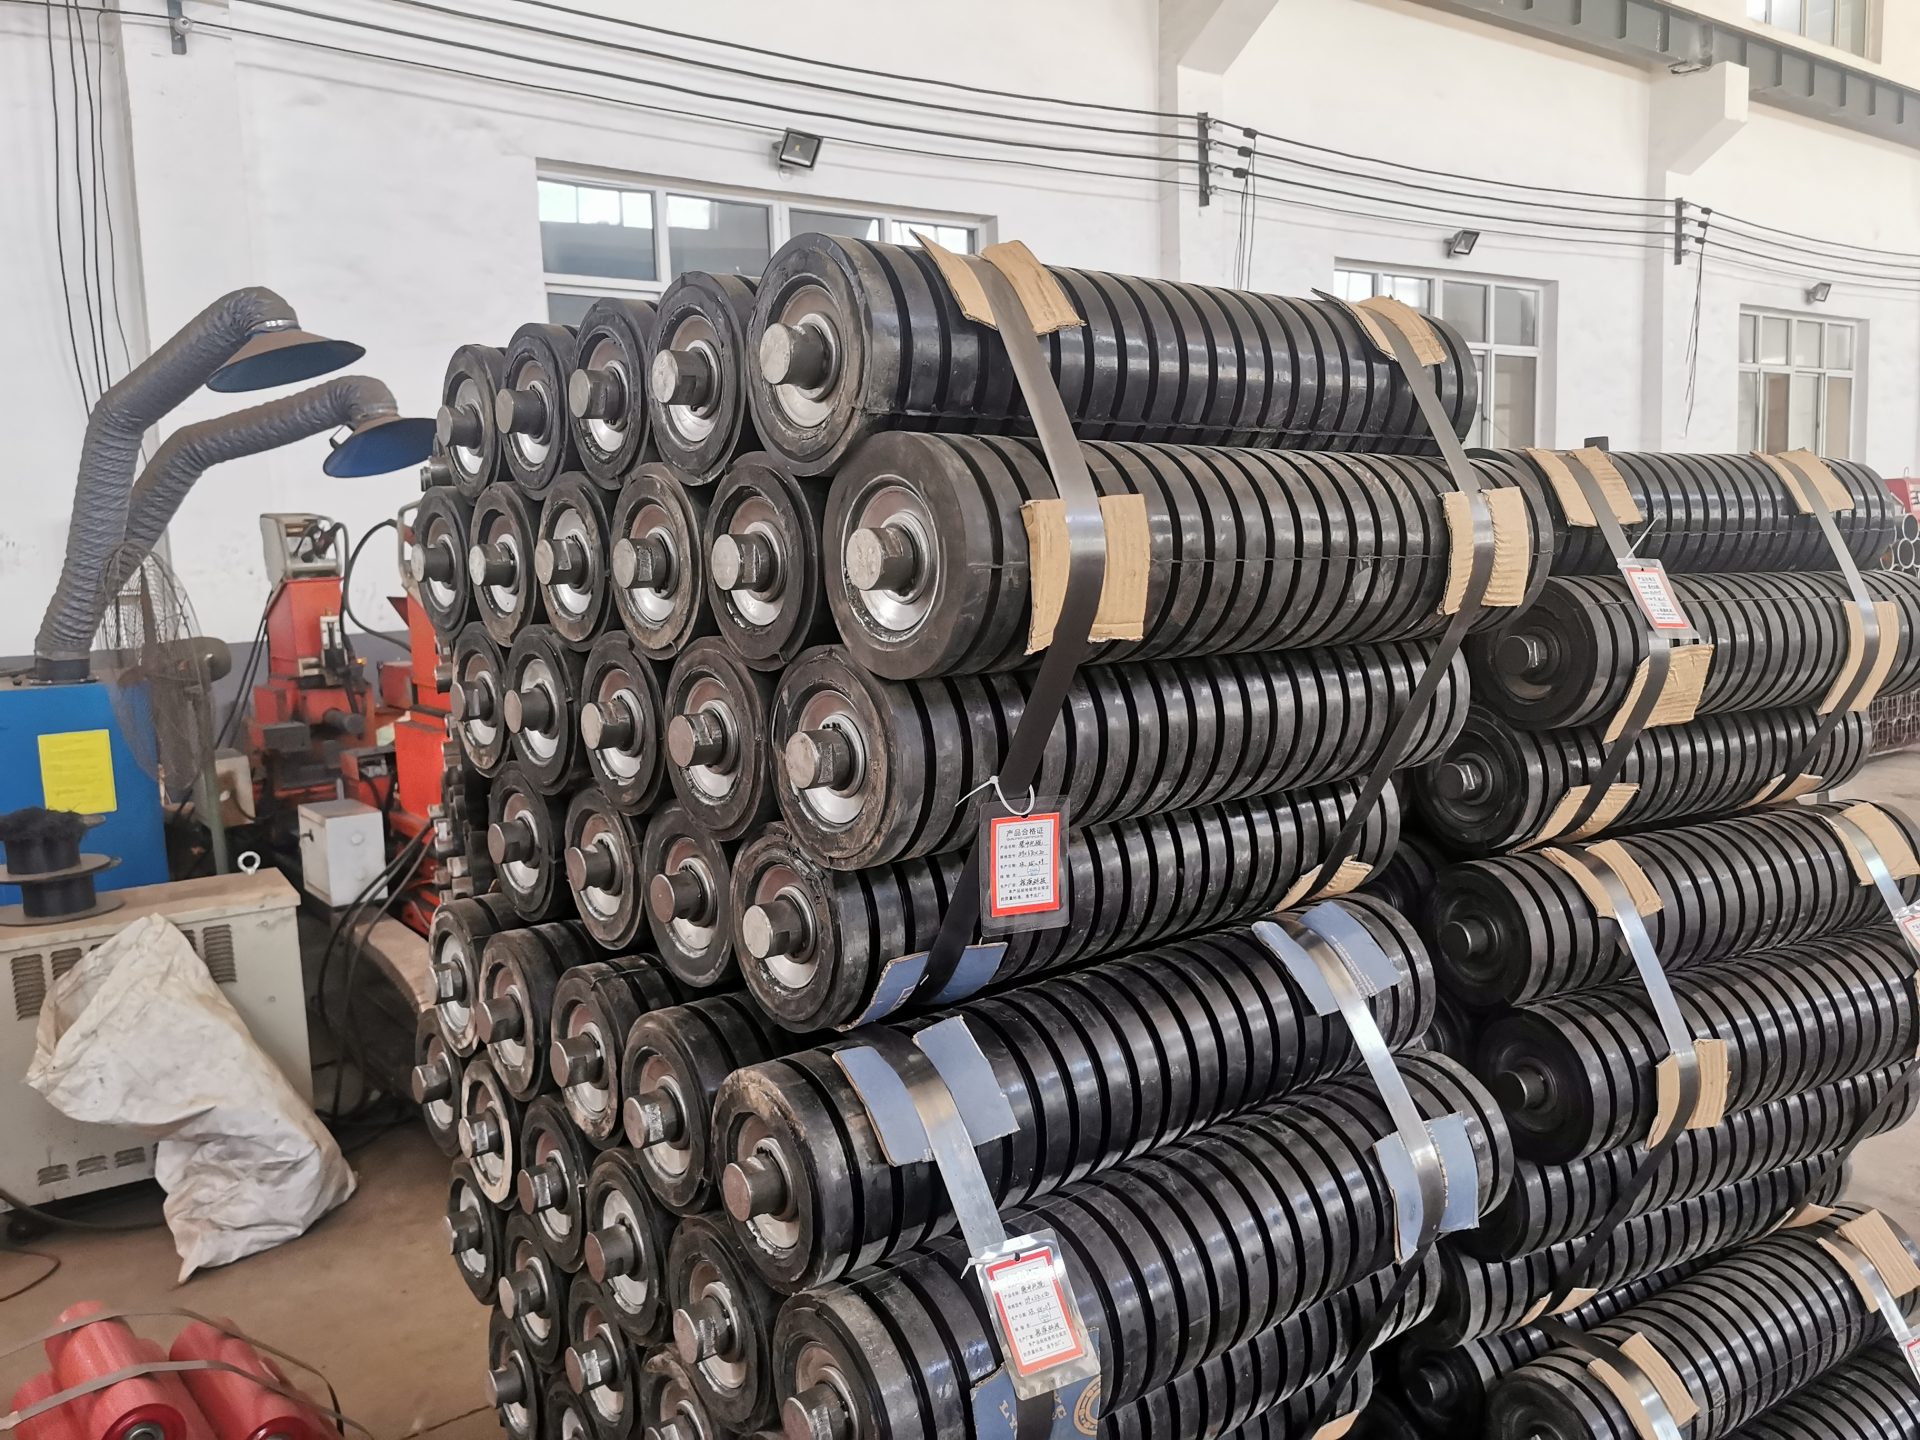
A carrying roller under incoming material is not automatically an ordinary carrying roller with a different location label. The loading duty can change the required working surface and support arrangement. GRAM’s rubber-ring impact rollers provide a distinct route for that discussion.

The rings belong to the belt-contacting working construction, while the underlying roller body and shaft ends still need to fit the accepted supports. Identify both. An outside ring diameter is not a substitute for the dimensions and relationships of the complete assembly.

A distributor combining an ordinary carrying order with loading-zone replacements should preserve those line items separately. Otherwise a request for “carrying rollers” can conceal a ringed construction that was expected at only a few stations. The supplier needs to know which duty the rings address, rather than add them to every position or omit them from the loading supports.

Where the plant changes the loading arrangement, the retained roller sample supplies mounting evidence but may not describe the new duty. Keep the revised material entry and support requirement alongside the sample identity. The responsible project team should accept the offered arrangement for that change; this article does not prescribe impact capacity or spacing.

Suspended carrying groups cannot be ordered as anonymous loose rollers

GRAM carrying garlands use connected rollers in a suspended group. The component’s location within that group and its connection relationship matter alongside its body dimensions. A loose roller from a garland should not be assigned to a rigid carrying station simply because it looks like a cylinder of the right size.
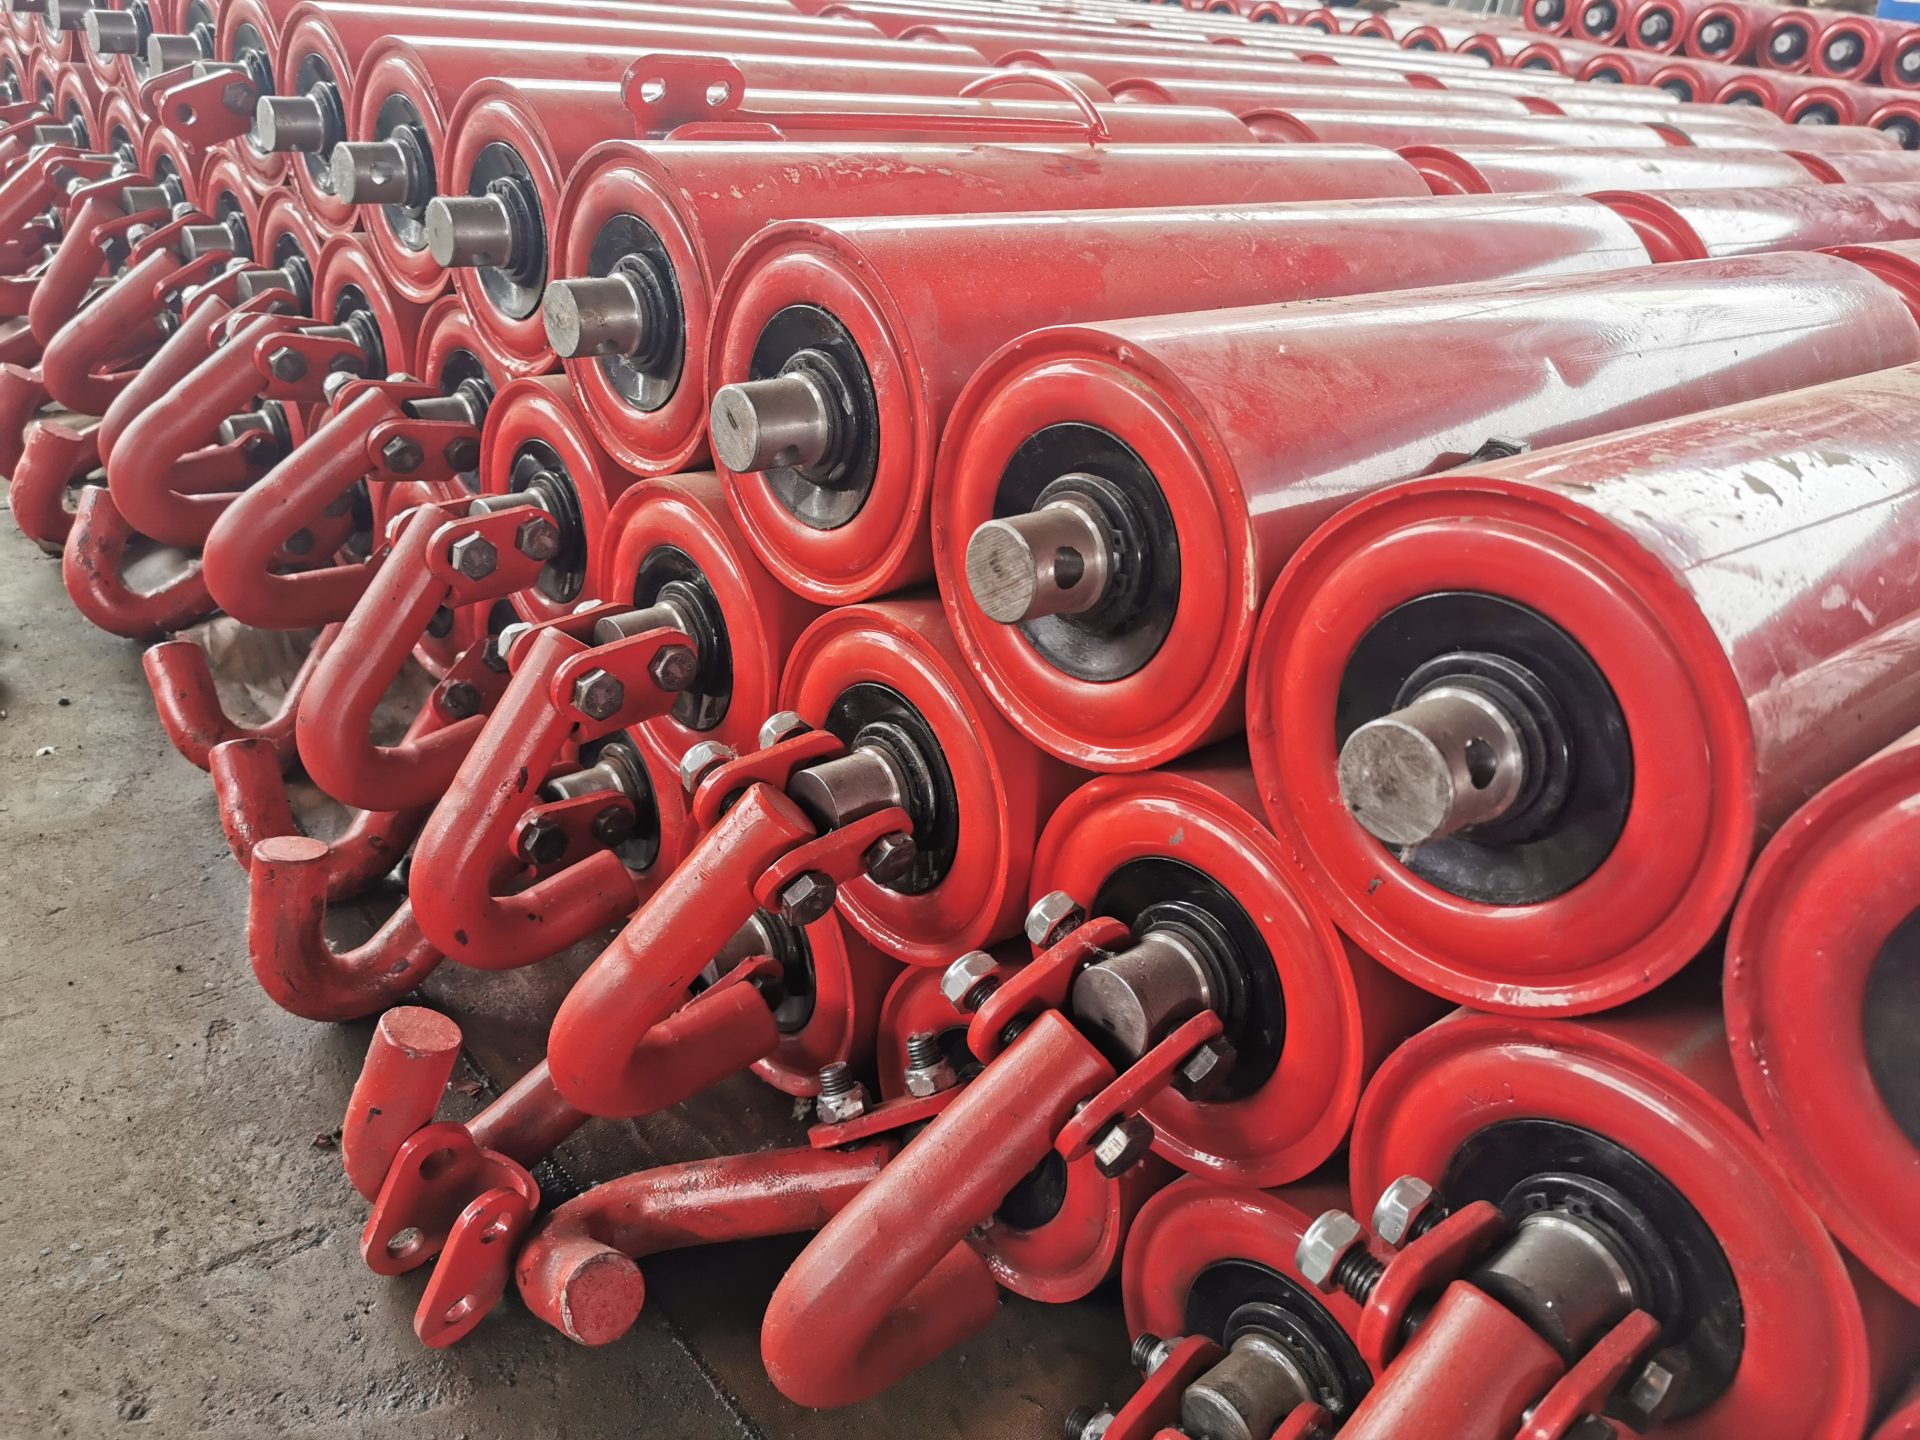
GRAM connected carrying garland with individual roller positions within the suspended group
Preserve the connected group as well as the identity of each roller being replaced.

If the buyer wants only part of an existing garland replaced, define the retained group and the connection scope of the supplied parts. If the entire group is being purchased, identify it as an assembly. The same photograph should not be used to imply that unspecified suspension hardware is included in both offers.

The receiving team also needs to distinguish loose components from complete supplied groups. Keep their references visible on the actual delivery information. Packaging details and grouping should be agreed for that order; a product photograph does not establish the supplier’s standard packing practice.

Carry the position key through the replacement order

Consider a shutdown order containing centre rollers for one conveyor and wing rollers for another. The tubes may appear similar on the workshop rack, while the shaft projections or bracket seats differ. Separate the destinations in the order even when the supplier groups their manufacture or transport. The contractor should be able to check a delivered item against its intended retained station without dismantling a second sample to rediscover the distinction.

If a loading station has several ringed rollers among neighbouring plain supports, mark where the ringed construction begins and ends in the accepted arrangement. A close-up of one impact roller cannot establish that boundary. The location sketch gives the supplier a reason for the different working surfaces and gives the installer a clear destination for each accepted item. Keep this as a component assignment record rather than a claim that the described transition has already been engineered for a changed feed.

Use the same location references in the quotation, accepted construction and receiving information. Where the supplier consolidates equivalent units into a single item, preserve the list of positions that equivalence covers. A contractor can then distribute the accepted replacement without recreating its identity at the conveyor.

When a delivery contains several similar roller bodies, the package identification should help separate centre, wing, loading and garland items according to the accepted offer. Agree that requirement before dispatch rather than assume an undocumented labelling service. It is a practical way to protect the position information already used to select the assemblies.

Resolve a position mismatch before treating a delivered roller as interchangeable. The useful purchasing decision is not simply “steel or polymer”; it is the accepted construction for a named place on the retained conveyor. Keep that place attached to the roller all the way from removal to the replacement order.
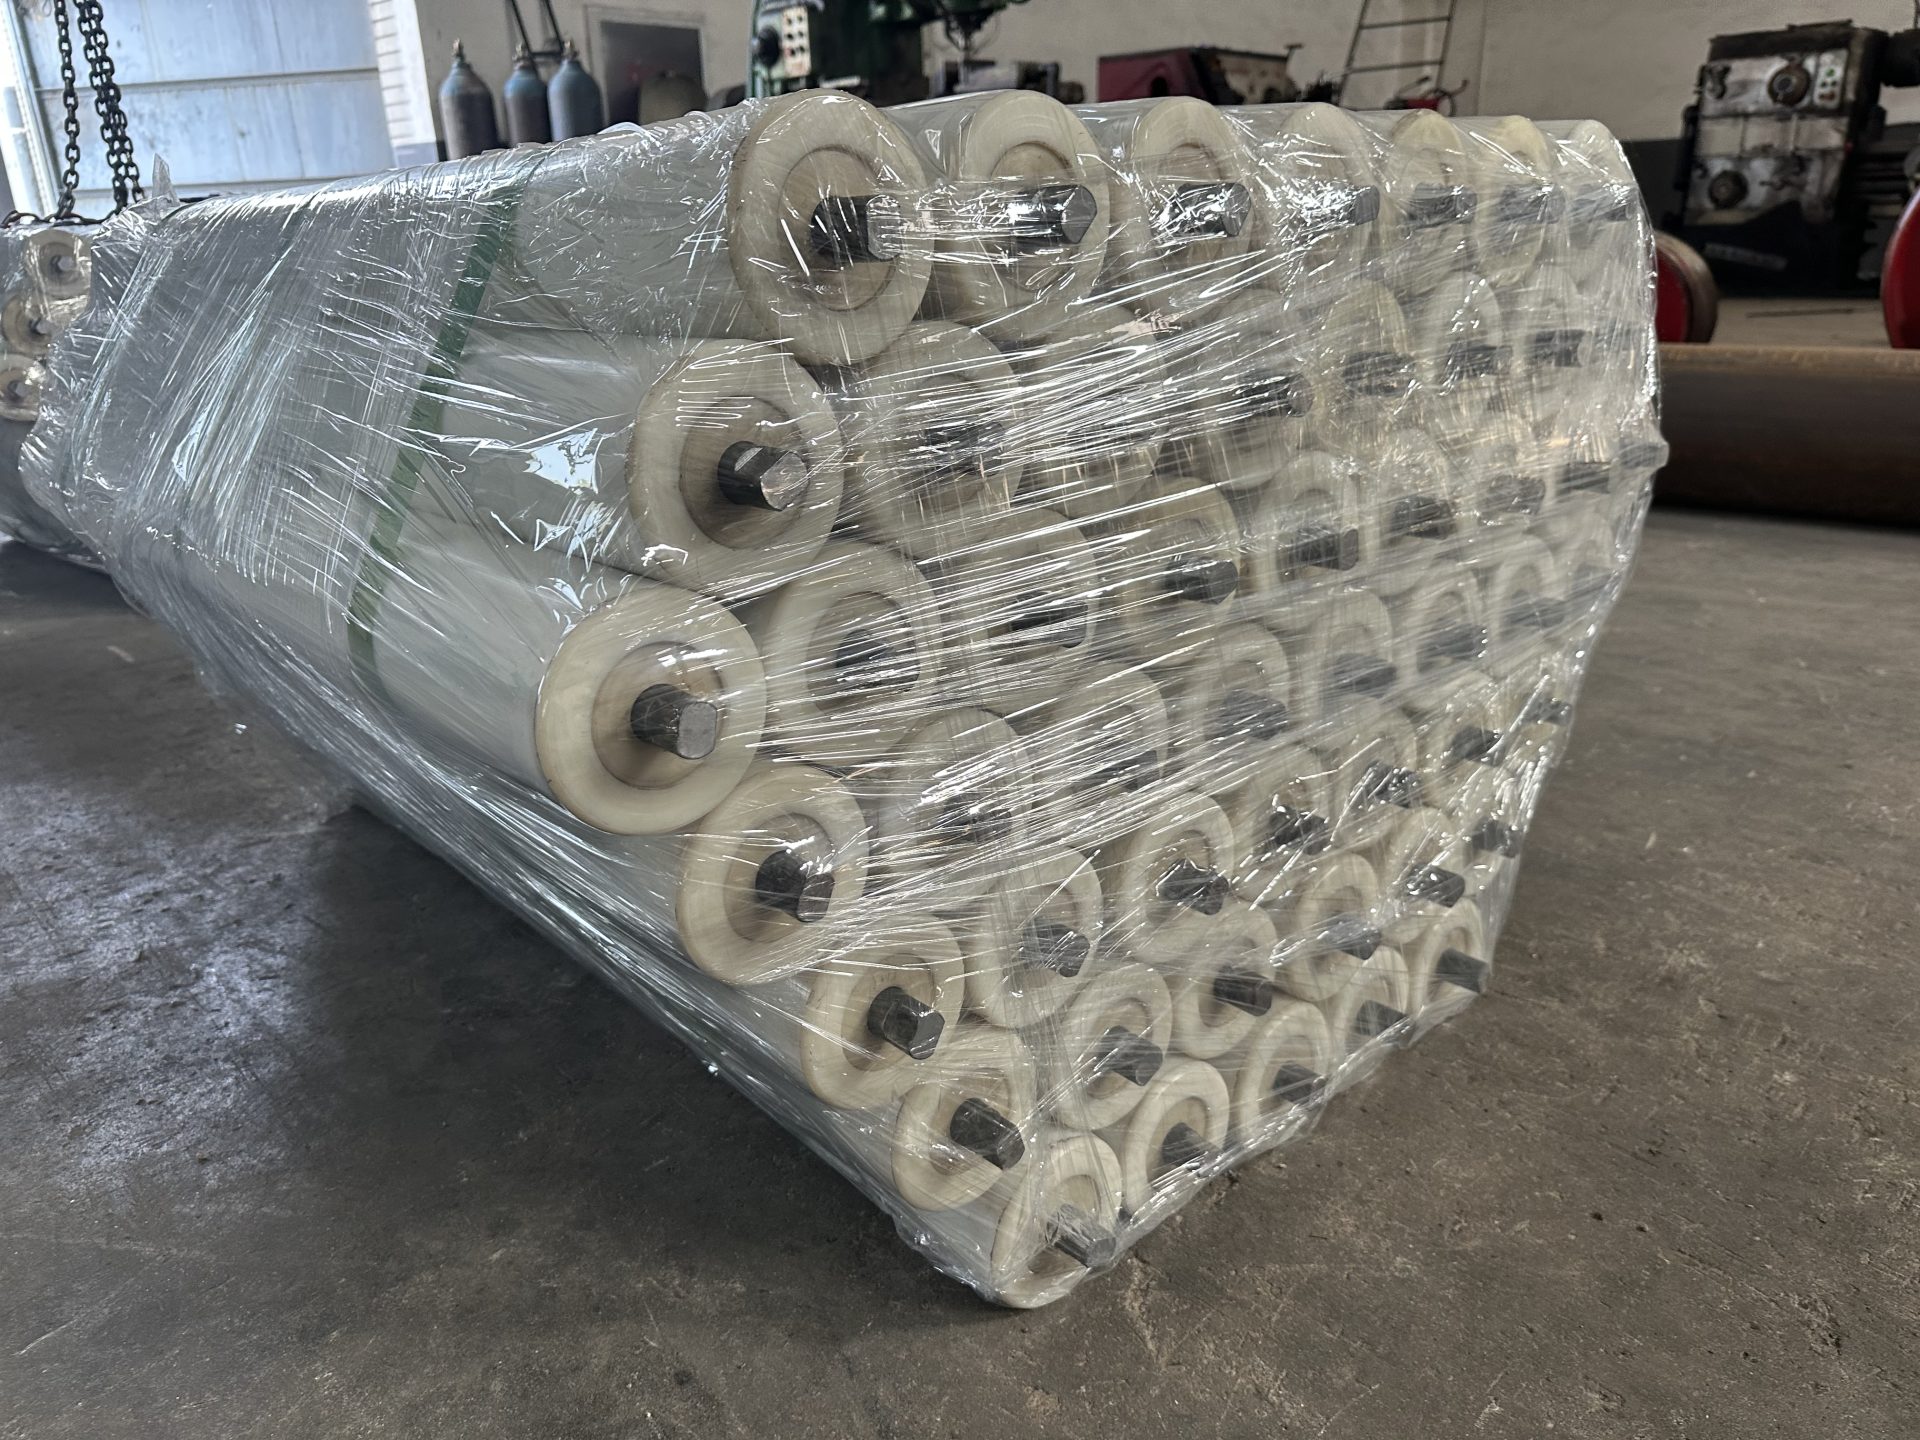
Polymer conveyor roller assemblies with metal shaft ends

A plastic working surface can remain intact while the roller stops turning. That is why an industrial buyer assessing a polymer conveyor rollers supplier should look beyond the tube material. For wet bulk handling, recycling or a coastal terminal, the useful question is how the complete roller deals with the load and the exposure around its ends. GRAM’s polymer roller range describes a machined polymer tube or solid bar, sealed precision bearings, non-contact rubber seals and metal end caps. Those parts should be evaluated together.

The polymer body may be relevant when corrosion of the working surface is a maintenance concern. It does not make every remaining part immune to water, chemicals or damage. Before changing from steel to a polymer construction, identify where the old roller failed and which part of the proposed assembly addresses that failure.

A Polymer Conveyor Rollers Supplier Should Identify the Complete Construction

The word polymer describes a broad material family. It does not identify a particular resin, reinforcement, bearing arrangement or end-cap material. A quotation that lists only a tube diameter and the word “plastic” leaves the buyer unable to assess the complete roller against a defined duty.

Machined Polymer Tubes and Solid Bars Are Different Starting Structures

GRAM’s published construction description allows a machined polymer tube or a solid bar. A hollow tube and a solid body are not the same geometry, even if their outside diameters match. Ask which structure is proposed and how the shaft and bearing arrangement relate to it. The order should identify the actual assembly rather than merge both possibilities into one material label.

For a long roller face, the body’s behavior under load deserves attention. For a shorter or differently supported roller, the same outside material may face a different structural requirement. The supplier should assess the proposed body with its support span, loading pattern and operating speed. Do not assume that a solid body is automatically preferable or that a hollow body is automatically adequate.

If the previous roller shows a persistent change in shape, distinguish surface wear from body deformation before specifying the replacement. A worn surface suggests a different investigation from a body that no longer presents the intended working geometry. Record the loading position and temperature exposure with that observation. The bearing-to-body connection also needs to remain appropriate for the proposed structure; selecting a polymer solely because it resists the carried material leaves that mechanical interface unexamined.

The working surface also needs to be considered against the carried material. Abrasive particles, sharp contamination and accumulated deposits create different wear mechanisms. Explain the actual exposure instead of asking for a universally wear-resistant polymer. The material and structure of the proposed roller must answer that particular operating condition.

Sealed Precision Bearings Remain Part of the Polymer Roller Order

The bearings provide rotation; they are not replaced by the polymer tube. GRAM identifies sealed precision bearings in its polymer assembly. Their suitability still depends on the proposed load, speed and conditions around the roller ends. A sound tube cannot compensate for a bearing arrangement that is unsuitable for the application.

A recycling maintenance buyer may find several rollers with little visible surface damage but poor rotation. That observation should lead to an examination of bearing condition and the contamination route, rather than an immediate demand for a harder tube. Record whether failures cluster beneath a chute, near washdown or along a particular return section. The location can help distinguish exposure from a general material problem.

Non-contact Seals and Metal End Caps Need Separate Exposure Checks

GRAM lists non-contact rubber seals and metal end caps as distinct elements of the polymer construction. That is a useful starting distinction: the tube’s resistance, the seal’s suitability and the end cap’s exposure are separate questions. A statement about the body material cannot answer all three.

Rubber Seals Must Match the Water and Chemical Contact

Describe how contamination reaches the ends of the roller. Rainfall, slurry splash, dusty material and cleaning water are different exposures. Also describe whether chemicals are present, how they contact the assembly and whether temperatures change during cleaning. Without that information, “wet conditions” is too broad to establish seal suitability.

For the rubber seal review, identify the actual cleaning agent and exposure pattern, including whether residue remains around the roller ends.

A non-contact arrangement can be part of a roller design, but the name alone does not establish a pressure-wash rating or permission to direct a jet at the bearing area. Obtain the proposed assembly’s cleaning and environmental limits. If the operator’s current cleaning practice exceeds them, changing the tube material leaves the same ingress risk in place.

Rulmeca’s composite roller description shows that body construction and sealing options are considered separately in a complete roller. Its resin formulations, seals and ratings belong to that manufacturer. The general lesson for a GRAM order is to name each relevant part and request confirmation for the actual exposure.

Metal End Caps Prevent a Blanket Corrosion-proof Claim

A polymer tube can reduce the area of metallic working surface while the assembly retains metal end caps and other metallic components. Identify those materials and where they will be exposed. If the original failure occurred at the roller ends, the tube change may address only a portion of the problem.

At a coastal terminal, a buyer may be comparing corroded steel shells with a proposed non-metallic shell. The comparison should also record shaft exposure, end-cap material and the bearing-end environment. There may be a sensible reason to change the shell, but that reason should not be extended into a guarantee that the complete assembly cannot corrode.

Rulmeca’s published metallic-to-non-metallic replacement example demonstrates that a material change can be evaluated for a specific corrosive environment. That project, its quantities and its construction belong to Rulmeca. It does not establish an equivalent GRAM installation; use the example only to understand why a replacement assessment needs both environmental and mechanical information.

GRAM’s steel roller family remains a relevant alternative where the proposed steel assembly matches the mechanical duty and environmental requirements. Evaluate the complete steel and polymer proposals for the same position. Comparing a specified polymer assembly with an unspecified “steel roller” creates a material comparison without a common technical basis.

Nylon Rollers and Other Polymer Rollers Are Not One Interchangeable Stock Item

GRAM offers nylon conveyor rollers separately from its broader polymer range. Nylon belongs to the polymer family, but the two names do not define identical products. A buyer should confirm the actual material and construction rather than accept either name as a complete substitute for the other.

Light-colored nylon conveyor rollers wrapped together with shaft ends visible
The nylon roller family is a separate route to examine. Surface color and a plastic description cannot establish material grade or allowable duty.

A distributor combining replacement stock for several customers should preserve those distinctions. One customer may need a particular shaft interface and exposure limit; another may be replacing a different polymer construction. An outside diameter shared by both orders is not a reason to merge their stock references before interchangeability has been established.

Polymer Roller Material Names Need Product-specific Limits

Request the material identification, operating limits and relevant compatibility information for the proposed roller. Do not copy another manufacturer’s chemical table or assume that every polymer behaves similarly in moisture and temperature. The buyer’s approval should refer to the supplied assembly, not to a generic description of plastic.

GRAM’s HDPE conveyor roller article explains another material route. It is useful for the terminology, but it does not establish that a particular roller in the polymer range uses that material. Confirm the construction before transferring an HDPE-specific requirement into the order.

Electrical behavior also needs its own evidence when the application requires it. Do not treat a non-metallic body as proof of either electrical insulation for the complete assembly or a suitable static-dissipation characteristic. If the site has a hazardous-area requirement, the approved product documentation must address it. General polymer advantages are not an underground or hazardous-area approval.

Quiet Rotation Is a Roller Requirement, Not a Noise Reduction Guarantee

The polymer range describes smooth, quiet rotation, and GRAM also offers a silent roller conveyor range. These descriptions identify product routes worth assessing where noise is a concern. They do not provide a measured reduction for a specific installation or establish that a tube change will solve every source of conveyor noise.

A noisy conveyor can have damaged bearings, poorly supported components or material impact as well as noise associated with the roller body. Describe when the sound occurs and which position produces it. A repeatable observation under a defined duty is more useful than a request for the quietest material without an agreed comparison.

If a sound-level criterion is part of the project, agree how it will be measured and which operating conditions apply. Keep the requirement attached to the complete assembly and the intended conveyor position. Do not write a numerical improvement into the purchase description unless the proposed product and test basis support it.

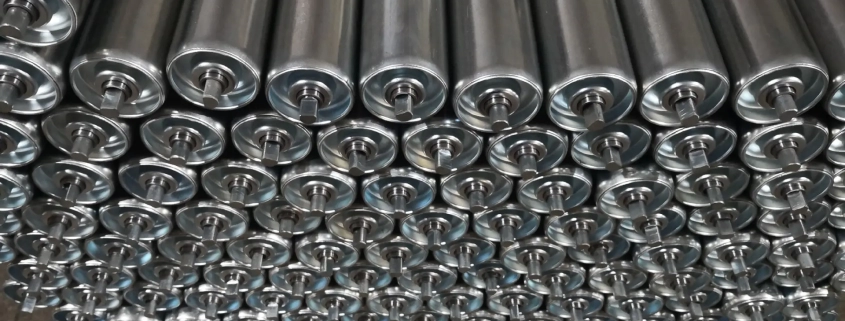
Metal conveyor rollers stacked with shell ends and bearings visible for comparison with polymer assemblies
Compare complete assemblies under the same duty. Body material is one selection variable alongside bearings, seals and support geometry.

Loading Impact Can Require a Different Roller Family

A polymer body proposed for ordinary carrying duty should not automatically be assigned to the material landing zone. GRAM’s impact roller range addresses a different support duty through a ringed impact construction. The material landing pattern and load should determine whether an impact assembly is required.

A terminal operator may have corrosion along the carrying run and repeated damage directly below the transfer chute. Those observations can justify two different component decisions. Assess the polymer assembly for the carrying exposure, while the transfer-point support is evaluated for impact. Buying one body material for every station can conceal that distinction.

The proposed impact roller still needs an agreed installed diameter, shaft arrangement and support geometry. A polymer carrying roller and a rubber-ring impact roller can both be non-metallic at the working surface without performing the same job. The construction and duty, rather than the surface appearance, establish which family belongs at each position.

Keep the Polymer Roller Construction Intact Through Receipt and Storage

The receiving check should connect the delivered roller to the agreed body structure, bearing and seal arrangement. Record the product reference and drawing revision so a later spare order does not quietly change a tube into a solid body or substitute a different end assembly. Where inspection evidence is required, specify which construction features it must establish.

Transport protection should preserve the working surface and the roller ends. Agree how the polymer bodies will be supported and how the end caps and shaft interfaces will be protected against damage. The packing arrangement should follow the supplied roller geometry; no photograph of a bundled shipment establishes a universal packing method for all polymer orders.

At receipt, do not treat smooth hand rotation as proof of performance under the operating load. It can be one agreed preliminary check, alongside identification and visible condition, but the acceptance basis must address the actual application. Confirm the relevant inspection method and limits before delivery rather than inventing a pass criterion beside the unloaded shipment.

Once the shell, seals, bearings and remaining metal parts have been identified, the material change becomes a defensible decision. If only the polymer tube has an established compatibility basis, keep the rest of the assembly open for review. The goal is a roller that addresses the site’s exposure as a complete unit, not a corrosion-resistant surface surrounding an unresolved failure path.

GRAM rubber-ring conveyor impact rollers

A replacement impact roller cannot protect the belt where the incoming rock misses its support. A contractor choosing a quarry conveyor impact rollers supplier should show where the material lands, how the belt is supported there and where the loading zone changes into normal carrying support. GRAM’s rubber-ring impact rollers and load-zone belt support provide two routes to assess. Begin with the actual chute and belt position before specifying a roller diameter or replacement quantity.

The buyers who benefit most are quarry maintenance teams and contractors altering crusher discharge or transfer chutes. First confirm the material stream under credible operating conditions, including its position across the belt. Then give the supplier the existing station geometry and shaft interfaces. The product name does not establish an impact capacity or prove that the support is correctly located.

A quarry conveyor impact rollers supplier needs the rock landing position

The material trajectory and the support station are parts of one loading arrangement. Identify the belt direction, chute outlet and landing region on a drawing. Record any difference between an empty-belt position and the loaded operating condition using the plant’s approved engineering assessment. The supplier should not have to infer these relationships from an isolated roller sample.

Crusher discharge changes can move the impact away from the original station

A quarry modifying a crusher discharge may retain the original conveyor frames. If the rock now enters at a different position or with a changed stream shape, those frames may no longer place the support beneath the relevant landing region. Review the modified transfer as a system. Copying the old roller dimensions is a mounting decision, not an assessment of the new impact condition.

Provide the range of stone sizes and the intended feed condition to the responsible designer. Describe whether large fragments occur regularly or during an upset. The supplier needs that operating basis to discuss the offered assembly. No drop height, impact energy or load rating should be invented from a general photograph of the product.

Edge loading should be distinguished from central belt support

A buyer seeing belt-edge damage should identify where the material actually lands and how the edge is supported. The issue may involve the stream location, chute geometry or surrounding contact rather than the roller material alone. Do not assume every edge mark means the plant requires impact rollers along the entire conveyor.

Have the belt and transfer inspected under the approved isolation procedure. Describe the damage position without claiming a cause that has not been established. A drawing and photographs of the isolated arrangement can help the supplier understand the interface, while the plant’s engineer determines the required support and any transfer correction.

Quarry impact roller selection must define the rubber-ring assembly

GRAM’s impact roller construction uses rubber rings on the working body. That is a different contact surface from an ordinary steel carrying roller. Identify the offered complete assembly, including the working body, bearing ends and shaft interfaces. A rubber roller enquiry should specify that impact-support function rather than leave the supplier to choose between ringed and continuously coated products.

Rubber rings should be reviewed with the supported belt shape

The ringed surface belongs to the loading-zone support arrangement. Ask how the proposed roller fits the intended station geometry and where it contacts the belt. If an existing sample is worn, compare the offered new arrangement with the approved conveyor drawing rather than copying worn dimensions without review.

The rubber-ring impact roller discussion explains that construction boundary. For a quarry enquiry, keep the principal question focused on the rock landing zone and support transition. Ring dimensions alone cannot determine whether the assembly is located correctly beneath the transfer.

Shaft ends still need to fit the retained quarry brackets

Record the actual mounting span and shaft end form. If the supplier proposes a different end assembly, compare its full envelope with the frame and neighboring components. A matching nominal roller length does not establish that the shaft seats or bearing ends fit without interference.

Where the repair retains the station brackets, inspect those interfaces before ordering. Damage or distortion in the retained frame can affect the installed support position. Do not use a different roller dimension to compensate for an unreviewed frame problem. Have the equipment owner resolve the mounting condition first.

Conveyor impact bed with longitudinal bars and inclined side support regions
A bar-type impact bed is another support route to assess for the defined loading zone.

Compare rubber-ring rollers and impact beds at the actual transfer

GRAM’s load-zone support images show longitudinal bars and inclined side regions. This is a different support arrangement from rotating impact rollers. The choice should be evaluated against the conveyor geometry, material entry and maintenance needs. It is not enough to select whichever product appears more substantial in a photograph.

A contractor may need to assess how the proposed support affects the belt contact region and the surrounding loading arrangement. Provide the retained equipment envelope and the approved support requirement. Any dimensional or operating suitability of the offered bed must be established for that project; the general product route does not declare a universal impact rating.

Replacement access differs as well. A roller needs a defined removal path from its brackets, while a bar-type support needs its own access arrangement. Include guards and nearby chute components in the review. The plant should not discover that the selected replacement cannot be serviced through its approved maintenance route after installation.

The quarry loading zone needs a clear exit into carrying support

Impact support is not the whole conveyor. GRAM’s steel carrying roller route is relevant beyond the loading zone, while its suspended garland range offers another carrying arrangement for bulk materials. Each assembly has its own mounting and support geometry.

Show where the belt leaves the proposed loading support and reaches the next carrying station. Have the designer assess that transition against the belt and load conditions. A support arrangement can be appropriate at the landing point while still needing a coordinated transition to the surrounding stations.

Steel conveyor rollers for normal carrying support beyond a quarry loading zone
Normal carrying support should be defined separately from the impact-support region.

GRAM’s main roller range provides the broader construction choices. Use it to identify an appropriate carrying or replacement route after the support function is established. Do not treat every roller on a quarry line as an impact roller simply because the first transfer handles falling stone.

External Rulmeca bulk component information distinguishes impact and carrying products. That functional distinction supports the transfer review. Its product-specific capacities, models and installation dimensions are not ratings for GRAM equipment.

Include oversize rock and fines in the quarry impact offer

Oversize rock and fine aggregate should both appear in the transfer description

A quarry’s usual product description may omit the occasional large fragment that matters at a loading zone. Tell the responsible designer which operating conditions can produce that fragment and how the feed is controlled. The supplier’s assembly proposal should refer to the defined range. An impact rating cannot be chosen from the average material description alone.

Fine material can create another issue around the same station: deposits at end components or the retained brackets. Describe those conditions separately from the rock impact. A rubber-ring working surface addresses the support construction, while contamination at the ends requires a discussion of the offered bearing protection and maintenance exposure. One feature should not be presented as resolving both automatically.

For a chute modification, show the proposed and retained geometry clearly. If the station location, loading direction or adjacent support has changed, identify who approves that change. The roller manufacturer can supply against a defined assembly requirement, but the quarry’s transfer design must be coordinated by the responsible project team.

A buyer planning a phased repair should identify which parts will remain in service after the new impact assembly is fitted. Worn neighboring carrying rollers, damaged brackets or unresolved belt contact can affect the installation. Inspect and assess those retained interfaces through the approved procedure rather than assuming a new loading-zone product makes the surrounding equipment acceptable.

If several transfers need replacements, keep each loading description attached to its station identification. Two stations can use similar roller dimensions while receiving different rock streams. The supplier should know whether the buyer has established a common duty or simply has a convenient common frame size. That distinction prevents an unreviewed substitution between transfer locations.

Ask the supplier to identify the assembly offered for the stated landing condition and mounting arrangement. If an applicable load or impact performance is required, obtain the corresponding product-specific information and test basis. A generic heavy-duty description cannot establish the value needed for the plant’s engineering approval.

Inspect delivered rubber rings, end components and shaft interfaces against the approved assembly record. Check visible damage and rotation before installation. Where a set contains different positions or components, preserve their identification. An undocumented change in working profile or mounting geometry should be reviewed before it enters the loading zone.

Agree packing that protects the rubber working surfaces and keeps projecting shaft ends from damaging neighboring components. Mark the replacement packages by station or transfer position. If ordinary carrying rollers arrive in the same delivery, keep them distinct from the ringed impact assemblies.

Show the supplier the rock path before approving the impact roller order. The useful replacement is the one that matches the defined support geometry at the actual landing zone and connects properly to the carrying arrangement beyond it. If the rock path has changed, resolve that change rather than expecting a stronger-sounding roller description to compensate.

Steel conveyor rollers stacked with bearing ends and shaft interfaces visible

Fine material around a roller end is useful evidence for a quarry replacement inquiry, but it is not proof that a bearing has failed or that changing the body material will solve the problem. A quarry conveyor rollers supplier should see where the deposits form, which positions are affected and what cleaning exposure occurs there. Begin with GRAM steel rollers and the actual complete end construction, then compare alternatives for the identified quarry duty.

A quarry operator or contractor should preserve the distinction between dust on the outside, deposits on the working body and evidence of an internal problem. Each raises a different question. The supplier needs the actual observation and retained equipment information before offering an accepted replacement construction.

A quarry conveyor rollers supplier needs the deposit location

State whether fines collect on the roller body, near the end cap, around the shaft interface or on surrounding supports. A photograph should show enough of the retained position to locate the deposit. A close-up of dust alone can conceal which part of the assembly the buyer wants the supplier to evaluate.

For a quarry whose screening duty has changed, describe the current stream as well as the former one. Fine material presented to a roller near a screen discharge can differ from exposure elsewhere in the plant. Do not turn the shared quarry application into an assumption that all positions need the same end construction.

Does the inquiry distinguish three observations? material on the working surface, material around the ends, and any independently established internal condition. Keep them separate before asking for a different roller.

Working-surface deposits are not bearing inspection results

A visible deposit on the body describes belt-contact conditions and material accumulation. It does not identify the internal bearing state. If the buyer has separate inspection information, attach it with the roller reference; if not, describe the external observation without presenting a diagnosis.

The same caution applies to a stiff or noisy removed unit. Record how the condition was observed and which assembly was examined. The supplier should not be asked to infer a universal bearing failure mode from a short description that lacks the relevant component and operating context.

End exposure should include the actual cleaning contact

If quarry cleaning reaches the roller ends, describe that exposure as part of the duty. State what actually contacts the assembly rather than assume that any outdoor roller is suitable for every cleaning method. The proposed end and seal construction needs its own accepted basis for the relevant condition.

A contractor should distinguish cleaning of nearby structure from direct exposure of the roller ends. Otherwise the supplier may assess a different condition from the one present at the retained position. This article does not prescribe a washing method or claim that a seal arrangement has been tested for it.

Compare steel and polymer as complete quarry roller assemblies

GRAM’s steel route describes a cylindrical rotating body with bearings toward the ends and projecting shaft interfaces. Those end components matter when the buyer’s concern involves fines near the shaft or cap. The steel body alone does not define the complete assembly’s resistance to the observed environment.

Steel body identity should remain attached to the offered ends

Ask for the actual proposed body and end arrangement for the retained position. A replacement that reproduces the tube dimensions can still contain a different end construction. Conversely, a familiar external cap appearance does not establish identical internal components or a particular dust-exclusion performance.

For a quarry ordering several ordinary steel rollers, identify which positions carry the end-exposure requirement. A consolidated manufacturing or shipping order can still preserve those different duty references. Do not let a shared tube size erase the condition that triggered the supplier review.

Polymer bodies do not remove metal ends and bearings from the review

The GRAM polymer roller route describes a machined polymer tube or solid bar, sealed precision bearings, non-contact rubber seals and metal end caps. A polymer body is therefore one part of a more varied assembly. The end components remain relevant to the quarry exposure.

GRAM polymer rollers whose body and complete end construction should be reviewed for quarry fines exposure
A polymer surface does not establish the performance of every component at the roller end.

A buyer comparing a polymer offer with the previous steel roller should keep the changed body and proposed end construction visible. The accepted mounting relationship also remains necessary. Neither a body-material preference nor a retained shaft fit settles the complete environmental suitability question.

A primary roller field-evaluation example relates observations to identified equipment and conditions. That is a useful general evidence principle. Its measured values, operating history and seal conclusions do not describe GRAM rollers or the buyer’s quarry.

Ringed quarry rollers need the working body and ends described together

GRAM’s rubber-ring impact rollers use a different belt-contacting surface from a plain cylinder. If the affected position lies at material entry, preserve the ringed working construction in the offer while also identifying the ends being evaluated.

GRAM rubber-ring impact roller showing a working-surface decision separate from quarry roller-end exposure
Ringed working surfaces and end exposure are different parts of the same assembly review.

Do not treat rubber rings as evidence of a particular bearing-seal rating. The rings address a working-surface function; the complete end construction addresses another part of the proposal. A supplier should identify both where the customer’s retained duty requires them.

For a contractor comparing plain and impact positions near the same transfer, mark which roller construction belongs at each location. Similar deposits do not make their operating roles interchangeable. Keep the material-entry condition connected to the impact proposal rather than copying the ordinary carrying description.

Belt cleaning and tracking are separate from a roller-end substitution

If deposits originate from material carried beyond the discharge, the buyer should also identify the belt residue path. GRAM’s polyurethane cleaner route addresses belt contact through a blade and supporting assembly. It does not establish that fitting a cleaner will eliminate every deposit at roller ends.

The return roller carryback discussion helps describe that residue duty. Keep the cleaner and roller proposals separate, identifying which observed problem each is intended to address. A changed roller body should not be sold as a substitute for an unresolved material path.

Likewise, the GRAM self-aligning idler route concerns tracking-related support. If deposits coincide with belt movement, preserve both observations without assuming that an end seal change will correct the belt path. The actual retained arrangement needs its own assessment.

A quarry can investigate several interacting conditions while still keeping the supply order clear. Identify the selected roller construction, any separately accepted cleaner or tracking proposal and the equipment interfaces that remain. Avoid combining unrelated product descriptions into a promise of a complete cure.

Protect the accepted quarry roller ends through delivery identification

Consider a quarry that reports dry fines around several steel roller ends near one screening line, while rollers elsewhere mainly show deposits on the working bodies. Keep those observations attached to their separate locations. A photograph of the worst dusty end should not become the environmental description for the entire plant’s replacement order. The supplier can compare constructions for the identified positions without being asked to infer that every unit has the same internal condition.

A contractor may also find that one affected roller sits near a cleaning access point while a neighbouring unit is shielded by retained equipment. Show that distinction in the inquiry where it changes actual exposure. It does not prove that the shielded assembly needs no review; it gives the supplier a clearer description than a blanket statement that the conveyor is washed. Avoid assigning a washing-resistance rating that neither the actual proposed assembly nor its documentation establishes.

For ringed loading rollers, separate material lodged around the working rings from fines observed at the ends. The ringed surface may require its own maintenance assessment while the end construction remains a separate supplier question. Describe both locations and preserve the complete roller reference so one photograph is not used to support two different diagnoses.

The supplier’s proposed end construction should remain recognizable in the accepted item reference and delivery information. Where several similar roller bodies have different agreed ends, the receiving team should be able to distinguish them. Agree that requirement for the actual order instead of assuming an unpublished standard label system.

Ask how the selected roller bodies, end caps and shaft interfaces will be protected in the proposed package. The discussion should concern these supplied assemblies, not a generic export packing statement. Identify any transport or receiving constraints the quarry has, and let the supplier define the actual arrangement.

On receipt, preserve any observed external damage separately from the original operating concern about fines. A damaged delivered end and a dusty retained unit are different records. Neither should be used to invent an internal diagnosis or an unsupported claim about the new assembly’s expected life.

Give the supplier a clear picture of where fines reach the retained roller, accept a complete construction for that position, and keep the unrelated cleaning or tracking questions visible. That makes the replacement decision specific enough to review without assigning every quarry problem to the body material.

Steel conveyor rollers stacked with bearing ends and shaft interfaces visible

A screen adjustment can change the idler duty downstream without moving a single conveyor bracket. A plant choosing an aggregate conveyor idlers supplier should tell the supplier when the handled product changes from coarse stone to smaller or wetter material. GRAM’s conveyor roller range and its steel, polymer, impact and suspended arrangements provide routes to review. Start with the material leaving the screen, the loaded belt shape and the installed support geometry.

This is useful for screening operators, quarry maintenance buyers and distributors supplying several aggregate lines. First establish whether the purchase replaces normal carrying support, loading-zone support or a suspended group. Then describe the changed particle distribution, moisture and feed pattern. An old roller sample can preserve mounting dimensions while saying little about the new duty.

An aggregate conveyor idlers supplier needs the current screen output

The product name should identify what the conveyor now carries. Coarse aggregate, washed fines and a changing mixture can present different contact and contamination conditions. Provide the current operating description rather than the screen setting alone. The supplier needs to understand the material that reaches the belt and where it is deposited.

Coarse aggregate and wet fines should not share an unexplained duty description

A screening plant may change its product grading while retaining the conveyor frames and rollers. If the resulting material contains more fines or moisture, the ends may see a different deposit pattern. Record that change alongside the existing mounting dimensions. The replacement discussion should address the present exposure, not merely reproduce the original purchase label.

A distributor stocking for both dry stone and washed material should keep those duty descriptions separate. The same nominal roller size can appear in both locations, but the assembly selected for each must be confirmed. Stocking convenience is useful only after the operating requirements are understood.

Screen discharge position affects the loading-zone support

The material stream may move when the screen arrangement or discharge chute changes. Identify where it lands relative to the belt center and support station. GRAM’s rubber-ring impact rollers are a different construction from ordinary carrying rollers. Their purpose should be assessed at the actual material entry.

If the stream now reaches an edge or a different station, have the loading arrangement reviewed. A correctly sized replacement roller cannot establish that the retained station sits beneath the changed landing point. Record the chute and support geometry together rather than trying to solve the problem by requesting a more substantial roller body.

Rubber-ring impact rollers for assessing changed screen-discharge loading conditions
Review impact support where the screen product reaches the belt, separately from normal carrying support.

Aggregate conveyor idler selection should preserve the belt support shape

The idler assembly supports the belt in an intended cross-sectional shape. That shape and the conveyor’s frame references belong in the enquiry. Do not assume an individual roller’s tube dimensions establish the station geometry. If the purchase includes brackets or a complete set, identify those parts of the assembly explicitly.

Carrying rollers need a position within the support station

Use the carrying-roller position guide to separate the role of an individual roller from the whole support arrangement. State which station and position the replacement serves, and retain its shaft-end and mounting references. A roller described only by diameter and length can leave that relationship unclear.

When the handled aggregate changes, review the loaded belt condition through the equipment’s approved engineering process. The offered roller assembly must suit the defined load and support geometry. A supplier’s general carrying-roller description is not a calculation of the conveyor’s capacity under the new screen product.

Suspended garland groups need their links and connections defined

GRAM’s carrying garland range describes linked suspended rollers and includes aggregate applications such as sand, gravel and crushed stone. The group is a complete arrangement, so specify its suspension interfaces and geometry as well as the individual rollers.

If only one component is being replaced, assess compatibility with the retained group. If the whole group is being renewed, identify what the supplier includes in the assembled set. The purchasing scope should not depend on an installer discovering which links or mounting components were omitted after delivery.

Compare steel and polymer idlers against the aggregate exposure

GRAM’s steel rollers provide a metal body route with end bearings and shaft interfaces. Its polymer rollers provide a separate route described with tubes or solid-bar bodies, sealed precision bearings, non-contact rubber seals and metal end caps. Compare complete assemblies rather than isolated shell materials.

Wet fines can make the end construction particularly important. Tell the supplier where deposits reach the roller and whether cleaning adds another exposure. A polymer body’s general corrosion resistance does not establish the protection of every bearing or shaft. Ask what construction is offered for that actual position.

Polymer conveyor roller assemblies for comparing body and end construction in aggregate service
Material comparison should retain the same frame, loading and contamination requirements.

For a dry coarse-product line, a different problem may dominate: the mechanical support duty or damage at entry. Do not assume a moisture-focused replacement addresses those requirements. State why a material change is being considered and compare the offered assemblies against that reason.

Rulmeca’s bulk component information separates steel, polymer, impact, return and suspended products by function. That external distinction helps organize an aggregate enquiry. Its specific models, loads and approvals remain its own; they are not ratings for the GRAM assemblies.

Use the aggregate line’s operating evidence before repeating an old idler order

Record when the screen product changed and which roller positions began to show different deposits or rotation. The observation should identify an actual condition rather than claim an unverified failure mechanism. Close inspection must follow the plant’s isolation procedure; do not approach moving rollers to collect measurements.

Compare similar positions under similar material conditions where possible. A new idler on a clean dry line is not a useful comparison with a worn unit beneath wet fines. Keep the exposure and load differences visible so that the purchase decision does not assign every change to the roller body material.

Short production runs and changing moisture should be included in the enquiry

A plant producing several grades during a day should describe the range of material conditions the same conveyor sees. The roller may not operate under a single steady product description. Explain which combinations of coarse material, fines and moisture are credible, and ask for the offered assembly to be assessed against that defined range.

If cleaning is performed between products, provide the method and any exposure at the roller ends. That can be relevant even when the conveyed aggregate is normally dry. Retain the cleaning condition in the replacement record so a later repeat order does not omit it.

Keep aggregate duty changes with the replacement station drawing

Before a changed screen product becomes the new normal, agree what information needs to remain in the idler specification. The product description, moisture condition and loading location should be current. The mounting dimensions may be unchanged, but that does not make the old duty description accurate. Keep both parts of the record so an urgent purchase does not revert to an obsolete operating assumption.

A buyer comparing assembly offers should also identify which components belong to the supplied unit. An individual carrying roller, a roller-and-bracket combination and a suspended garland group have different boundaries. If the quotation omits that boundary, ask for the drawing and item description to be clarified. The installer should not discover the intended scope while trying to assemble parts from several deliveries.

The aggregate spare register should preserve the approved material and end arrangement

A distributor may receive an offer for a polymer body after previously stocking steel rollers of the same nominal dimensions. Identify that material change in the inventory description, together with the offered bearing-end construction. Matching mounting dimensions can be useful, but they do not establish equal duty. Keep the customer’s approved operating condition with the assembly that was evaluated for it.

Similarly, do not combine dry carrying rollers and replacements selected for wet fines simply because their tubes look alike. The proposed end arrangement may be a significant part of the selection. If the supplier offers a substitute, obtain its construction description and assess it against the same exposure before accepting it for the stored part number.

For an installation trial, select a station with a defined material and loading condition. Record what the comparison is intended to show, and retain the approved isolation and maintenance procedure. A short successful trial under one screen grade should not become a blanket performance claim for every aggregate mixture handled at the plant.

At delivery, compare the complete assemblies with the approved station records. Confirm mounting span, shaft ends and supplied set components, and inspect rotation and visible damage. If end protection was part of the selection, verify the declared arrangement on the delivered units rather than accepting an undocumented alternative.

Agree packing and identification that distinguishes impact assemblies, ordinary carrying rollers and suspended groups. Protect shaft ends and connecting components from contact damage. A distributor serving several aggregate customers should retain both the mounting specification and duty description on the inventory record.

When the screen product changes, update the idler enquiry before placing the repeat order. Keep the frame dimensions that remain valid, replace the obsolete material description and confirm the role of each support assembly. That gives the supplier a clear basis for a replacement that belongs to the current aggregate line.

Steel roller assemblies with cylindrical bodies, bearing ends and projecting shafts

A steel certificate can describe the roller shell without saying whether the complete idler assembly meets the order. Buyers evaluating a belt conveyor idlers manufacturer should connect the accepted drawing, offered construction and inspection evidence to the same component. GRAM’s conveyor roller range includes several materials and duties, with customer-specification manufacture described for roller supply. Establish which complete assembly is being offered before treating evidence for one material as approval of the whole unit.

A belt conveyor idlers manufacturer should identify the assembly behind the evidence

Start with the actual roller or assembly reference in the accepted proposal. A shell, shaft, bearing end and sealing arrangement form different parts of the component. The inspection information should make clear which accepted construction was examined, rather than rely on a general statement that conveyor rollers are checked before delivery.

An engineer receiving only a shell-material certificate should preserve the unanswered assembly questions. GRAM’s steel roller route can establish the type of product under discussion, but the certificate does not automatically describe the bearings, shaft interface or finished working body. Ask how the supplied evidence corresponds to those actual components.

Keep the component reference consistent: the accepted drawing, offered material and end construction, examination record and delivered identification should describe the same roller assembly. A document for a constituent material is one part of that evidence, not the complete acceptance case.

The steel body and its bearing ends need distinct descriptions

GRAM’s steel rollers have cylindrical working bodies, bearing ends and projecting shafts. Preserve the actual accepted construction for each relevant part. A material document describing the steel body should not be assumed to establish the condition or identity of the bearing-end arrangement.

If a repeat order changes the end construction, keep that revision visible in the supplier’s acceptance information. The shell can remain similar while the completed assembly changes. A previous record should not be treated as applicable solely because the nominal body dimensions still match the older order.

The shaft interface is part of the completed roller offer

The projecting shaft and its retained supports define an installation relationship separate from the cylindrical belt-contacting body. The accepted order should identify that interface without relying on a supplier’s general range description. This allows the receiving team to compare an identifiable completed component with the actual offered construction.

This discussion does not establish a shaft size, tolerance or support rating. The responsible design must define the accepted values for the order. The manufacturer’s evidence should connect to those actual requirements rather than supply a generic result with no clear relationship to the delivered assembly.

Polymer idler acceptance includes the bearings, seals and metal end caps

GRAM’s polymer rollers are described with a machined polymer tube or solid bar, sealed precision bearings, non-contact rubber seals and metal end caps. These are specific construction elements to identify in the offer. The polymer working surface does not make the remaining parts disappear from the assembly review.

A buyer choosing polymer because a previous steel body suffered surface deterioration should still retain the bearing-end and sealing questions. Evidence about the tube material alone cannot establish the complete assembly’s accepted duty. The supplier should identify what has been examined and which requirements remain supported only by the proposed construction description.

A tube declaration is not evidence for every end component

The declared polymer material and the offered end construction should be recognizable as separate parts of the same order. If the supplier provides a material statement, identify the component it addresses. Do not read it as a general environmental or service-life guarantee for the bearings, rubber seals and metal caps.

For an alternative proposal that changes the end cap or sealing arrangement, ask which assembly reference the supporting information now describes. A similar tube appearance does not establish an unchanged complete construction. Keep the revised offered parts connected to the actual acceptance case before approving the substitution.

GRAM polymer roller bodies and end components to identify together in the accepted assembly evidence
The working body and end components belong to one identifiable supplied construction.

Roller rotation evidence needs an identified construction and examination basis

A claim that a roller turns smoothly should refer to an actual examined assembly and the applicable acceptance basis. Keep the offered bearings and seals identifiable when considering that evidence. A subjective description of one demonstration component should not become a numerical operating guarantee for all supplied rollers.

The buyer should ask what condition was examined and how the reported result corresponds to the accepted order. Do not invent an acceptable resistance, bearing life or operating-temperature limit from a range description. Where the contract requires a particular measurement or examination, the responsible technical parties must agree its actual basis.

Factory evidence and field evidence describe different conditions

An examination before dispatch and an observation on an installed conveyor concern different operating conditions. If either is supplied as evidence for the GRAM offer, identify the actual component and circumstances. Neither should be presented as the other, or treated as proof of unexamined environmental performance.

Rulmeca’s published field comparison illustrates the value of linking observations to identified equipment. Its project, measurements and conclusions belong to that manufacturer. They are not GRAM trial results and should not be used to fill missing evidence for the order under review.

Rubber-ring impact rollers require their own working-body identity

GRAM’s impact rollers have rubber-ring working surfaces around the roller body. Keep that construction identifiable where it is selected for a loading duty. A record for a smooth steel cylinder does not automatically describe the completed ringed assembly being purchased.

The accepted proposal should identify the ringed working construction as well as the shaft and end arrangement. Where the buyer requests evidence concerning a particular supplied part, the manufacturer should connect that evidence to the actual offered component. No ring hardness, material grade or impact-energy rating follows from the product photograph.

The ring arrangement and core body should remain distinguishable

A buyer should be able to identify what the offer describes when it refers to the working diameter or ringed surface. Preserve the accepted construction relationship instead of treating the visible outside of a sample as the only definition. The underlying body and bearing ends still belong to the complete roller acceptance.

If a proposed revision changes the ringed arrangement, keep the affected component reference visible. Do not assume that evidence for the previous working construction remains applicable simply because the retained shaft interface is unchanged. The supplier’s actual acceptance information should follow the revised assembly.

Suspended garland acceptance extends beyond the individual rollers

GRAM’s carrying garland assemblies use suspended connected rollers. The individual roller construction and the linked supplied group therefore need distinguishable acceptance information. A document identifying one roller is not a complete description of the connections and delivered assembly scope.

For a buyer ordering garland components alongside ordinary steel idlers, preserve the group reference and the accepted connection scope. The receiving team needs to know which supplied parts belong together, without assuming that every similarly sized roller can be moved between the linked assembly and a retained rigid station.

GRAM connected garland roller assembly whose group and component acceptance references should remain distinguishable
Accept the identified suspended group as well as the roller components it contains.

Agree delivery identification that preserves the assembly grouping and its component references. Any separately supplied connection parts should be identified in the actual offer; a photograph is not proof that all surrounding mounting hardware is included. The receiving documents should let the buyer compare the delivered scope with what was accepted.

Accept manufactured idlers against the selected assembly revision

A mixed delivery creates a specific receiving problem: a plain steel roller, a rubber-ring impact roller and a connected garland group can each have an accepted reference without sharing the same acceptance scope. Identify the plain roller by its body and ends, the impact roller by its ringed working surface as well as those ends, and the garland by the supplied connections and group arrangement. A receiving label that describes all three simply as “idler” loses distinctions already made during selection. Keep the accepted assembly references visible on the delivery information that the receiving team actually uses.

Where a polymer roller is offered as an alternative to a steel unit, separate the retained mounting relationship from the revised body and end construction. The dimensional fit can remain acceptable while the materials and seal arrangement change. A fit drawing therefore answers a different question from evidence about the assembled roller’s running behaviour. Accept each against the proposed revision, and keep any unresolved requirement explicit. The buyer does not need to invent a universal test limit to distinguish those two questions; the important step is ensuring that the supplier’s evidence refers to the assembly being purchased.

The discussion of mixed-fleet roller identities helps separate product roles. For manufacturing acceptance, connect that role to the actual assembly revision and its evidence. Do not let a general family reference replace the construction that the supplier has agreed to deliver.

Where a document does not identify the examined component, ask for that connection before accepting it as support for the order. A useful answer can also state what evidence is unavailable. That is preferable to expanding a material statement into an unsupported claim about complete roller performance.

Release the order when the selected body, shaft, bearings and end construction remain identifiable through the accepted proposal and delivery record. Keep ringed surfaces or suspended-group connections visible where they form part of the supplied assembly. The receiving team should be assessing the roller that was actually selected, not a collection of documents that merely mention the same product family.

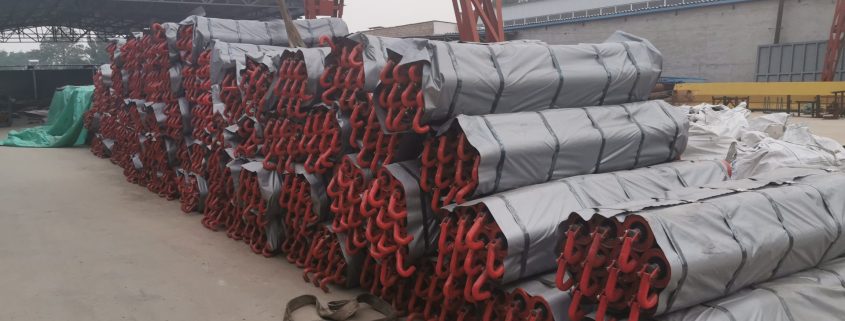
Wrapped carrying garland sets with red suspension end connections exposed
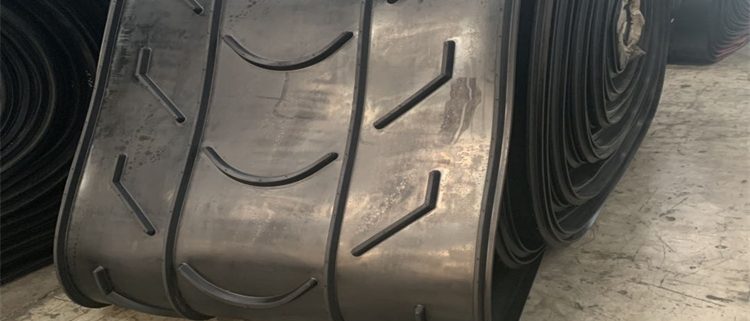
GRAM fabric conveyor belt with a raised working profile

Two chevron belt offers can share an overall width while describing different raised patterns. The quarry or distributor comparing them should ask for the actual offered profile layout before treating their dimensions as equivalent. A chevron rubber conveyor belt supplier needs the intended material, retained incline and complete belt construction. GRAM’s fabric belt range shows raised-profile options; use that route to establish the proposed pattern and base belt rather than infer them from the word chevron.

A photograph helps identify the kind of surface being discussed. A clear pattern description or drawing is needed to define the actual offered geometry. The buyer should be able to distinguish the complete belt width from the layout of the raised working profile.

A chevron rubber belt offer needs more than overall width

Overall width describes the outside belt dimension. The profile layout describes a different part of the working surface. Keep those descriptions separate when asking the supplier to reproduce a sample or propose a construction for a retained inclined conveyor.

For a quarry with only a removed sample, identify whether the sample represents the intended current pattern or merely the worn belt being replaced. A used profile may provide useful evidence without establishing the original geometry. Do not ask the supplier to invent a new nominal profile from an unlabelled worn section.

The profile’s working span is not automatically the full belt width

Ask the supplier to identify the proposed pattern across the belt and its relationship to the edges. A drawing should make clear which dimensions refer to the belt and which refer to the raised pattern. An outside width should not be used as a substitute for every profile dimension.

A distributor comparing equal-width proposals should keep the actual pattern differences visible. The customer needs to evaluate the proposed working surface for the intended material. A shared stock-width description does not establish the same raised layout or complete construction.

Profile height and base thickness describe different geometry

The raised feature and the underlying belt build need distinguishable descriptions. Ask what a quoted thickness includes. The buyer should not assume that a dimension including the profile is the same as the base construction’s thickness.

Where the proposal includes a dimensional drawing, retain its reference points and definitions. If the supplier gives only a total dimension, clarify the profile and base-belt meanings before comparing alternatives. This article does not supply a standard GRAM profile height or a universal measurement convention.

GRAM raised-profile fabric conveyor belt surface to define separately from overall width and base thickness
Define the raised pattern and the underlying belt as separate parts of the proposed construction.

Pattern direction belongs to the retained conveying arrangement

The drawing should show how the proposed profile is oriented in relation to the intended belt travel and material movement. A pattern photograph detached from that arrangement can be interpreted differently by the supplier and installer. Keep the intended orientation with the actual offer.

If the plant expects operation in more than one direction, state that requirement rather than infer suitability from a symmetrical-looking photograph. The accepted proposal needs the actual operating condition. Do not assume a generic chevron description establishes reversible duty.

The chevron conveyor belt supplier should compare the actual material duty

A raised pattern is not an automatic acceptance for every material on every incline. Provide the actual conveyed stream and retained arrangement. The supplier can then explain the proposed working profile and the basis on which it addresses that duty.

External profiled belt descriptions relate pattern choices to material and inclination. That general relationship helps frame the inquiry. The manufacturer’s profile heights, inclination claims, widths and production method are not GRAM specifications.

Drawing information What the buyer should keep distinct
Overall belt width The outside dimension of the complete belt
Raised pattern layout The span, orientation and shape actually proposed
Base construction The covers and reinforcing build beneath the profile
Application basis The actual material and retained inclined duty being assessed

A quarry moving from one screened stream to another should describe the revised material rather than simply repeat the previous pattern request. The old profile may remain a candidate, but its use needs an accepted basis for the changed duty. A raised surface alone does not eliminate that review.

For a contractor retaining the incline and changing the belt, keep the equipment record attached to the offered profile. Avoid converting another manufacturer’s advertised incline into a project acceptance. The actual GRAM proposal and responsible equipment review need their own basis.

GRAM’s belt routes help define the base beneath the profile

The GRAM conveyor belt range is a route for identifying the intended complete product. Use it with the specific fabric and rubber construction descriptions. A profile family does not define every reinforcing or cover feature of the belt underneath it.

EP reinforcement keeps polyester and nylon directions identifiable

GRAM EP rubber belts use polyester in the longitudinal direction and nylon transversely. If EP is proposed for the profiled belt, preserve the actual fabric build and cover description with the pattern. The EP letters alone do not establish a finished rating or profile geometry.

A buyer comparing two EP alternatives should therefore compare their complete proposed constructions. A shared reinforcing family can coexist with different base thicknesses or profile descriptions. Keep any such differences visible rather than collapse them into one generic chevron specification.

NN reinforcement is another declared fabric route

GRAM NN rubber belts use nylon in both fabric directions. That is a different declaration from EP. If the supplier proposes it as an alternative, identify the actual complete build and assess it for the retained equipment instead of assuming that the same raised pattern makes the bases interchangeable.

A distributor should preserve that distinction when passing the offer to the final customer. The customer needs to know whether the proposal changes the pattern, the base reinforcement or both. A generic “nylon reinforced chevron” description can conceal the difference between NN and EP.

Another GRAM profiled fabric belt image illustrating why the offered pattern and base construction must be identified
A profile image helps describe the surface; the accepted offer identifies the actual build.

Rubber cover requirements remain attached to the profiled offer

GRAM’s rubber belt range distinguishes the outer rubber construction from its reinforcement. The profile description should not remove the cover-duty requirement. A raised pattern does not prove suitability for every exposure of the conveyed material.

If the customer has a material-compatibility or specialist-cover requirement, keep it in the actual proposed complete belt. Do not combine a general profile photograph with a separate cover-family statement and present the combination as an accepted product. The supplier should identify what it is actually offering.

The profiled belt and retained return-path discussion covers equipment contact beyond the carrying surface. Preserve that review alongside the pattern drawing. A drawing that clearly defines the raised geometry does not, by itself, establish compatibility with the whole conveyor.

Approve the profile revision that will actually be supplied

Consider a distributor comparing two proposals for the same retained incline. One provides an overall width and a photograph; the other provides a drawing that distinguishes the raised pattern from the base. The buyer has different information to assess, not automatic proof that the second belt performs better. Ask the first supplier to identify the missing geometry, then compare the complete proposals against the material and equipment duty.

A worn sample also deserves a precise role in the enquiry. Mark which parts of its geometry are being reproduced and which original features are uncertain. If the remaining profile varies across the sample, do not present a single worn feature as a verified original nominal height. The supplier needs an accepted offered pattern rather than an invented reconstruction of the previous belt.

Where an existing drawing is available, check whether it identifies the pattern currently fitted or an earlier purchase. A changed profile may retain the same outside width. The contractor should provide the current record and show the proposed revision clearly, so the selected replacement is not ordered against a superseded pattern merely because the width appears correct.

If the supplier offers a different profile to suit the actual material, retain it as a proposed alternative until the project accepts it. Ask for its defined geometry and complete base build. A surface that looks similar in a photograph can still be a different working proposal, and the final order should not conceal that difference behind a shared chevron label.

If the supplier changes the pattern after the initial quotation, update the accepted drawing or description. Do not leave a sample photograph as the controlling reference while approving a different offered layout. The buyer and supplier need one identifiable current proposal.

Where the order includes several widths or destinations, keep the corresponding pattern references with each item. A consolidated dispatch can still contain different accepted builds. Agree how the supplied rolls will be identified so the receiving team does not infer their destination from a similar visible profile.

Before release, settle the outside width, the actual raised layout, the base construction and the duty to which that proposal applies. Compare the offer as that complete belt. Equal widths and the same chevron name are useful starting descriptions, but they are not the final procurement decision.

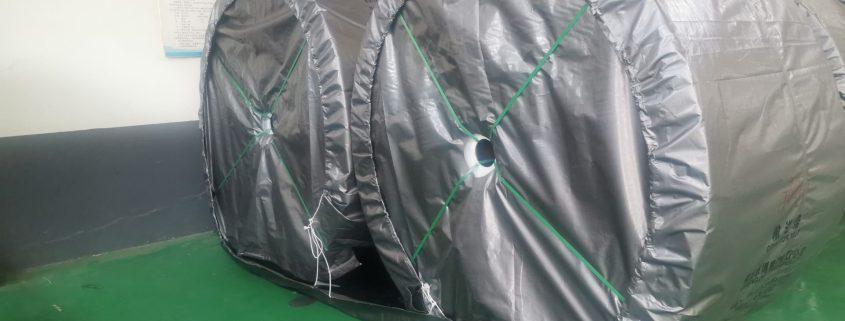
Wrapped GRAM belt rolls requiring identification of the actual supplied construction and form

Two rubber-cover wear figures cannot be compared usefully if the test basis is missing. A smaller number might describe less material loss, another method or a different reported quantity. Quarry and bulk-material buyers assessing an abrasion resistant conveyor belt supplier should establish what was measured before changing the cover specification. GRAM’s rubber belt range and EP constructions provide routes for that discussion. Bring the actual material and damage evidence as well: abrasion data alone will not settle a sharp-lump or loading-impact problem.

Make the abrasion resistant conveyor belt supplier’s numbers comparable

A result needs its method, reported quantity and sample identity. Request those details alongside the proposed cover description. Without them, the purchaser cannot know whether two figures describe the same kind of assessment or the rubber actually being offered.

For comparable volume-loss tests, lower loss indicates less rubber removed under that test. Fenner Dunlop’s wear discussion explains this interpretation and distinguishes wear mechanisms. It does not supply a test value for GRAM. No cover-loss number should be assigned to the proposed belt without its own applicable data.

Evidence received for the cover Comparison the buyer can make
Same method and quantity, identified proposed compounds Compare the reported loss within that test basis; separately assess suitability for the material duty.
Bare numbers, different methods or unidentified samples Request clarification before treating the values as equivalent performance evidence.

A distributor comparing offers for a quarry should preserve the result’s stated units. Do not rewrite a mass-based figure as a volume-based figure or convert an unexplained number into a cover grade. If a customer specifies a particular test requirement, compare the submission against that requirement instead of selecting whichever figure appears smallest.

The abrasion sample should represent the offered cover

The connection between a sample and the proposed rubber matters as much as the number. Ask which cover compound the result identifies and whether that is the one in the offer. A test on another compound or an unspecified catalog example does not establish the performance of the ordered cover.

Keep the upper and lower cover descriptions distinct. GRAM’s EP construction separates those covers from its textile carcass. If the material-contacting cover is being revised for wear, identify that revision directly rather than replace the complete belt description with abrasion resistant rubber.

Rubber belt roll illustrating the cover construction to connect with an abrasion result
The proposed cover must be identified in its own evidence. Appearance does not reveal a rubber-loss figure.

Abrasion-resistant belt selection changes when sharp material cuts the cover

Sliding wear and a local cut are different observations. Record whether rubber is gradually disappearing across a contact region or whether sharp material is creating distinct incisions and missing pieces. The supplier’s cover proposal should address the observed mechanism, rather than rely on one abrasion figure to answer every form of damage.

Sharp crushed stone raises cutting questions beyond volume loss

For a crushed-stone line, describe the material shape and size range together with photographs of the damage. A cover can have a reported wear result while the actual order still needs assessment for sharp-particle contact. Ask what evidence supports the proposed compound for that condition; do not infer cutting resistance from the abrasion number alone.

GRAM’s mining belt route is relevant to discussing bulk ore and demanding material duties. It is not a separate proof that every listed construction has a particular cut or abrasion classification. Connect the chosen reinforcement and cover to the described material rather than allow the application label to substitute for evidence.

Chunk loss at loading calls for a support review

When rubber pieces are lost near a transfer, include the landing condition in the assessment. Record where the material contacts the belt and what supports that region. An abrasion test is not a measurement of the complete loading arrangement, and a cover-only change can leave the original mechanical condition unexamined.

GRAM’s impact rollers use ringed working surfaces in the illustrated assemblies. They provide a different support route from a plain carrying roller. The loading-zone support range also includes beds, saddles and idlers. Their actual geometry and duty need engineering assessment; no generic support family is automatically a cure for chunk loss.

Rubber-ring impact roller assemblies illustrating a loading-support route
Ringed rollers change the belt-support arrangement at loading. They do not establish the abrasion performance of the cover.

For a quarry replacing both belting and loading supports, keep the two decisions separately stated. The belt proposal concerns construction and cover evidence. The support proposal concerns the actual assembly and its installation. Review their interaction, but do not describe a support purchase as an improvement in the belt’s laboratory abrasion result.

Keep EP reinforcement separate from the wear-resistant cover decision

The EP route identifies polyester longitudinal yarns and nylon transverse yarns. Its carcass provides a distinct part of the belt construction beneath the covers. Changing the proposed upper rubber does not settle the reinforcement requirement, and a reinforcement upgrade does not establish a new cover-wear result.

If the original carcass designation is to remain, state that in the revised order. If the supplier proposes another construction, obtain its actual specification and have it assessed against the conveyor. The GRAM rubber range includes fabric and steel-cord routes; neither should be silently substituted because the inquiry emphasizes abrasion.

Cover thickness and tested wear describe different things

Cover thickness is a construction dimension; a wear result describes behavior under a stated test. Request both when both matter to the order. A thicker cover is not proof of a better compound result, and a favorable laboratory result does not determine the acceptable thickness for the retained conveyor.

Ask the supplier to identify the proposed cover dimension and its tolerances in the agreed specification. Where the conveyor retains its pulleys, supports and cleaners, the responsible engineer must review the finished construction against those contacts. Do not estimate a new dimension from a worn belt surface or choose thickness solely from a generic product photograph.

A wear specification should preserve the agreed rubber result

When a tender requires a maximum reported loss under a named method, retain that requirement in the final cover proposal. Replacing it with a phrase such as premium wear rubber makes the acceptance condition less precise. Have the supplier identify the offered compound and applicable result against the requirement, without inventing a classification from the product family name.

If offers use different test descriptions, first determine whether the results can legitimately answer the same requirement. The buyer should not devise a conversion between unrelated methods to make the commercial comparison easier. Where clarification changes the offered compound, keep the revised compound identity attached to its revised evidence rather than combine the favorable number from one proposal with the price of another.

For a repeat EP order, this distinction also prevents a cover substitution from being hidden by an unchanged reinforcement designation. The belt can remain EP while the proposed upper rubber changes. The receiving record should therefore retain the agreed cover description as well as the fabric construction. If the delivered identification differs, resolve that difference before the belt is installed and its documents become separated from the shipment.

Carry the wear evidence into a material-specific belt trial

When a comparison on the actual conveyor is feasible and approved by the site, define the observed condition before the replacement runs. Record the construction, material duty and relevant support changes. Otherwise, a later difference in damage can be attributed to the new rubber when the loading arrangement or feed also changed.

The landing-zone roller discussion examines the support interface in more detail. Use that separate assessment when impact is part of the evidence. It should complement the cover review, not replace it with a different product claim.

For the next abrasion-resistant order, require a comparable test description, an identified cover and an account of the real material contact. If the main observation is cutting or chunk loss, make that condition part of the proposal. The smallest unexplained number is a poor reason to repeat a belt that is failing for a different mechanism.

Steel conveyor rollers stacked with bearing ends and shaft interfaces visible

Cement dust and kiln-adjacent heat are different reasons for a roller to need attention. A contractor evaluating a cement plant conveyor rollers supplier should map those exposures separately before choosing one replacement assembly for the entire plant. GRAM’s steel rollers, polymer rollers and suspended carrying arrangements provide product routes to compare. Start with the conveyor location, belt support geometry and actual conditions at the roller, rather than the plant’s general industry label.

The relevant enquiry may concern limestone handling, a dusty raw-material route or a transfer near a heated process. First confirm which duty applies. A roller’s temperature suitability cannot be inferred from a heat-resistant belt elsewhere on the same website, and a protected bearing should not be assumed immune to every dust or cleaning condition.

A cement plant conveyor rollers supplier needs a location-specific exposure

A cement works contains several conveying environments. Fine powder can enter spaces around end assemblies, while coarse material can impose different support and impact conditions. A nearby heated process can add radiant or conducted exposure that is not described by the material’s average temperature. Record each condition at the actual proposed replacement position.

A maintenance team replacing recurring bearing failures on a dusty raw-material conveyor should identify where the dust accumulates. Does it cover the roller body, reach the shaft ends or pack around the frame connection? That information helps define the end-protection enquiry. Visible deposits alone do not establish whether the body material needs to change.

Fine cement dust calls for an end-assembly discussion

GRAM describes polymer rollers with a machined tube or solid bar, sealed precision bearings, non-contact rubber seals and metal end caps. Those construction details make the proposed end arrangement worth reviewing alongside a steel alternative. Ask what exact assembly is offered for the dust condition and how its components are identified in the product documents.

Do not equate the phrase sealed bearing with unrestricted dust performance. The complete arrangement, installation condition and maintenance practice matter. Provide any cleaning method used around the ends, especially if the plant removes deposits with direct washing. Dust service that becomes wet during cleaning is a more specific exposure than a general dry conveyor description.

Coarse limestone transfers need a separate loading assessment

Where limestone or another coarse feed enters the belt, identify the landing location and support through the transfer. GRAM’s rubber-ring impact rollers have a different working surface from ordinary steel or polymer carrying rollers. Their role should remain tied to the loading zone rather than applied automatically along the whole conveyor.

A contractor should also record whether the chute or feed stream has changed since the original roller selection. The original frame may remain in place while the landing position moves. Copying its roller dimensions does not establish that the support still matches the incoming material. Have the transfer condition reviewed against the actual plant equipment.

Rubber-ring impact rollers for reviewing coarse-material loading support in a cement plant
Coarse material landing on the belt is a different selection problem from fine dust around bearing ends.

Cement conveyor roller selection must distinguish ambient and local heat

The temperature at a roller may differ from the plant’s reported ambient condition. Identify nearby equipment, material exposure and operating periods that affect the roller body and ends. A replacement proposed for a sheltered raw-material route should not automatically be accepted beside a heated process because its shaft dimensions match.

Polymer roller temperature suitability requires its own evidence

A contractor may consider polymer bodies for a dusty or moisture-exposed route, then propose the same spare near a kiln-adjacent transfer. That second position needs a separate assessment. Request the offered body’s and end components’ applicable thermal information. No resin name or general corrosion-resistance statement establishes the allowed temperature for the entire roller.

Record periods when the conveyor stops with material present or when nearby equipment remains hot. The assembly can continue to receive heat without the normal operating movement. The plant’s responsible engineer should define the credible exposure, and the supplier should identify the construction proposed for that condition.

Heat-resistant belt ratings do not become steel roller ratings

A conveyor belt and a roller contain different materials and have different functions. A temperature statement for a belt cover does not establish the bearing, seal or shaft arrangement’s thermal suitability. Keep their product documents separate even when both components are purchased for the same transfer.

Steel is a relevant body route to compare, but the word steel does not establish an unlimited assembly temperature. End components still need attention. Ask for the complete offered construction and the applicable limits instead of assuming that replacing polymer with a metal tube resolves every local heat requirement.

Review suspended cement carrying stations as complete garland sets

GRAM’s carrying garland range describes linked suspended roller groups and names limestone and clinker applications in cement production. These are useful application references. The actual set still needs to match the conveyor’s suspension, support geometry and operating conditions.

If the purchase covers a complete garland group, identify the links and suspension interfaces as well as the individual rollers. If it covers only selected rollers, check compatibility with the retained connecting components. A visually similar roller body may not define the complete set geometry or the required mounting arrangement.

For a plant holding mixed spares, separate suspended groups from rigidly mounted individual rollers in the item descriptions. Record the conveyor location and approved construction with the package identification. This prevents a nominal diameter from becoming the only basis for an urgent substitution.

Polymer conveyor roller assemblies for a separate review of dust, moisture and temperature suitability
Confirm the offered polymer assembly against its intended location; material choice alone is not an operating approval.

Preserve cement conveyor mounting references when changing roller construction

GRAM’s main roller range explains body, bearing and shaft considerations. For a replacement, record the mounting span, shaft end and belt contact geometry from the actual equipment. If a different body or end arrangement is proposed, compare its full envelope with the retained frame.

A deposit around the shaft seat can also affect the sample used for measurement. Inspect the mounting interface under the plant’s approved isolation procedure and distinguish buildup from the original seating surface. Where the old sample is worn or distorted, use the equipment drawing or an unworn matching assembly to establish the required dimensions.

The fines-at-roller-ends discussion is relevant to this evidence-gathering task. It helps describe contamination without assuming the same operating condition exists across every plant line. A cement enquiry should retain its own dust composition, local heat and mounting information.

Ask for cement-duty evidence that corresponds to the offered assembly

An offer should identify the body material, bearing arrangement and protective end components that will actually be supplied. If the supplier proposes a modification for the dusty position, have it shown in the assembly record. General statements about durability should not replace a description of what has changed and which duty it is intended to address.

Rulmeca’s cement and quarry application information provides external context for the variety of bulk-material conveyor environments. Its project results and product capabilities belong to Rulmeca. They are not evidence of GRAM customer performance or a thermal rating for a GRAM roller.

Dust removal and inspection need the plant’s approved procedure

Close inspection, cleaning and replacement must be carried out with the equipment isolated as required by the site. Do not infer a maintenance method from the roller material. Provide the supplier with the cleaning procedure that affects the assembly, and obtain any product-specific instructions needed for the offered end construction.

If the plant changes its cleaning practice after the roller was selected, review that exposure change before repeating the order. A previously dry dust condition may become a wet deposit around the ends. Keep the current operating description with the replacement specification so the next purchase does not rely on an obsolete assumption.

Deliver cement roller replacements by exposure and conveyor position

For a plant purchasing spares for several cement routes, the supplier evaluation should preserve the differences that justified each construction. Put the dusty raw-material position and any heat-exposed transfer in separate item descriptions, even if their frames use the same nominal roller size. This lets the buyer compare the intended offered components instead of assuming one undifferentiated cement roller can cover both.

A proposed construction change should be identified before the repeat order is accepted. For example, a different end cap or bearing protection arrangement may matter at the dusty position even when the body dimensions are unchanged. The buyer needs to know what changed and which operating condition was used to approve it. A visually similar delivered assembly does not answer those questions.

Where replacement access is restricted, include the removal space in the drawing review. A cement deposit, adjoining guard or nearby chute can make an otherwise compatible assembly difficult to remove through the approved maintenance route. Resolve that practical installation issue before choosing the final body and end arrangement, without altering the conveyor’s safety provisions to accommodate the spare.

Inspect delivered shaft ends, body condition and rotation against the approved assembly record. Where dust protection or thermal suitability drove the choice, verify the supplied components against the declared construction. Separate any undocumented substitution before installation; matching tube dimensions alone is not enough.

Agree packing that protects bearing ends and projecting shafts, with packages identified by conveyor position. If dusty raw-material and heat-exposed replacements arrive together, keep their assembly descriptions distinct during storage. A common frame size should not erase an important operating boundary.

Send the supplier a cement-plant position list with dust and local heat recorded separately. Choose the roller route for each actual location, preserve the frame references and obtain the offered assembly’s applicable evidence. That allows purchasing to compare real alternatives without treating the entire plant as one interchangeable cement duty.