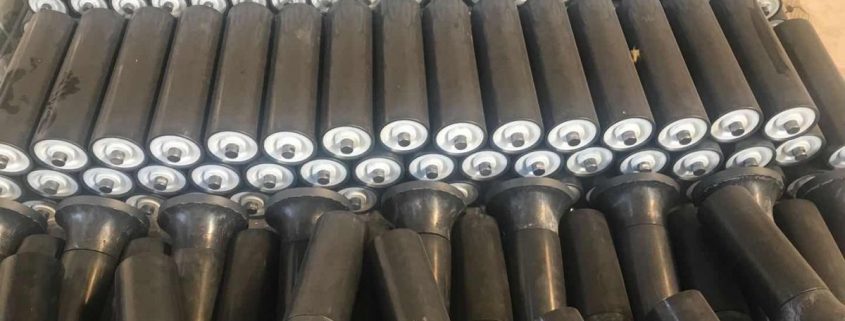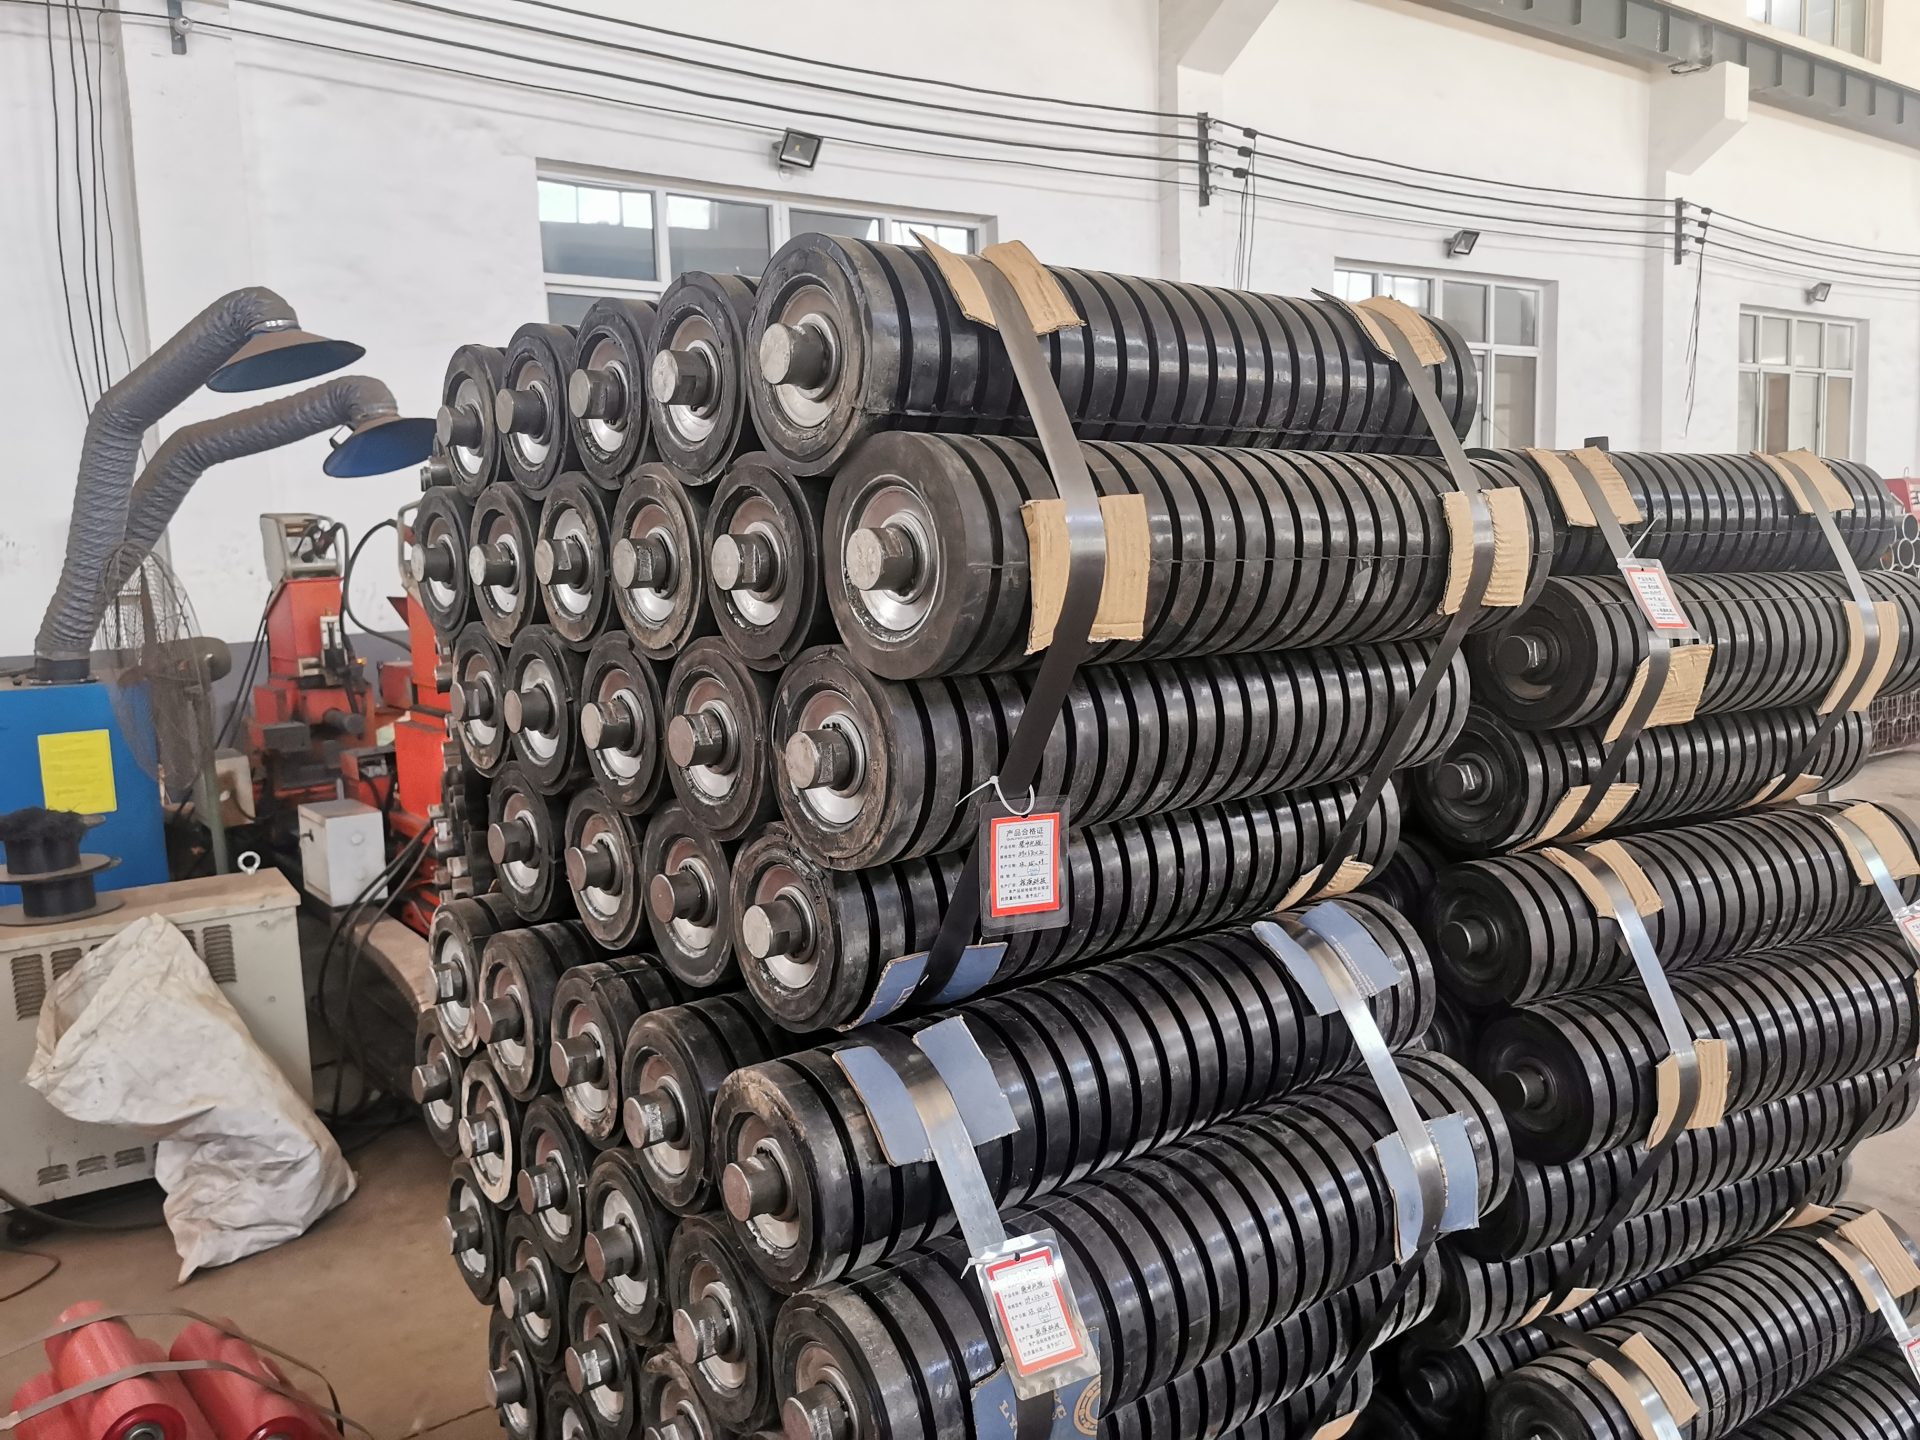
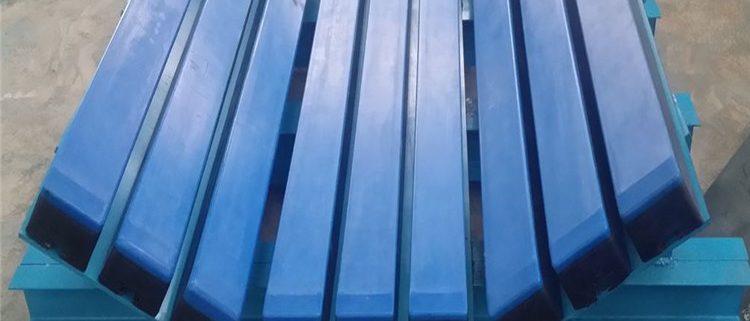
Conveyor load-zone impact bed with longitudinal bars and inclined side supports

The impact bed fits beneath the belt, but a worn support bar cannot be withdrawn without removing nearby structure. An aggregate transfer-point contractor should resolve that problem before choosing a conveyor impact bed supplier for a retrofit. GRAM’s loading-zone belt support range includes beds, saddles and idlers. For an impact-bed proposal, start with the retained frame, belt geometry and the actual component removal method. Installation clearance and future service clearance are two different approval questions.

A bed can be the intended support route while its proposed arrangement remains unsuitable for the available space. The retrofit review should explain how the unit will be mounted, how the belt will be supported during approved maintenance and how the wearing components can leave the installation. A drawing that shows only the assembled bed under the conveyor does not answer those questions.

Ask the Conveyor Impact Bed Supplier How a Worn Bar Leaves the Installation

GRAM’s existing bed photographs show longitudinal supporting bars on fabricated frames, with central and inclined side regions. Those visible components make a useful starting point for an access discussion. They do not identify a universal withdrawal direction or a standard modular removal feature. Ask how the particular proposed unit is serviced.

The Bar Removal Direction Needs a Defined Clearance Envelope

A contractor may have enough room to bring a complete bed into an unfinished transfer point but much less room after skirts, guarding and adjacent equipment are installed. Identify the proposed withdrawal direction for the actual wearing component. Then compare the required movement with the completed installation, not with the space available during initial construction.

If a bar slides out, the reviewer needs its removal route and the parts that must first be released. If another method applies, document that method instead. Do not infer the service arrangement from the fact that the bars appear separate in a photograph. The offered construction, fixings and access requirements must agree.

Show obstructions along the removal path: retained steelwork, chute supports, cables, guarding and other equipment. Identify which are fixed and which can be removed through an approved maintenance procedure. A service path relying on dismantling unrelated structure should be visible before the installation is accepted as a maintainable retrofit.

The fixing access belongs to this review too. A bar may have a clear withdrawal path while its retaining feature remains unreachable behind a chute member. Ask which tools and approach directions the actual construction requires, then assess that access against the finished structure. If the drawing assumes access from below, show what occupies that space and how the approved maintenance arrangement reaches it.

This keeps the removal assessment specific to the offered bed: movement clearance and fixing access must both exist for its wearing component.

For a mine maintenance engineer, the important distinction is not whether a technician could somehow extract the component. It is whether the proposed method is workable under the site’s approved equipment-control and access procedures. A supplier drawing cannot replace the site’s safe method for isolating the conveyor and supporting the belt.

Side-region Components May Need Different Access from Central Bars

The inclined side regions shown in GRAM’s bed photographs do not occupy the same geometry as the central region. A proposed removal method should identify how each relevant component is reached. Access to a central bar alone is not evidence that a side-region component can be exchanged within the retained structure.

At a narrow transfer station, a skirt or frame member may obstruct a fixing on one side while the other side is open. Record both sides rather than presenting the more accessible side as representative of the whole bed. If the proposal requires a removable part to create access, include that part and its approved scope in the retrofit design.

Impact belt support frames with longitudinal bars arranged across central and inclined side regions
The central and inclined support regions need their own component access assessment.

The Conveyor Impact Bed Supplier Needs the Retained Mounting Structure

Once the service path is understood, establish how the complete unit mounts to the conveyor. GRAM’s photographs show fabricated support structure and mounting feet. Their appearance does not establish hole spacing, fixing capacity or compatibility with the existing steelwork. Those particulars belong in the offered unit’s drawing and the project’s structural review.

Mounting Feet Must Match an Approved Load Path into the Frame

A buyer retaining the lower structure should show the mounting locations and the condition of the available supports. Compare the proposed feet, fixing arrangement and installed height with that structure. Do not treat an apparently convenient hole position as approval of the load transferred through it.

If the original support was a roller station, the bed’s attachment and load distribution may differ. The engineer should assess the complete change, including any new cross-members or other approved supporting work. A component that fits between the conveyor sides can still require an installation scope beyond replacing the old rollers.

Keep existing damage visible in the review. A worn, deformed or repaired support should not become an unquestioned reference just because it is staying on the conveyor. Establish which retained elements are serviceable and which must change before the bed proposal is approved.

Bed Height Should Be Reviewed Against the Intended Belt Path

The installed height affects how the belt meets the support and adjacent stations. Identify the intended belt path, retained equipment and the proposed support position on the same drawing. A bed that can be bolted down is not necessarily positioned correctly for the working belt.

A contractor replacing several support elements should distinguish a true retrofit drawing from a catalogue outline. The retrofit drawing needs to show the bed’s relationship to the conveyor, including the transition to retained support upstream and downstream. If that relationship depends on an adjustment, identify how the offered assembly achieves it.

Do not invent a universal support gap from product photographs. The appropriate installed relationship belongs to the selected construction and the engineering agreement. The purchase should carry those agreed requirements so the installation team is not asked to create them after the parts arrive.
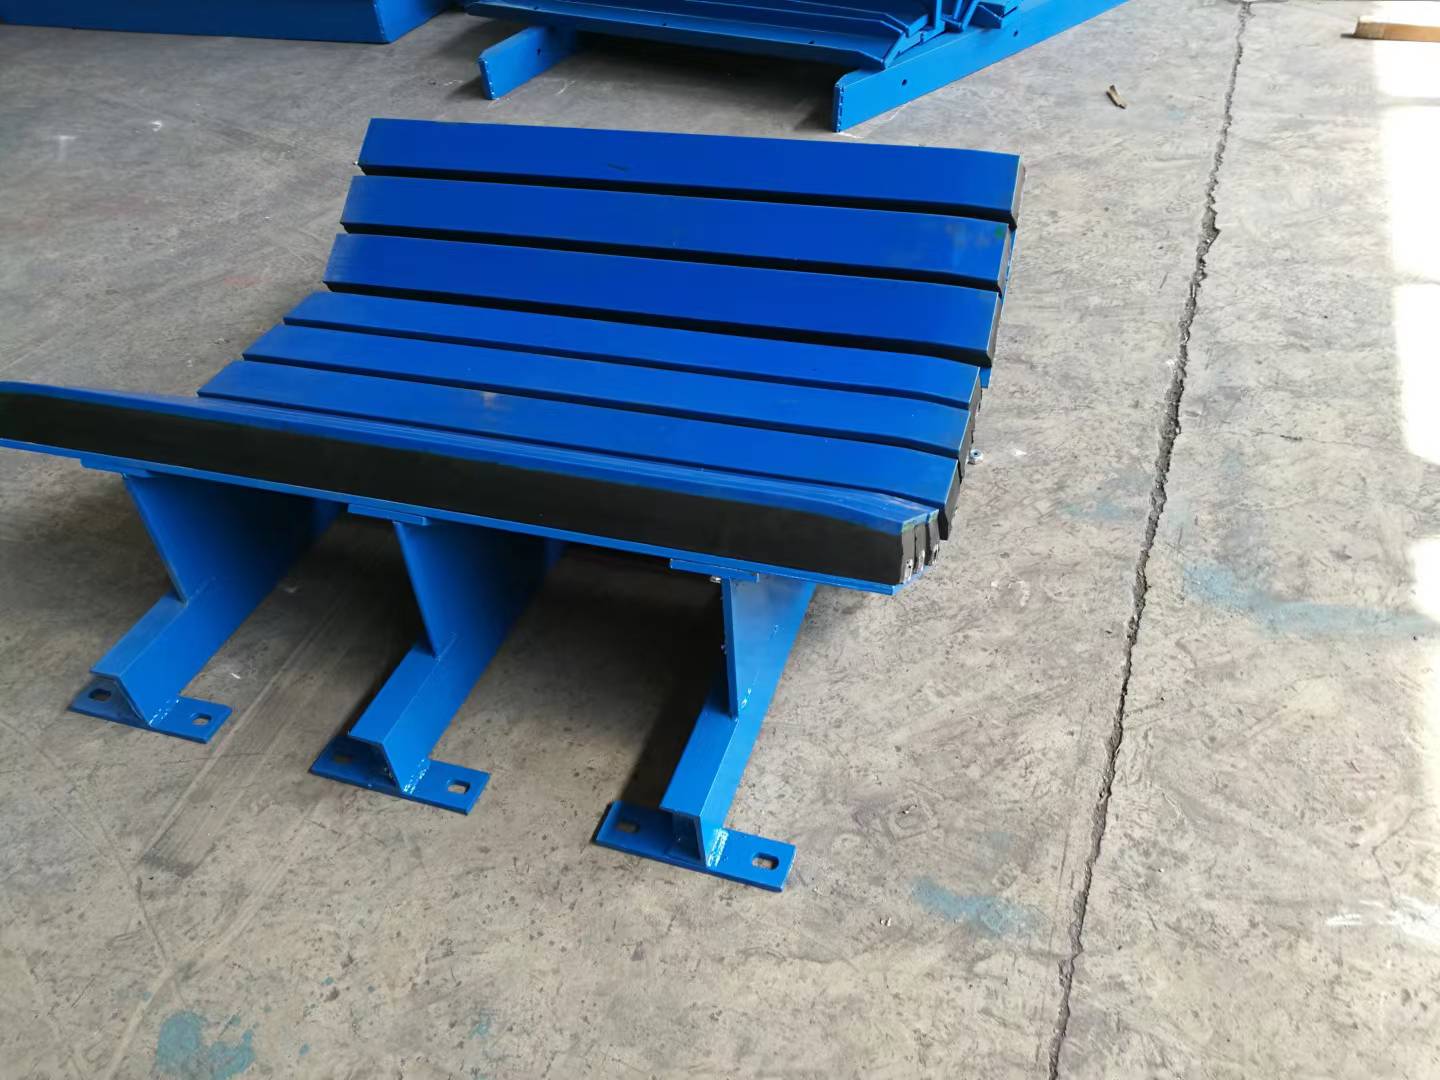
Blue impact support assembly with longitudinal bars and mounting feet visible on the floor
The visible feet are a starting point for a mounting review, not a complete fixing specification.

Confirm the Belt and Adjacent Supports Before Freezing the Retrofit

The bed is selected for the belt and loading duty, not as an isolated frame. Record the belt width, construction and intended trough relationship alongside the proposed assembly. GRAM’s mining conveyor belt range offers relevant belt routes, but a range name does not establish compatibility with an unnamed support unit.

Retained Carrying Rollers Still Define the Approaches to the Bed

GRAM’s steel carrying rollers are a separate rotating support family. Where those rollers remain beside a new bed, their geometry and condition belong in the retrofit review. The transition should be assessed as a relationship between the bed, belt and adjacent supports.

If the retained roller station has moved or deteriorated, a bed drawing referenced to its current position can preserve an undesirable belt path. Establish the intended condition after any support repairs. Then confirm that the proposed bed and remaining rollers belong to that approved geometry.

For a transfer-point maintenance buyer, also identify whether the belt construction is staying. If a belt change and a support change are planned together, the bed should be assessed against the proposed belt, not only against the removed one. Keep the two supply scopes connected in the engineering record.

Rubber-ring Impact Rollers Remain a Distinct Support Alternative

GRAM’s impact roller assemblies use a rotating, ringed support route. A bed and an impact roller station should not be treated as equivalent simply because both are considered for loading duty. The chosen route must fit the approved material-support and installation requirements.

This distinction also affects maintenance scope. A roller replacement and a bar replacement involve different components and access arrangements. If a project changes from one route to the other, explain the future wearing-component supply and service method as part of the change rather than leaving it to the maintenance team to discover.

Metso’s conveyor solutions handbook treats impact support as a defined conveyor component selection. Its assemblies and ratings belong to Metso. The general engineering point is to approve support for the actual loading position, while the retrofit additionally needs the particular unit’s mounting and service arrangement.

Define Which Impact-bed Components the Retrofit Order Supplies

GRAM’s conveyor accessories range provides a broader route for the associated component discussion. For the actual bed, the order should identify the assembly, wearing parts, fixings and any agreed supporting components. A picture of a complete unit does not establish what a particular quotation includes.

  • The offered bed assembly: the exact frame and support arrangement identified on the approved drawing.
  • The wearing components: the actual bars or other parts, their identifiers and their confirmed replacement method.
  • The mounting boundary: supplied fixing components and the retained or separately modified conveyor supports.
  • The service boundary: removable parts or access provisions required for the agreed component replacement.

If a quotation covers only replacement bars, confirm that they suit the retained assembly. Similar length and appearance do not establish matching fixing geometry or contact construction. Obtain confirmation of the actual compatibility rather than using a material colour or a generic “impact bar” description as the acceptance basis.

Conversely, a complete new frame should not inherit an old bar approval without review. A change to the supporting arrangement can change how the components are fixed and presented to the belt. The approval record should identify the new complete arrangement and the specific wearing parts that belong to it.

Plan Delivery Around the Bed’s Actual Assembled and Service Dimensions

The assembled unit’s handling envelope and the wearing component’s removal envelope are different. Keep both available for the contractor. The first helps establish how the unit reaches the mounting position; the second helps establish whether the finished installation can be maintained.

Ask how the proposed assembly will be supplied and protected in transit. The actual unit mass, lifting information and package dimensions should support the unloading and placement plan. The existing photographs show bed structures on the floor, not approved lifting points or a prescribed transport arrangement.

If bars or mounting parts travel separately, identify them by the assembly reference and intended position. Keep those identifiers with the components during unpacking so the installer can match them to the drawing. A collection of similar-looking pieces is not a complete installation instruction.

At receipt, compare mounting geometry and supplied components with the final approved revision. Record visible damage to the frame, contact surfaces or fixing features before placement. Resolve an unapproved change while the assembly is accessible, rather than after it has been enclosed by skirts and guarding.

Accept an Impact-bed Retrofit That Can Be Serviced in Its Finished Position

The existing loading-zone impact bed explanation provides broader context for support selection. For the retrofit, the decisive record is more specific: the offered assembly, retained mounting structure, belt relationship and confirmed wearing-component removal path.

Before approving the installation, compare that removal path with the completed conveyor arrangement. Identify any agreed removable obstruction and keep its scope in the maintenance documents. If access exists only before the transfer point is completed, the design has answered the installation question but not the service question.

Release the bed order when the contractor can explain how it reaches its mounting position and the maintenance team can explain how its wearing parts leave that same position later. That is the practical difference between a component that fits under the belt and a retrofit the site can continue to use.
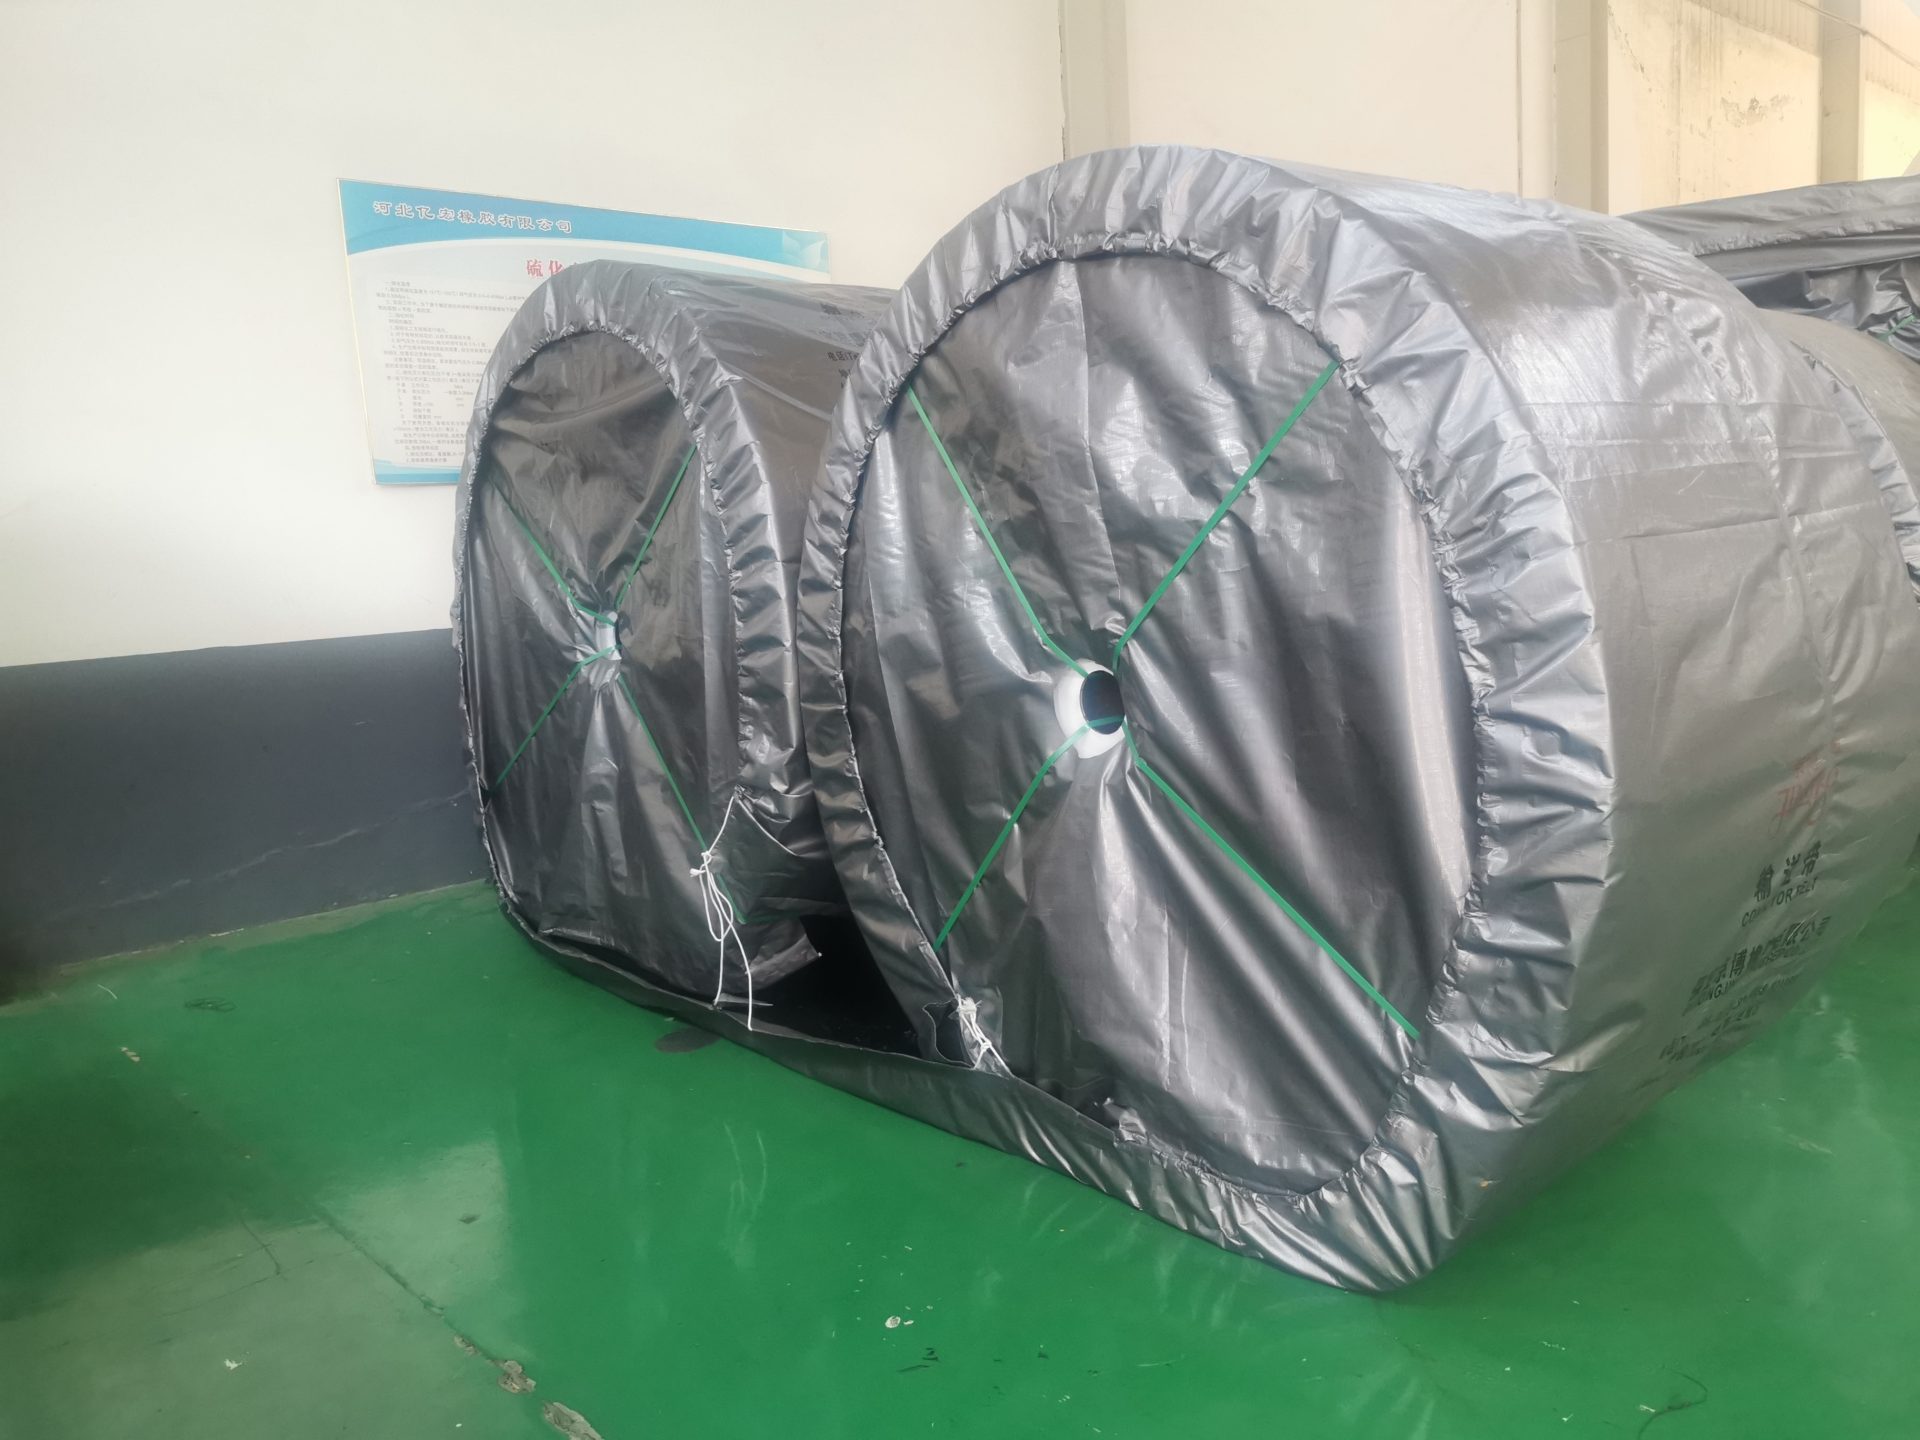
Bulk material conveyor belt supported by troughing rollers along the carrying run

Dry fertilizer granules and a damp blended product can behave differently on the same conveyor. A buyer selecting a fertilizer conveyor belt supplier should identify the conveyed chemistry, moisture and temperature before treating a general rubber belt description as suitable. GRAM’s rubber conveyor belt range includes fertilizer handling, while its HR route discusses relevant process applications. Start with those ranges and the actual material condition, then define the reinforcement and cover required by the equipment.

The relevant buyers include blending plants, maintenance teams and distributors supplying agricultural-material handling. First establish what touches the belt, including additives and credible residue. The supplier should identify the offered complete construction for that exposure; no generic oil-resistant or chemical-resistant label should become a promise of compatibility with every fertilizer.

A fertilizer conveyor belt supplier needs the conveyed formulation

Provide the product description and relevant process information through the plant’s approved technical channels. Where compatibility or safety documentation is required, use the actual material documentation and responsible engineering review. An informal name such as fertilizer does not establish the chemistry that the cover will meet.

Granules, dust and additives should be declared as separate contact conditions

A granulated product may also contain loose fines or an additive that changes the surface residue. Tell the supplier which condition is normal and which is associated with handling or storage variation. The cover enquiry should refer to that defined exposure rather than assume the visible granules describe everything contacting the rubber.

A distributor receiving enquiries for several fertilizer blends should preserve their material descriptions separately. The same conveyor width does not establish chemical equivalence. Keep the customer’s approved exposure and the offered cover specification linked so a later repeat purchase does not substitute a belt selected for another formulation.

Damp fertilizer requires more than a dry-product label

A blending plant receiving material after outdoor storage may see a different residue from its normal dry feed. Describe the moisture condition and where the material contacts the belt. If the wet condition is occasional but credible, include it in the engineering assessment rather than supplying only the easiest operating case.

Do not infer that water alone explains every change in belt behavior. The actual mixture, contact duration and cleaning exposure need to be considered. Ask the supplier to identify the offered compound and relevant compatibility information instead of assigning a universal chemical-resistance claim to the whole range.

Fertilizer belt selection should keep the cover and fabric requirements distinct

The cover meets the product; the reinforcement provides the belt’s mechanical construction. GRAM’s EP rubber belt uses polyester warp and nylon weft. Its NN rubber belt uses nylon in both directions. Those distinctions help identify the fabric routes, but they do not establish compatibility with a particular fertilizer mixture.

EP reinforcement should match the conveyor’s approved mechanical duty

Provide the required width, route and retained pulley and take-up information. The offered EP construction needs to be defined beyond its fabric name, with the applicable cover arrangement and reinforcement details. Have the complete belt checked against the equipment requirements through the responsible design process.

If the original specification is unclear, obtain the equipment records or a suitable assessment of the existing belt. A black working surface does not establish the fabric inside. The purchase should result in an identifiable complete belt, not an instruction to reproduce an unspecified fertilizer roll.

NN fabric is another construction route, not a chemical protection certificate

If NN is proposed, assess its complete offered construction against the same mechanical duty. Do not interpret its nylon reinforcement as a declaration that the cover resists the customer’s formulation. The material-contact and reinforcement decisions should both be documented, with neither used as a shortcut for the other.

A buyer should also identify any construction change from the original belt. A different fabric, cover or overall arrangement can affect the required joining and installation assessment. Ask the supplier to identify the proposed change before the belt is accepted as an equivalent replacement.

Wrapped conveyor belt rolls illustrating the need to identify the actual fabric and cover construction for fertilizer handling
Preserve both the reinforcement description and product-contact requirement on the delivered belt identity.

Warm fertilizer process feed needs a separate thermal assessment

GRAM’s HR rubber belt range includes fertilizer-industry applications. That makes the heat-resistant route relevant where the actual feed is warm or hot. It does not establish a single temperature limit for every offered belt or prove chemical suitability for a particular formulation.

Warm granules should be described at the belt loading point

Identify the material condition reaching the conveyor, not only a temperature reported elsewhere in the process. Include the credible exposure duration and any state in which material remains on a stopped belt. The responsible process team should establish the requirement; the supplier should provide applicable information for the offered complete construction.

A distributor supplying both stored granules and warm process feed should keep those requirements separate. The same nominal belt width may appear in both enquiries, but that does not create one shared cover approval. State whether heat, chemistry or both drive the selection for each item.

Sticky fertilizer residue should be discussed with the cleaning arrangement

If material adheres to the belt after discharge, identify the residue and the point where cleaning acts. GRAM’s conveyor accessories include a polyurethane cleaning route. That is a separate component enquiry which needs its own material, installation and maintenance information.

Polyurethane cleaner suitability should follow the real fertilizer residue

A cleaner’s blade material should not be assumed compatible with every fertilizer simply because the belt cover has been selected for the product. Provide the actual residue and operating conditions to the cleaner supplier. The offered blade and assembly require their own applicable information.

Also identify the belt surface and joining arrangement that the cleaner will meet. An equipment change can alter the cleaning interface even when the nominal width remains unchanged. Coordinate the belt and cleaner enquiries against the same intended process, without claiming an unspecified cleaning efficiency.

Polyurethane conveyor cleaner assembly for a separate assessment of fertilizer residue and belt contact
The cleaning assembly needs its own compatibility and installation review.

Read fertilizer compatibility evidence as product-specific information

The fertilizer and chemical-duty discussion is relevant to preparing a detailed enquiry. Any resulting claim should identify the offered belt and the exposure assessed. Do not extend a result for one mixture, temperature or contact period to an undefined family of products.

Dunlop’s belt range literature distinguishes cover duties and reinforcement options. It supplies professional context for keeping those choices separate. Its compounds and product performance are not GRAM evidence and should not appear as GRAM model capabilities.

Where the project needs a defined compatibility test or document, state that requirement before approving supply. If the available evidence does not address the actual combined exposure, retain it as an unresolved approval item. Purchasing should not turn an incomplete test description into a blanket resistance promise.

Preserve the fertilizer belt exposure record through delivery

Fertilizer formulation changes belong in the next belt enquiry

A blending plant may introduce a new product while keeping the same conveyor and replacement dimensions. Compare the new contact condition with the one used to select the existing cover. Provide the changed formulation, additives, moisture and temperature through the appropriate technical records. The supplier needs that information before the old belt can be treated as suitable for the new service.

Cleaning changes should be identified separately. A cover that meets the conveyed product may also contact a different cleaning mixture during shutdown. Ask for the offered belt’s applicable information for that exposure instead of assuming the fertilizer-duty description includes every cleaning process used at the site.

A proposed alternative should identify any changed cover or reinforcement. The supplier should not combine chemical information for one compound with the construction description of another into an apparent equivalent. The buyer’s approval needs to concern the complete offered belt and the actual combination of exposures.

For a distributor serving several fertilizer customers, avoid keeping only a generic product category in the stock description. Record the customer’s approved construction and exposure boundary. A roll with matching width and length can still have a different cover. Assess a substitute against the actual material contact before it is released for that customer.

If compatibility information is incomplete, the purchase can still progress the confirmed dimensions and delivery questions while retaining the material-contact approval item. Do not fill the gap with an unverified resistant-to-all-chemicals claim. Obtain the relevant product or engineering evidence before the belt is accepted for the unresolved exposure.

Agree the supplied length and form, joining responsibility and required identification. Match the delivered reinforcement and cover description with the approved item. Inspect accessible surfaces and edges for damage using the agreed handling procedure, and retain the relevant product and storage instructions.

Ask how the belt will be packed to protect it from unrelated contamination during shipment and storage. A fertilizer-duty label is not permission to expose the delivered belt to unspecified chemicals before installation. Keep the packaging identification readable so different cover constructions do not become mixed spares.

Send the supplier the actual granule chemistry, moisture and temperature together with the conveyor specification. Approve the cover for that exposure and the reinforcement for that equipment, then coordinate the cleaning and joining interfaces. If the fertilizer formulation or moisture changes later, update that record before repeating the order.

Wrapped roller assemblies in the GRAM ceramic range with circular end plates and projecting shaft ends visible

A request for ceramic rollers can leave the most important part of the order undefined: what is ceramic, what it contacts and what complete assembly will arrive. Industrial buyers comparing a ceramic conveyor rollers manufacturer should settle those questions before treating the material name as an upgrade. GRAM has a ceramic roller route alongside other conveyor roller families. Begin with the intended working contact and an identified proposed construction. A ceramic description does not, by itself, establish a load rating, impact duty or approval for a hot process.

A ceramic conveyor rollers manufacturer should define the working surface

Ask which part of the offered roller is ceramic and how that part is constructed. The inquiry should distinguish a ceramic working region from the remaining body, ends and shaft interfaces. Do not assume that a surface-material description means every part of the assembly has the same material or exposure capability.

GRAM’s ceramic discussion mentions alumina. That material name alone does not identify the composition, purity, finish or construction of an individual offered roller. Obtain those details where they are relevant to the intended contact, without adding an assumed composition or hardness to the order.

Ceramic material and roller surface finish need separate descriptions

The material designation and its working finish answer different questions. The buyer needs the proposed finish defined for what the roller will touch, whether that is a conveyor belt or another identified process contact. A broad statement about smoothness cannot establish the required surface condition for every installation.

CoorsTek’s technical materials information explains ceramic selection in relation to component requirements and manufacturing methods. This is general design background; its formulations, processes and capabilities are not GRAM supply facts. For the GRAM proposal, ask for the actual offered construction rather than borrow an external material specification.

For a maintenance team considering ceramic after repeated working-surface wear, record the existing contact and wear location. Ask what part of the proposed ceramic construction addresses that condition. A material change should have a stated purpose, not simply replace the old roller’s name with a harder-sounding description.

Review the complete ceramic roller assembly before retaining the frame

A surface proposal still has to belong to an assembly that fits and works in the intended position. GRAM’s ceramic photographs show individually wrapped cylindrical assemblies with projecting shaft ends. The photographs identify visible form, but they do not establish hidden bearing details or the dimensions of the proposed order.

Shaft extensions and mounting features must match the proposed drawing

Define the shaft interfaces and the installed mounting arrangement for the actual replacement. Identify working-face length separately from total assembly length. A ceramic-surface proposal cannot resolve an incorrect shaft extension or a mounting feature that does not fit the retained frame.

For a buyer preserving the original frame, supply the accepted drawing or reliable interface measurements and mark uncertain information. Ask the manufacturer to state any difference in its proposed assembly. Do not approve the ceramic material against one description while the site expects another shaft arrangement.

The ceramic contact diameter should refer to the finished assembly

The contact diameter needs to describe the supplied working surface, not an unidentified underlying component. Ask the supplier to state the finished dimension and the inspection basis applicable to the offered construction. Do not estimate a surface thickness or diameter from the wrapped product photograph.

If the proposed construction changes the contact position or clearance, have that effect reviewed on the conveyor. Retaining a frame does not prove that any roller of approximately the same visible size will work in it. The fitted assembly and its intended duty remain part of the acceptance.

Compare ceramic, steel and polymer rollers for the actual contact problem

Different material routes are useful when the buyer can explain what needs to change. GRAM lists ceramic, steel and polymer rollers separately. Compare proposals for the same identified role and contact before choosing a construction; do not compare the material names while allowing the duty to change between offers.

A steel roller proposal provides a separate construction baseline

The steel roller offering is a distinct route for a buyer reviewing a replacement. If an existing steel working surface is wearing, preserve the old construction and operating history as the comparison baseline. Ask how the proposed ceramic option differs in the region that matters to that wear observation.

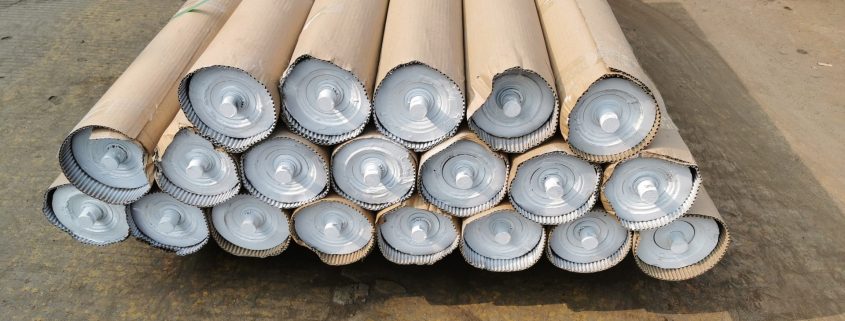
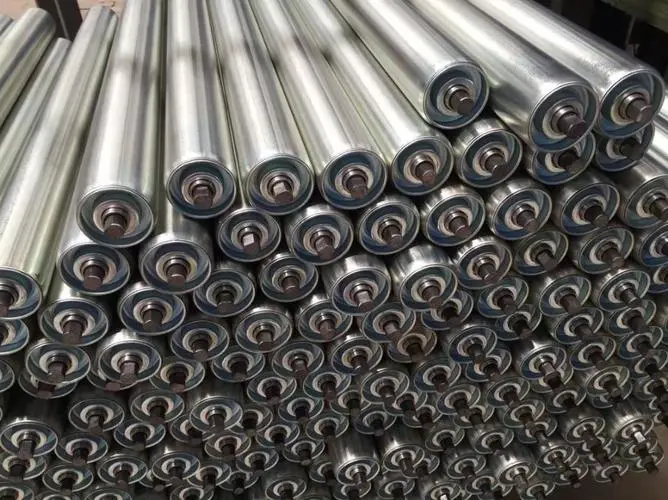
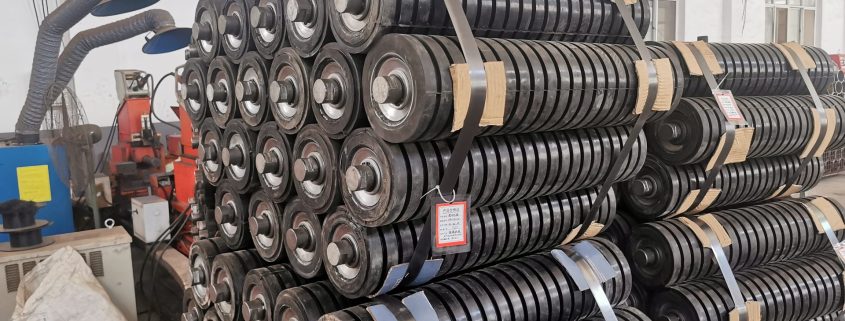
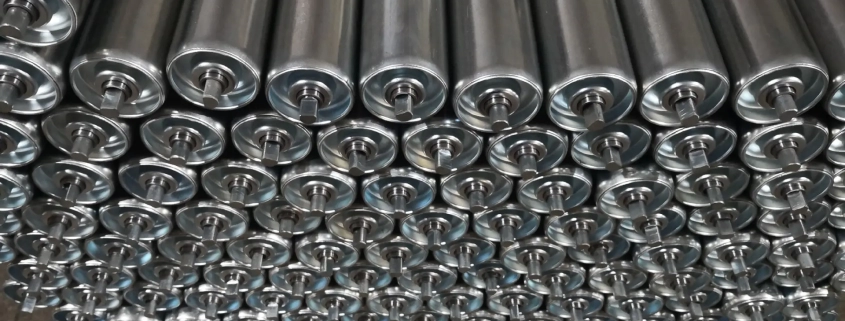
Stacked steel conveyor rollers illustrating the separately defined steel construction baseline
The steel route supplies a comparison construction, not proof of the ceramic proposal’s duty rating.

Do not attribute every observed difference to the working material if the proposals also change bearing arrangement, dimensions or operating conditions. Keep those differences visible. Where the real concern is an end-component failure, a new working-surface material may not answer the problem that caused the replacement.

A polymer roller body leaves other assembly components to assess

GRAM’s polymer route describes body, end, bearing and sealing components. That shows why a body-material choice is only part of the complete roller assessment. Compare the actual proposed assembly with the ceramic offer rather than assume that a polymer label describes every component.

Polymer roller assemblies showing another material route to assess against the intended contact
Keep the polymer construction identifiable when comparing it with a ceramic working-surface proposal.

For a distributor receiving alternatives, retain each proposal’s drawing and material identity. The customer should be able to distinguish the ceramic working-region proposal from the steel or polymer assembly offered beside it. An alternative price does not establish interchangeability.

Ceramic wear claims do not establish impact or kiln duty

Wear, impact and hot-process requirements are different conditions to assess. A description of ceramic wear resistance is not sufficient evidence of suitability for every loading event or temperature. Tell the supplier the actual position and duty and request the supporting construction information that the responsible engineer needs.

Rubber-ring impact rollers remain a different loading-support route

GRAM’s impact assemblies visibly use rubber-ring working surfaces. That is a separate construction to discuss for a loading-support problem. A ceramic offer should not replace it solely because the buyer wants greater wear resistance; the actual loading duty and compatibility must be reviewed.

The roller-family discussion helps keep the intended working role identifiable. Use that distinction when a purchase request has combined material selection and roller position into one short description.

Protect the identified ceramic surface through receiving and fitting

Agree handling and package protection for the actual offered ceramic construction. The working surface should remain identifiable and available for the agreed inspection, while the shaft interfaces receive protection appropriate to the supplied assembly. Do not derive a lifting method or allowable impact from a photograph of wrapped rollers.

If an agreed sample establishes the surface finish, keep it identified with the proposed construction revision and the acceptance description. Its role is to provide a comparison for that surface requirement, not to prove the production assembly’s bearing performance or load capacity. Ask how the delivered rollers will be checked against the agreed surface and dimensions. Where the supplier changes the ceramic construction after the sample is accepted, reopen that comparison instead of applying the old surface acceptance to an undefined replacement.

At receipt, compare the assembly and records with the accepted surface and drawing description. If damage, a visible surface difference or an unexplained construction substitution appears, resolve it before installation. The inspection should follow the offered object’s actual acceptance conditions rather than a generic promise that ceramic is durable.

Ask for the surface description, assembly drawing and intended contact to be agreed together. If the manufacturer answers only ceramic roller, the order still lacks a defined object. Release the replacement when the proposed working surface and the complete fitted assembly answer the original wear or contact problem.

Steel conveyor rollers stacked with bearing ends and shaft interfaces visible

A drawing marked “roller length” can refer to the tube, the working face, the full assembly or the shaft. Those are not automatically the same dimension. Before a custom conveyor rollers manufacturer starts production, agree which surfaces locate the roller in the machine. GRAM’s roller offering includes fabrication to customer specifications; engineering buyers and equipment builders should supply an unambiguous assembly definition, then compare the steel, polymer, nylon or impact route against it. A single length written beside a photograph is a weak basis for approving a custom component.

A custom conveyor rollers manufacturer needs to know where the dimension starts

Identify the actual dimension being requested and its endpoints. If the customer gives only a number and the word length, the supplier may interpret a different part of the assembly from the designer. Resolve that ambiguity before pricing or manufacturing instead of expect the receiving team to recognize it after the components arrive.

Tube length is not necessarily the usable roller face

The rotating body can have end regions or additional working-surface elements that make a simple tube measurement insufficient. Show the required belt-contact region in the assembly drawing. A measurement of the body should not be presented as a complete definition of the working face unless the intended construction makes that relationship clear.

For a contractor replacing components in retained brackets, the removed roller can help explain the existing arrangement. Keep its measured condition separate from the requested new geometry. A body damaged or worn at one end does not provide an unquestionable reference for the original face dimension.

Body or tube dimension
The specified endpoints on the rotating body; identify exactly which surfaces the drawing uses.
Shaft projection and end geometry
The portions outside the rotating body and the particular interfaces that meet the retained brackets.
Installed support span
The separation of the shaft support locations in the actual machine, not an alternative name for body length.
Complete assembly envelope
The outer extent of all relevant supplied parts, which may include projecting ends or a ringed working surface.

Steel roller bearing ends belong in the assembly drawing

GRAM’s steel assemblies show bearing ends and projecting shafts beside their cylindrical bodies. The custom order should identify the required end arrangement with the body. A dimensioned tube does not tell the manufacturer all the interfaces needed to install and support the complete roller.

The bracket locates the shaft, not a loose tube on a bench

Show the retained support surfaces and the required shaft interfaces. The designer should determine which dimensions control placement in those supports. Avoid a drawing that gives a complete outer length while leaving the shaft ends undefined; a component can satisfy that outer envelope yet fail to sit correctly in the retained brackets.

The same principle applies when the two ends differ. Identify each end rather than assume a symmetrical assembly. A site photograph can suggest that one end has a different projection, but it does not define the geometry or its acceptance tolerance. The approved drawing must answer that question.

If the supplier proposes an end construction different from the one requested, have the responsible designer review the change. An attractive body price should not obscure the fact that the alternative shifts a locating surface or changes the way the shaft is retained. The purchasing line should reference the accepted complete assembly.

Bearing location must remain connected to the supported shaft

The bearing arrangement and shaft support geometry are connected parts of the roller. Identify the offered arrangement and the applicable assembly information instead of selecting a bearing name separately and assume it completes the drawing. A bearing description cannot establish the installed load path on its own.

This article does not prescribe bearing fits or shaft tolerances. Those require the actual components, intended duty and responsible design acceptance. The buyer’s useful action is to make sure the manufacturer and designer are discussing the same interfaces, not apply a universal tolerance copied from an unrelated roller.

A polymer substitution can preserve one dimension while changing another

GRAM’s polymer route describes a polymer body with precision bearings, non-contact rubber sealing and metal end caps. That arrangement should be evaluated as a complete component. Matching a steel roller’s body length does not prove that every end surface and supported position remains identical.

Polymer roller bodies and end assemblies whose locating dimensions need a defined custom drawing
The end construction must be included when comparing a polymer assembly with a steel reference.

Preserve the required interface, not an assumed internal construction

An equipment builder may want a polymer alternative while retaining its existing frame. Give the supplier the machine interfaces that must remain compatible and let the proposed complete assembly be reviewed against them. Do not force an undocumented internal arrangement from the old steel component onto a different construction merely because its exterior looks similar.

Conversely, a material substitution should not be permission to alter the installed support position without disclosure. The drawing should make the retained interfaces visible so a reviewer can identify which changes affect fit and which concern the construction inside the assembly. Keep both kinds of change explicit in the proposal.

The nylon roller route is another product family to review where appropriate. Its name does not establish a particular manufactured dimensional tolerance or make it identical to every polymer roller. The manufacturer should identify the proposed material and complete geometry for this order.

Rubber-ring impact rollers need a working-surface dimension

GRAM’s impact assemblies have a rubber-ring working surface. The outside of those rings, rather than only the underlying body, meets the belt. A custom impact-roller drawing should therefore identify the complete contact profile with its mounting interfaces.

Rubber-ring impact roller assemblies showing why working diameter differs from the core body description
A custom impact assembly requires the ringed working profile as well as shaft and body dimensions.

The ringed diameter belongs beside the supported belt line

If the designer requires a particular belt support geometry, the drawing needs the accepted outside profile and the shaft position that establishes it. A matching tube diameter does not ensure a matching ringed diameter. Equally, a matching ringed diameter does not define the shaft interfaces that place it correctly in the station.

Specify the intended ring arrangement through the approved construction information. A photograph is not enough to establish spacing or an acceptable compound. The order should distinguish the required geometry from the performance evidence needed for the intended impact duty; neither can be inferred from the other.

Custom roller acceptance should use the drawing’s own measurement references

Decide which dimensions the receiving team must verify against the accepted drawing. Name the reference surfaces and the condition in which each measurement is meaningful. A measurement made across different endpoints cannot demonstrate conformity to a drawing dimension merely because it gives a familiar number.

Define the measurement before choosing the tolerance

The responsible designer should determine the required tolerance and the applicable method. The buyer should first make the dimension itself understandable: which feature, which reference and which assembly condition. Debating a tight numerical tolerance for an ambiguously named overall length does not improve the drawing.

For relevant custom assemblies, the parties may also need an agreed way to assess the working surface or rotation. Keep those criteria tied to the intended roller and duty. Do not make an unsupported runout claim or universal balance requirement just to make the supplier evaluation appear more technical.

Professional suppliers make complete component drawings available; Rulmeca’s drawing portal illustrates that approach, while its technical resource centre separates component scopes. These are industry references. Their dimensions, models and acceptance limits must not be transferred to a GRAM custom order.

Do not replace a functional locating reference with a convenient body edge

A body edge may be easy to measure on a bench without being the surface that locates the roller in service. Show the functional reference selected by the designer and keep dimensions related to it clearly distinguishable. The drawing should explain which features establish position, not leave the inspector to choose whichever edge is most convenient.

Where an end cap or ring extends beyond the underlying body, identify that extension separately. A complete envelope measurement and a body measurement can both be useful, but they answer different questions. Labeling both as roller length invites a disagreement that tighter tolerances cannot resolve.

For an assembly with several dimensioned features between its locating surfaces, ask the designer to identify how conformity to the installed requirement will be judged. The manufacturer should not have to infer which independently specified dimension takes precedence if they appear inconsistent. Resolve the drawing question before production instead of ask the receiving team to decide which conflicting dimension it should waive.

The approved roller revision should be the one that reaches production

Once the required dimensions are clear, identify the approved drawing revision in the final order. If a supplier proposes a different end construction during price negotiation, revise the accepted information before release. Otherwise the workshop can manufacture one interpretation while the receiving team checks another.

Ask the manufacturer to identify unresolved drawing questions before cutting or assembly. This is especially useful when the drawing comes from an old component and not every original detail is available. Leaving an uncertain dimension open for approval is preferable to presenting a guessed feature as a confirmed requirement.

Handling protection should preserve the accepted shaft ends and working surfaces, with the drawing identity retained on the supplied units or agreed package. A custom shaft projection damaged in transit can undermine the interface the order was designed to preserve. Packaging protection is therefore related to the particular assembly, rather than an unrelated request for “good export packing.”

The existing custom roller overview describes the broader product route. For this order, the decisive step is narrower: approve a complete drawing whose dimensions locate the roller in the actual machine. Compare price after the endpoints, interfaces and acceptance references mean the same thing to the designer, manufacturer and receiving team.

High Quality HR Rubber Belt for Heat Resistance

The normal cooler discharge temperature is not the whole specification for a clinker belt. A cement plant assessing a clinker conveyor belt supplier should also define the hottest credible upset and what happens when hot material remains on a stopped belt. GRAM’s HR rubber belt range explicitly lists clinker, sinter and coke applications. Start with that heat-resistant route, then obtain the applicable information for the offered complete belt rather than choosing a numerical limit from a general description.

The first engineering task is to establish the exposure at the belt, including the material condition, contact duration and operating interruptions. The first purchasing task is to connect that exposure with a declared cover and reinforcement construction. Those two records should agree before the buyer approves a replacement.

A clinker conveyor belt supplier needs the credible temperature upset

A normal operating measurement describes one state of the process. Identify whether a cooler problem, changed material flow or another credible event can expose the belt differently. The responsible plant team should define that condition using its operating information. The supplier should not have to infer the maximum relevant exposure from the material name alone.

Cooler discharge measurements need a stated location and method

Record where and how the material temperature is assessed. A measurement at one discharge location may not describe every particle reaching the belt or the temperature at the contact surface. Include the known variation and any uncertainty. This provides a clear basis for the supplier enquiry without claiming a precision the plant has not established.

A buyer who has only a normal process temperature should identify the missing upset information rather than add an arbitrary margin. Ask the responsible process engineer to establish the credible condition. The offered belt can then be assessed against a real exposure description instead of a convenient number selected for purchasing.

Stopped clinker on the belt creates a different contact period

A maintenance team may pause a loaded hot-material conveyor while the surrounding process remains warm. The belt then sees a different contact duration from normal movement. Include that state in the operating assessment. A general heat-resistant description does not establish that any hot load can remain stationary indefinitely.

The plant’s approved operating and shutdown procedure should address its hot-material condition. The article does not prescribe a universal stopping or cooling action. Give the supplier the resulting exposure requirements and obtain applicable offered-product information, while the site retains responsibility for its process controls and safe operating method.

Clinker conveyor belt selection should distinguish material and belt exposure

The material temperature is an input, but the actual belt exposure also depends on contact and operating conditions. Describe the particle condition, loading pattern and route. The supplier and plant engineer need that context to assess the offered cover and complete construction. Do not turn one temperature measurement into an unrestricted service claim.

Fine hot material and coarse clinker can contact the cover differently

Identify whether the conveyor normally carries coarse clinker, a finer mixture or a changed product state. The contact between the material and belt is part of the exposure description. If the mixture changes during an upset, keep that condition separate from the ordinary coarse-material description.

Professional discussion in Dunlop’s heat-resistant belt article explains why material characteristics and contact matter in thermal selection. Its product comparisons and performance claims are not GRAM data. Use the general reasoning to prepare the enquiry, then obtain the offered belt’s own applicable information.

Cover resistance and carcass suitability need separate confirmation

The cover meets the clinker, while the reinforcement provides the belt’s mechanical construction. GRAM’s rubber belt range discusses these product routes, but the specific offered cover and carcass must still be identified. A cover description alone does not define the entire belt’s thermal and mechanical suitability.

The temperature-basis guide is relevant when a buyer checks which component and exposure a temperature statement concerns. For clinker, add the credible upset and stopped-load states to that assessment. The approval should identify the complete belt offered for them.

Compare the GRAM reinforcement routes without treating them as heat grades

GRAM describes EP reinforcement with polyester warp and nylon weft, and NN reinforcement with nylon in both directions. These are fabric construction distinctions. Their names do not establish a numerical heat-service limit.

Provide the retained pulley, tension and take-up requirements with the thermal exposure description. The supplier should propose a complete construction that the responsible designer can review. An EP or NN label is not enough to establish the delivered width, reinforcement specification, cover arrangement or joining requirements.

GRAM’s steel-cord route uses longitudinal steel reinforcement. It may be relevant where the approved mechanical duty calls for it. The rubber cover and other construction details still require their own assessment; steel reinforcement does not establish unlimited heat resistance.

Longitudinal steel reinforcement cords illustrating a construction choice separate from a clinker belt heat-resistant cover
Select reinforcement through the mechanical duty, then confirm the complete belt’s applicable thermal information.

Ask the clinker supplier what the offered heat statement actually covers

Request a product-specific description of the applicable temperature and exposure conditions. It should identify whether the statement concerns material, cover or complete-belt service and any relevant contact-duration limitations. Avoid choosing a rating from an unrelated paragraph or another manufacturer’s product.

A thermal document should identify the offered cover and construction

If the project requires a test or acceptance criterion, state it in the enquiry and ask for the evidence corresponding to the proposed belt. The document should remain linked to the actual offered construction. A result from a different cover or reinforcement combination cannot be silently treated as proof for the final supply.

Do not add an exact heat class or test value where the site’s product information does not establish one. That uncertainty should be resolved through the offered belt documentation. A cautious, complete enquiry is more useful to purchasing than an unsupported numerical promise.

Short thermal upsets should not disappear inside a continuous-service description

A continuous operating statement and an intermittent exposure statement can refer to different conditions. Ask which one applies to the defined clinker route and what the offered product information actually permits. The supplier should make the boundary clear, while the plant establishes the process condition that must remain within it.

If the process engineer cannot yet define the credible upset, keep that as an open approval item. Do not convert the uncertainty into a claim that the belt will tolerate whatever the cooler produces. The procurement schedule should reflect the need to resolve that requirement before the product is accepted.

Reassess clinker belt changes before final delivery

A clinker process change should trigger a fresh review of the thermal basis

A plant can change cooler operation or the conveyed mixture without changing the belt width. Review whether the existing thermal description still applies. The supplier should receive the updated normal and upset conditions, while the responsible process team identifies the operating boundary. A repeat order based only on the original belt size can omit the exposure that now matters.

Changes in loading coverage or contact duration should be described as well. The new enquiry should identify what actually happens at the belt rather than simply report a process temperature from elsewhere. Where the plant does not yet have that information, mark the uncertainty for resolution instead of assigning a generic heat margin.

If the supplier proposes a different cover or reinforcement arrangement, ask which applicable thermal information belongs to the alternative. A rating associated with the original product should not be retained automatically after its construction changes. The offered complete belt and its stated exposure boundary need to remain identifiable together.

For a maintenance buyer keeping spare hot-duty belt sections, record the approved clinker exposure with the stock item. A heat-resistant description can be too broad to distinguish sections selected for different conveyors. Before a spare is reassigned, compare both the mechanical requirement and the thermal basis with the new intended location.

The plant can also define what evidence should be recorded after a credible thermal upset. Use the approved inspection and operating procedures to assess belt condition. Those observations can improve the next supplier enquiry, but they should not be turned into an unsupported service-life claim or a universal statement about every belt in the HR range.

The supplied length and form should identify whether the belt will arrive as an open length, completed loop or agreed sections. Establish the joining responsibility and applicable construction information before approving the final delivery requirement. A heat-resistant product name does not define the splice or the installed length.

Wrapped conveyor belt rolls illustrating the need to preserve the actual heat-duty construction and joining identification
Package identification should remain connected to the approved cover, reinforcement and supply form.

Ask for a packing arrangement suited to the actual belt and handling route. Protect the supplied identification and follow the offered storage instructions before installation. Do not leave the belt beside an unnecessary heat source simply because its intended duty involves clinker.

At receiving, match the construction and supplied documents with the approved thermal basis. Inspect accessible surfaces and edges for visible damage through the agreed handling procedure. Resolve an undocumented cover or construction change before the belt is installed at the hot-material route.

Approve the clinker replacement against the hottest credible state, not only the normal cooler reading. Keep the exposure, offered complete construction and joining arrangement connected. When one of those is still undefined, obtain the missing engineering or product information before releasing the belt for that route.

GRAM rubber-ring conveyor impact rollers

The damaged belt is beneath the chute, but the replacement request lists only roller diameter. A quarry buyer or mine engineer working with a conveyor impact rollers supplier should first establish where the material actually lands and how the belt is supported through that area. GRAM’s conveyor impact rollers are a relevant starting point for a rotating, rubber-ring support. Its impact load-zone belt support offers a separate route when an impact bed, saddle or different support arrangement needs to be considered.

The purchase is not settled by the presence of rubber on a roller. The support must suit the material landing footprint, the belt geometry and the forces transferred into the conveyor structure. Otherwise a stronger replacement may be fitted beneath the same poorly supported area and leave the original cause of damage unresolved.

Give the Conveyor Impact Rollers Supplier the Actual Landing Footprint

The material stream occupies an area, not a single point on a drawing. Describe its position along the conveyor and across the belt, together with the feed trajectory, largest relevant lumps and operating variations. Those details allow the engineer to assess whether the existing impact station arrangement supports the belt where the load is applied.

A quarry transfer may show repeated cover cuts between adjacent roller stations while the rollers themselves remain serviceable. Replacing only the rings can leave the same unsupported span beneath the incoming material. The investigation should compare the damage location with the station positions, not assume that every cut is evidence of insufficient ring hardness.

Large Lumps and Fine Material Load the Impact Bank Differently

A stream of fine material and occasional large lumps should not be reduced to one average feed description. An irregular lump can impose a localized loading event, while fine material may accumulate around the support and sealing area. Give the engineer the relevant material characteristics so both the structural and contamination questions can be assessed.

Material drop and direction matter as well as weight. Rulmeca’s impact roller technical material explains why impact support is assessed for the falling load and the base roller. Its models and dimensions are not GRAM specifications; the principle is to evaluate the assembly against the loading event rather than the static carried load alone.

At a mine transfer modified for a different feed route, the original impact bank may no longer sit under the new material trajectory. Mark the revised landing area before assuming that the old station quantities remain appropriate. If the load has moved, a like-for-like roller order can reproduce a support arrangement that no longer matches the chute.

Include the conditions under which the landing footprint was observed. A partly loaded feeder may produce a different stream from the intended production duty, and a brief observation can miss intermittent oversize material. The engineer needs the relevant operating range and the method used to describe it. That does not require inventing an impact-force value; it requires preserving the operating context for the support assessment.

Rubber-ring Impact Roller Geometry Determines the Supported Belt Line

The rubber rings form the working surface of the impact roller. GRAM’s product images show the ringed body, roller ends and projecting shafts. The complete outside diameter over the rings matters to the belt line; the underlying tube diameter is only part of the construction.

The Ringed Working Diameter Must Match the Intended Impact Station

Confirm the proposed working diameter, ring arrangement and roller face length for the intended position. A change in the ringed diameter can alter the belt support height even if the base roller and shaft appear similar. The engineer should review that geometry with the surrounding carrying run before the new component is treated as a direct replacement.

Worn rings are a poor dimensional reference for a new assembly. If the old working surface has lost material unevenly, its measured outside profile may describe wear rather than the intended belt line. Use the original construction information where available, or establish the replacement geometry through an approved assessment.

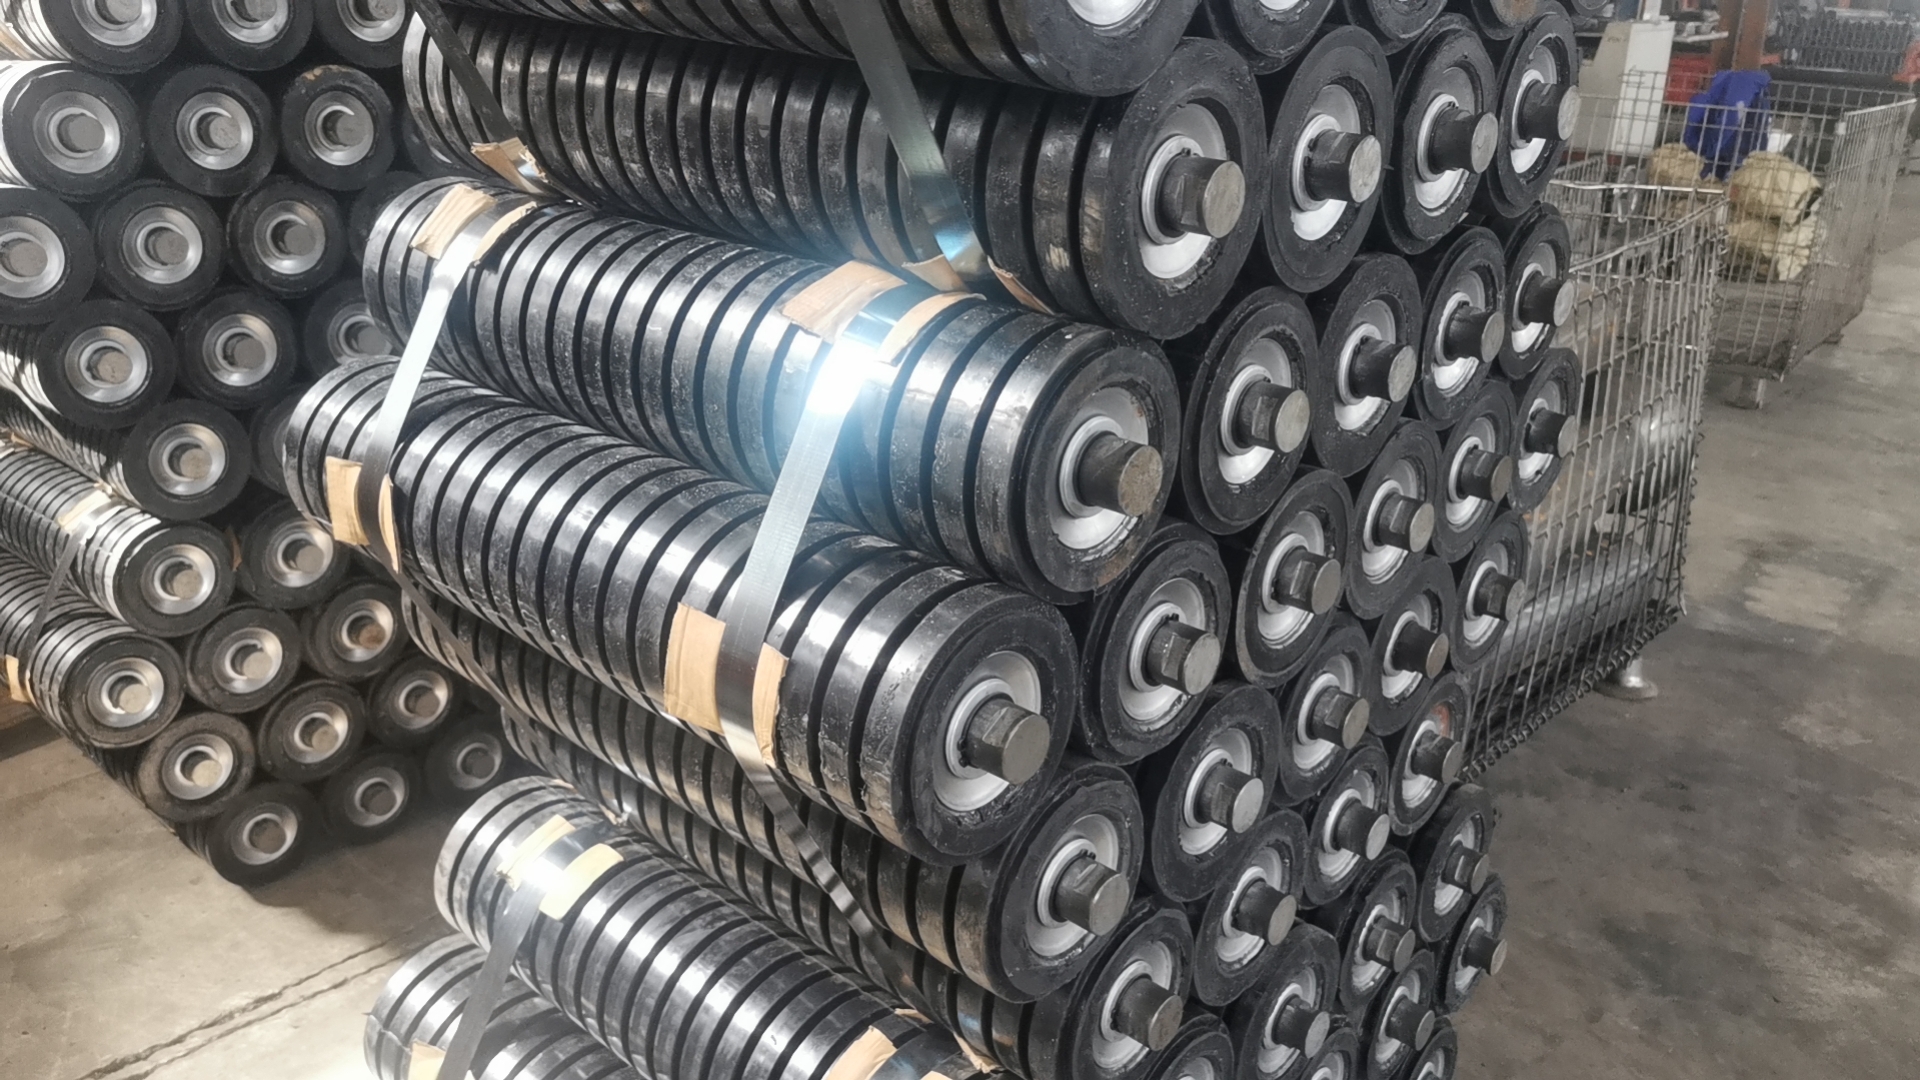
Stacks of black rubber-ring impact rollers with ring profiles and shaft ends visible
Specify the ringed working surface as part of the complete roller geometry. A base tube measurement alone cannot establish the supported belt height.

Centre and Wing Impact Rollers Share a Troughing Decision

Where a station supports a troughed belt, the centre and wing positions work together. Their heights, angles and interfaces should preserve the intended belt shape through the loading zone. Do not approve each roller in isolation and assume that the assembled station will reproduce the required support profile.

A replacement wing roller with the correct nominal length can still change the supported shape if its working diameter or mounting arrangement differs. Keep the station-level drawing associated with the individual components. The order should identify which positions are being replaced and which retained frame parts establish the assembly geometry.

When an Impact Bed Addresses a Different Loading-zone Problem

GRAM’s loading-zone support range includes impact beds, saddles and idlers. A rotating roller bank and an impact-bed arrangement provide different support geometries. The choice should follow the observed loading problem and the conveyor design, not a claim that either option is always superior.

Observed loading problem Question for rotating impact rollers Question for impact-bed support
Damage appears between support stations Does the station arrangement support the actual landing footprint? Would the proposed bed provide the required support through that area?
The belt moves beneath the chute sealing area Is deflection compatible with the intended sealing arrangement? How will the proposed support maintain the belt path and clearance?
Material accumulates around support components Can the rollers rotate freely and remain accessible? How will deposits, access and sliding-contact conditions be managed?

Continuous Belt Support Introduces Its Own Operating Questions

A bed supporting the loading region needs an appropriate structure, contact arrangement and installation clearance. The buyer should obtain the proposed geometry and the design basis for the loading conditions. A more continuous support surface does not remove the need to assess the conveyor structure or the belt’s movement through the transfer.

The Metso conveyor solutions handbook illustrates that impact-cradle selection depends on an application-specific loading assessment. Its calculation assumptions and classes belong to Metso. A GRAM bed proposal needs its own agreed design information; the handbook should not be used to assign a borrowed capacity to an unspecified assembly.

If an existing conveyor has limited access beneath the chute, confirm how either support arrangement can be installed and maintained. An impact bed that addresses support continuity may still require a different access envelope from removable rollers. The engineering comparison should include the physical installation, not just the purchase price of the visible working elements.

The retained structure needs a defined assessment when the support route changes. A bed may connect differently from an existing roller station and transfer its loads through different mounting points. Confirm the proposed attachment and the structure that will carry it before accepting a retrofit. A component that fits beneath the belt is not thereby confirmed as suitable for the existing frame.

Carrying Rollers Should Not Be Ordered as Unspecified Impact Replacements

GRAM’s steel carrying rollers provide a different family to examine for the ordinary carrying run. A robust metal shell does not automatically establish suitability beneath the material drop. If the component is intended for impact duty, the proposed construction and rating must address that duty explicitly.

The transition out of the impact bank also matters. The belt should move from the loading support into the carrying arrangement without an unintended step or abrupt change in geometry. Review the adjacent stations when the impact roller working diameter or support arrangement changes. The loading-zone order should not create a new problem immediately beyond its boundary.

Check the belt line on both sides of the revised support, including the approach beneath the chute. If an adjacent station is retained, its original working geometry remains part of the comparison. A new ring diameter should not be approved as a single-component improvement without showing how those neighboring supports relate to it.

Mining Belt Construction Cannot Replace a Loading Support Assessment

GRAM’s mining conveyor belt range is relevant when the belt itself needs replacement. Belt reinforcement and covers still have their own requirements. Buying a belt described as heavy duty does not prove that a poorly supported material landing area is acceptable.

For a transfer with both cover damage and damaged impact supports, coordinate the two decisions. Identify what the belt construction must withstand and what the support must do beneath it. If one component is changed without reviewing the other, the buyer can spend on a stronger belt while retaining the same concentrated loading geometry.

Conversely, changing the impact support is not proof that an already damaged belt can remain in service. The responsible engineer should assess the belt’s condition and the repair or replacement requirement. The support supplier’s role and the belt acceptance decision need clear boundaries so neither is inferred from the other.

Off-centre Feeding and Mistracking Need a Separate Correction

An impact roller supports the incoming load; it does not automatically centralize an uneven material stream. If feeding is persistently off centre, review the chute and loading arrangement. Metso’s belt-life maintenance discussion identifies off-centre feeding and alignment as issues that affect belt travel.

GRAM offers self-aligning idlers as a separate tracking-related family. They should be considered against an identified tracking requirement, not added automatically to every impact order. A support device cannot be expected to remove the underlying cause of a badly positioned material stream.

Distinguish local deflection beneath the incoming load from persistent mistracking beyond the loading zone. The observations may occur together, but they lead to different questions. The impact bank needs to support the belt; the feeding and alignment assessment needs to establish why the belt is moving sideways.

Release Impact Roller Dimensions with the Loading-zone Arrangement

Before dispatch, connect the approved individual roller drawing to its station and conveyor position. The receiving team should be able to identify the working ring diameter, face length, shaft arrangement and assigned location. If more than one impact station construction is supplied, keep the references distinct through transport and receipt.

Ask for protection that suits the ringed surfaces and exposed shaft ends. Rings should arrive in the condition required by the agreed assembly, and the package labels should preserve the position references. A bundled product photograph illustrates possible handling, but the actual protection and delivery scope must be agreed for the ordered rollers.

Rubber-ring conveyor impact rollers bundled together with exposed mounting shaft ends
Protect the working rings and the mounting interfaces together. Position identification should remain with the rollers until installation.

For the product-family background, GRAM’s rubber-ring impact roller explanation provides additional context. Use it to identify the construction, then return to the actual landing-zone geometry and approved support arrangement.

Site measurement, removal and installation must follow the mine or plant’s approved isolation procedures. The OSHA hazardous-energy guidance explains the maintenance principle. A material trajectory should be observed from an approved safe location; it is never a reason to reach beneath a moving belt.

When the supplier’s proposal shows exactly how the belt will be supported under the material stream, the impact purchase has a clear basis. If damage still falls between the proposed support positions or the revised chute sends material beyond them, revisit the arrangement before ordering stronger rings. The useful replacement supports the real transfer, rather than repeating the dimensions of a loading zone that has already changed.

Steel roller assemblies with cylindrical bodies, bearing ends and projecting shafts

Maintenance asks for a bearing, procurement asks for a roller, and the customer expects a complete replacement that fits the retained supports. Those requests concern different supply units. Before pricing the work, a replacement conveyor rollers supplier should establish what is being purchased and which parts, if any, will remain. Start with GRAM’s conveyor roller range and identify the actual complete assembly or component proposal rather than use “repair” as a substitute for supply scope.

For contractors and distributors, this is a purchasing boundary, not a dismantling instruction. A complete roller offer does not demonstrate that individual bearings are supplied separately. A component-only request does not demonstrate that the retained assembly is suitable for rebuilding. Those questions need their own actual proposal and responsible assessment.

The replacement conveyor rollers supplier needs one defined supply unit

State whether the customer wants a complete roller, an identified separate component or a connected group. Preserve that unit in the request, quotation and accepted order. A price can only be compared meaningfully when the buyer knows which unit it covers and what retained equipment the proposal assumes.

Resolve the workshop-to-order mismatch: name the item the supplier is expected to deliver, then identify what remains outside that supply. Do not convert a maintenance symptom into an assumed product or service.

A distributor should pass the clarified unit back to the final customer before accepting a different scope. If the customer requests a complete replacement but the quote covers a body alone, the offer is incomplete for that request. Do not fill the gap with assumed bearings, ends or assembly work.

A complete steel roller includes more than the visible tube

GRAM steel rollers use a cylindrical body rotating around a central axle, with bearings toward the ends and projecting shaft interfaces. Those parts describe the complete assembly relationship. A tube photograph does not establish that a tube-only offer includes them all.

If a complete roller is the required unit, keep the body and end construction identifiable together. The retained support relationship still needs definition. A quotation for an outside cylinder should not be presented as a ready replacement merely because its visible diameter resembles the removed assembly.

A bearing request should not imply an accepted roller rebuild

If maintenance requests an internal component, procurement needs to establish whether the supplier actually offers that component and under what identified scope. GRAM’s complete roller descriptions do not prove a separate bearing inventory or rebuilding service. The customer should receive an explicit answer rather than an inferred one.

The decision to retain or rebuild an existing assembly belongs to the responsible maintenance assessment. A component’s availability cannot establish that decision. Keep any intended retained parts and the party responsible for the work distinguishable from the supplier’s delivery obligation.

Compare roller replacement scopes before comparing prices

Separate the actual included parts and any stated exclusions. A low figure for one component should not be compared directly with a complete assembly price. Equally, a complete roller price should not be described as a repair service if it covers supply only.

Requested unit Boundary that must be clear
Complete roller The identified body, ends and assembly being supplied
Separate component The actual offered part and the retained assembly it is intended for
Connected group The supplied group and the retained supporting equipment

Consider a contractor gathering three proposals after a failed roller is removed. One supplier quotes a complete unit, another quotes only a body and the third offers a different assembly pending equipment review. The buyer has three different proposals, not three equivalent replacement prices. Clarify them against the same intended task before selecting one.

A primary roller range description distinguishes body construction, bearing ends and application-dependent configurations. That general assembly distinction is useful here. It does not establish GRAM repair services, component stocks or compatibility with another manufacturer’s roller.

Polymer replacements need a complete changed-construction proposal

GRAM polymer rollers are described with a machined polymer tube or solid bar, sealed precision bearings, non-contact rubber seals and metal end caps. If the buyer considers a polymer alternative, identify that actual complete unit rather than order an unspecified replacement body.

GRAM polymer rollers showing why a material alternative needs an identified complete supplied assembly
A changed body material does not define the entire replacement scope.

Retained mounting does not mean every internal component is retained

The new unit may be intended for the existing support interfaces while changing its body and end construction. State that relationship explicitly. The buyer should know which equipment remains on the conveyor and which parts belong to the supplied replacement assembly.

A material alternative should remain a separate proposal until the project accepts its fit and duty. A supplier’s generic polymer description should not be converted into approval for the removed steel unit’s location. Keep the actual offered reference and acceptance basis attached to the order.

For a distributor, do not describe a whole-roller substitution as a body repair. The customer needs to understand the actual item arriving. A changed supplied unit can have different commercial and technical boundaries from the component request that initiated the enquiry.

Rubber-ring replacements distinguish surface parts from complete impact rollers

GRAM’s rubber-ring impact rollers have a ringed belt-contacting working surface. A request concerning worn rings can refer either to separate surface components or a complete impact assembly. The supplier’s actual offer should establish which purchase is available and intended.

Do not assume separate-ring supply or an accepted ring-replacement service from a complete roller photograph. If the proposed unit is a complete impact roller, define the working surface, underlying assembly and mounting ends together. If a component is offered separately, preserve that narrower scope.

A contractor should also retain the original duty distinction. A plain roller cannot be described as an equivalent complete replacement solely because its shaft ends fit the same brackets. The accepted proposal needs the actual working construction selected for that location.

Where the removed rings no longer show the original profile clearly, identify the uncertainty rather than invent a nominal construction. The supplier can propose an identifiable replacement for the retained arrangement. The project still needs to accept that proposal rather than approve a guessed reconstruction.

Garland replacement units can be rollers or connected groups

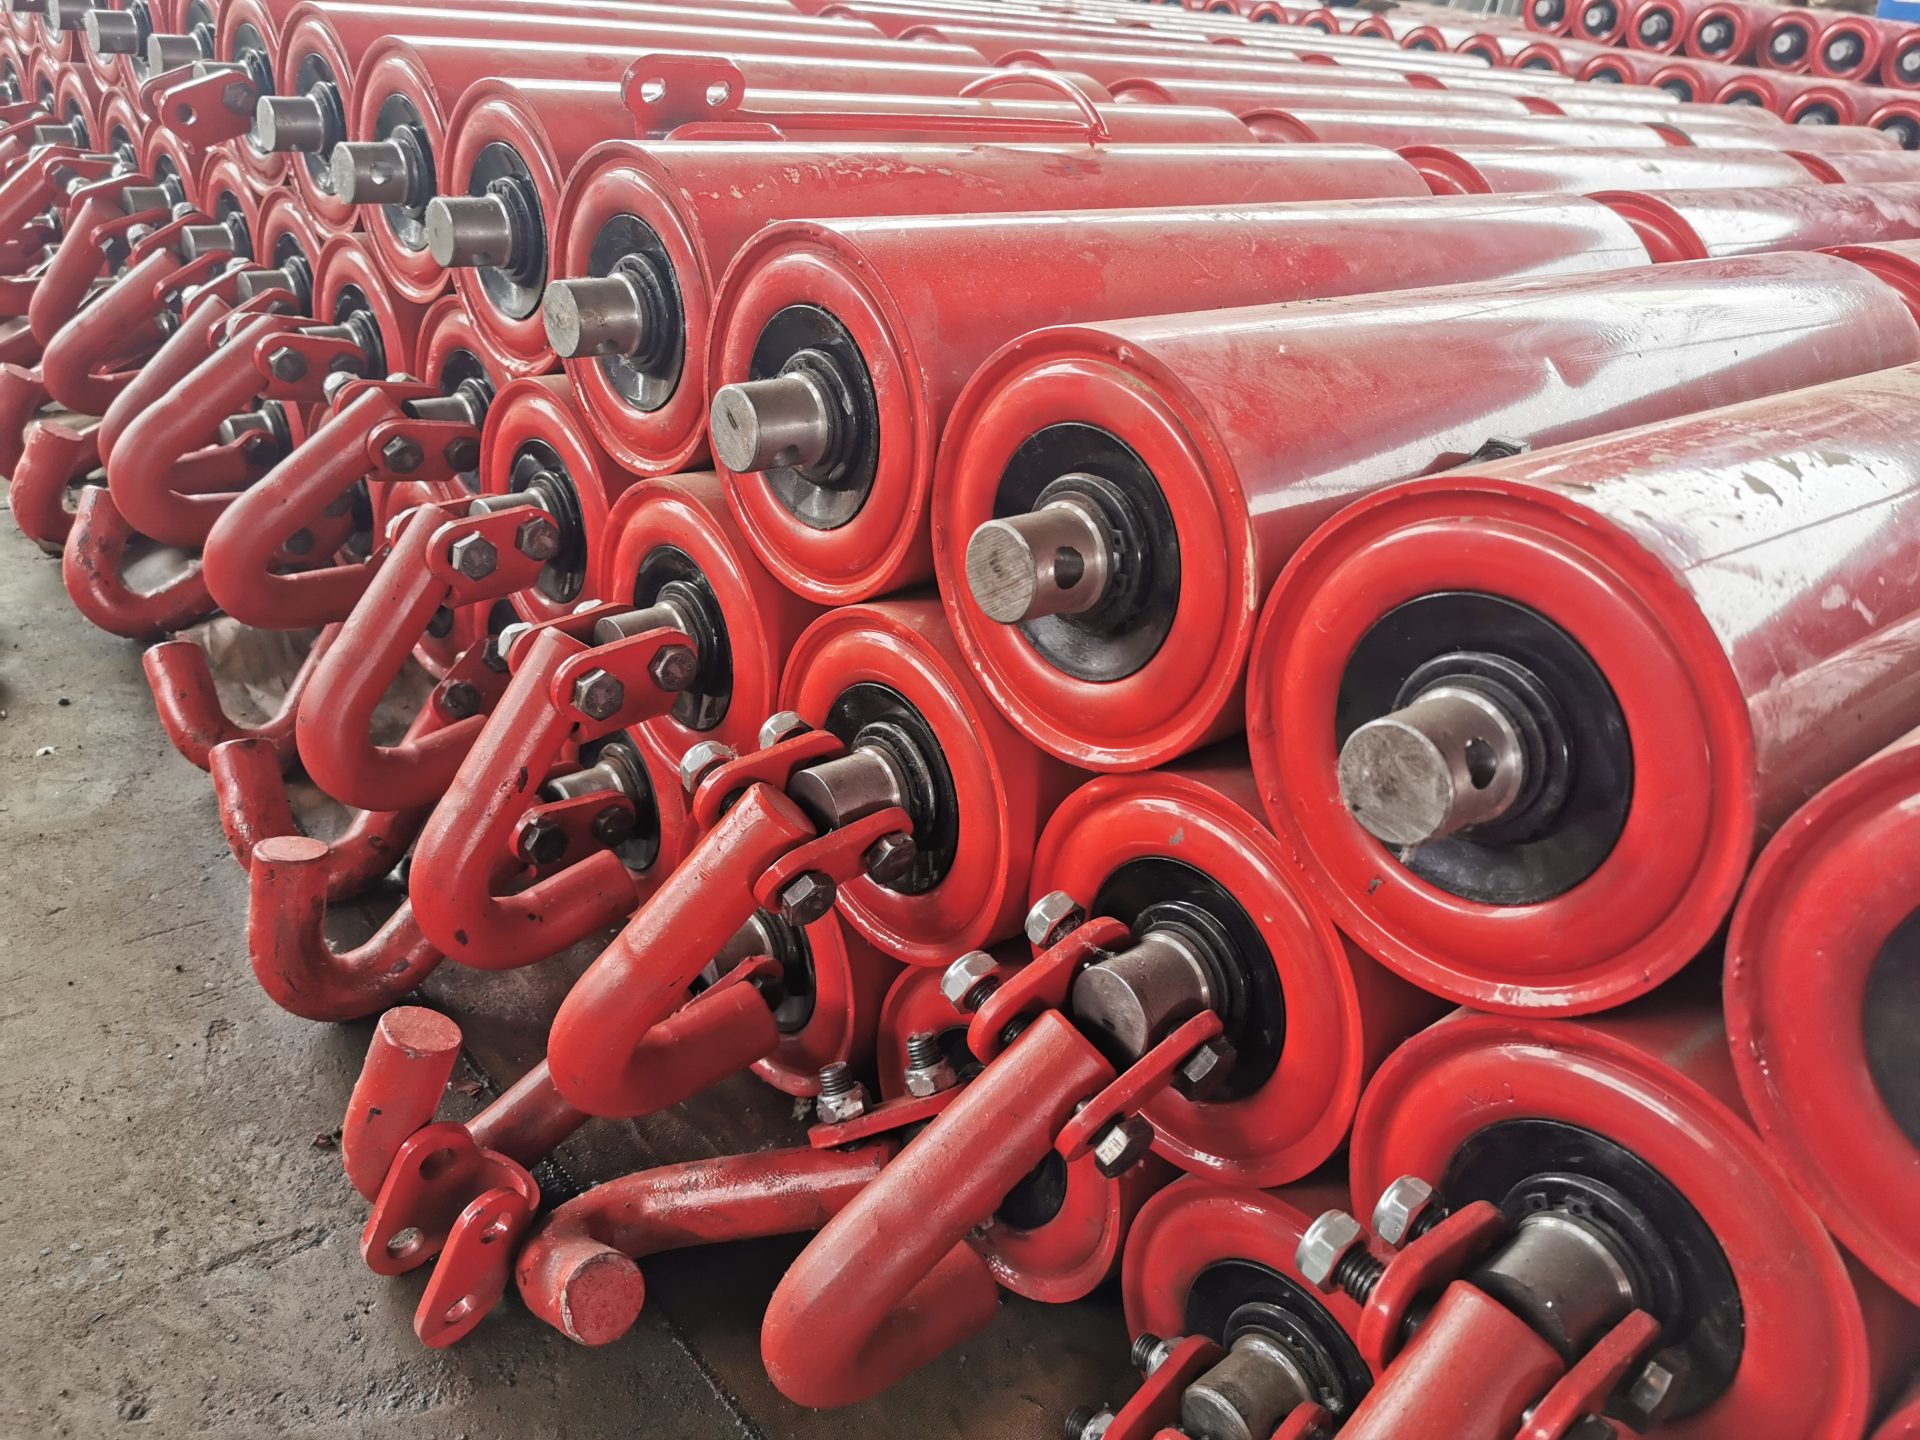
GRAM carrying garlands use connected rollers suspended as a group. The order unit should distinguish an individual component from the linked assembly. A quantity of loose rollers does not automatically constitute complete accepted groups.

GRAM linked garland assembly whose complete group scope differs from individual replacement rollers
The commercial unit should follow the component or group the customer expects to receive.

A distributor may receive a request for several “garlands” and quote individual roller prices. Resolve that mismatch before accepting the order. Identify the connected assembly, any supplied connection parts and the retained support boundary. Do not assume unspecified hardware is included.

For partial replacement, identify which group remains and which supplied component enters it. A loose roller reference should connect to the intended retained arrangement. If that relationship cannot be established, leave the proposal conditional rather than promise interchangeability.

Keep the repair responsibility outside an unapproved supply assumption

A supplier can deliver a defined unit without being responsible for dismantling, rebuilding or installing the retained equipment. If the customer expects additional work, identify it separately and establish whether it is actually offered. The purchase should not contain an implicit service obligation that no party accepted.

The mixed-fleet spares discussion helps classify the product roles involved. Here the narrower decision is what replaces the selected item and what the supplier delivers. A role label does not settle the included assembly or work scope.

Keep component supply, complete-unit supply and any separately agreed service distinguishable in the final record. If the supply changes after an initial component request, update the customer-facing description. The final order should describe the current decision, not the maintenance shorthand that began the conversation.

Receive the unit that was actually accepted for replacement

Consider a workshop request that changes from separate bearings to a complete steel replacement after the retained body cannot be accepted for reuse. Update the supplier order to the complete-unit scope and preserve the accepted mounting reference. The original component request should not remain the dispatch description after the purchase decision changes. This does not diagnose the old body; it makes the actual revised supply obligation clear to the customer and receiving team.

Agree how delivered items will identify the accepted complete assemblies or separately offered components. Where similar items have different destinations, preserve their references and quantities. A receiving team should not have to reconstruct the purchase scope from loose parts and a generic roller invoice.

Ask for the actual proposed packing of the selected assemblies, especially where projecting ends or ringed working surfaces are relevant. Do not copy a complete-unit packing description onto a component-only delivery. The contents and their protection should follow the actual supplied unit.

Resolve the unit before pricing the repair: a complete roller, a specifically offered component or an identified connected group. Keep retained equipment and additional work outside the supply unless they are explicitly included. That gives maintenance, procurement and the receiving team the same replacement to evaluate.

Polymer conveyor roller assemblies with metal shaft ends

A quotation gives the weight of a polymer body, while the retained steel roller’s record gives the weight of the complete assembly. Comparing those figures can exaggerate the apparent difference. A polymer conveyor idlers supplier should identify what each weight includes before a contractor uses it in replacement planning. Begin with GRAM’s polymer roller route and the actual complete offered assembly, including its body, bearings, ends and shaft interfaces.

This is relevant to buyers considering a material alternative for restricted installation access or a mixed replacement order. The weight of a supplied complete roller can inform the project’s handling review. It does not, by itself, establish load capacity, low running resistance or a quantified improvement in conveyor performance.

A polymer conveyor idlers supplier should identify the weight unit

State whether a value concerns the body, complete roller, connected group or transport package. Those are different units. Keep the object attached to the figure in the quotation rather than retain a number after its original description has been removed.

Use the same comparison basis: complete offered roller against complete retained or alternative roller, with construction and dimensions identified. Keep body-only and packaged weights separately labelled where they are supplied.

A distributor should preserve that distinction when passing the comparison to the customer. A body-only figure should not be presented as the weight that the customer will receive and install. Ask for the actual assembly basis if the supplier’s information is incomplete.

Does the polymer value include bearings, end caps and shaft?

GRAM’s polymer description includes sealed precision bearings, non-contact rubber seals and metal end caps in addition to the polymer body. Those components belong to the complete assembly. A body-material description therefore cannot establish the complete supplied weight on its own.

Ask the supplier which parts are included in the stated figure and which actual roller reference it identifies. If the figure comes from a different size or construction, keep that limitation clear. It is not an accepted value for the proposed replacement merely because both items use polymer.

Is the quoted polymer body a tube or a solid-bar construction?

GRAM describes a machined polymer tube or solid bar as body routes. These are distinguishable constructions even where the outside material family is shared. Preserve the actual proposed form when comparing the complete roller, rather than assume that every polymer body has the same internal build.

The supplier’s offered dimensions and construction should establish the actual item. Do not calculate its weight from an assumed resin density or a guessed wall thickness. A general product description does not supply those missing values for the current proposal.

Compare the polymer alternative with the retained steel roller

GRAM steel rollers use a cylindrical body, bearings near its ends and projecting shaft interfaces. Compare complete assemblies for the intended position. An outside diameter or tube length alone does not show that all other construction features match.

GRAM steel roller assemblies to compare on a complete-unit basis with a proposed polymer replacement
Compare identified complete assemblies, rather than a steel roller against a polymer shell.

A contractor considering a different body material should keep the retained mounting relationship explicit. If that relationship is accepted while the body and ends change, record the actual complete alternative. A lighter stated weight cannot substitute for the required fit and duty information.

For a plant buying several sizes, retain a weight basis for each accepted item where it is relevant. Do not apply the figure for a shorter or differently built roller to every replacement. Aggregated shipping information and individual assembly information answer different questions.

Does a lighter quoted roller establish the same accepted duty?

No weight comparison alone establishes equivalent load acceptance. The proposed polymer unit needs its own applicable construction and duty information. Keep that review alongside the weight basis rather than use one number as a summary of every performance question.

A buyer can prefer a material route while still leaving an unresolved capacity or environmental condition open. The useful supplier proposal states the actual construction and the basis it addresses. Avoid treating a broad lightweight description as an unconditional substitution for the retained steel unit.

Primary polymer roller descriptions discuss weight and running characteristics as separate product considerations. That distinction provides general context. Their resins, operating limits, components and claimed performance are not GRAM specifications.

Weight and running resistance are different acceptance questions

A figure for total assembly weight does not identify the resistance of the assembled roller as it runs. If the project requires running-performance evidence, ask for applicable information concerning the offered construction and its conditions. Do not turn a body-material comparison into a quantified energy-saving claim.

The polymer body and end-construction discussion helps identify the assembly involved. Here the purchasing question is what a supplied weight comparison proves. It should remain a weight comparison unless separate evidence establishes another claimed property.

Can a silent roller description replace noise evidence?

GRAM’s silent roller route provides a separate entry for noise-related enquiries. The name does not establish a quantified noise result for every polymer replacement. A project with a specific acoustic requirement needs its own applicable evidence and accepted basis.

For an engineer comparing several routes, keep noise, running behaviour and complete weight as distinguishable requirements. A proposal can address one while leaving another unresolved. That gives the buyer a clearer decision than bundling all three into a generic low-weight, low-noise promise.

Nylon and ringed rollers should remain identifiable alternatives

The GRAM nylon roller route is relevant when nylon is the actual specified material. Keep the proposed construction and material declaration recognizable. A general polymer family name should not replace a customer’s explicit nylon requirement.

If nylon is offered as an alternative, identify the actual complete roller rather than copy a weight from another polymer body. The accepted proposal should retain its own material, end construction and mounting basis. No resin grade or numerical material property is established by the family name alone.

GRAM’s rubber-ring impact rollers have an additional working-surface construction. A weight comparison with a plain roller should identify that difference. Do not present their complete masses as evidence of interchangeable duty simply because the underlying bodies appear similar.

GRAM rubber-ring impact rollers whose additional working surface changes the complete assembly comparison
Different working constructions need separately identified complete-unit comparisons.

Use complete assembly information for the actual delivery and access review

Consider a buyer who receives a light polymer-shell value for a short sample and compares it with a long complete steel roller scheduled for replacement. That comparison changes both the unit and the construction dimensions. Ask for the actual complete offered reference before using the difference in a project assessment. The supplier’s material description cannot correct an inconsistent numerical comparison after its original labels have been removed.

A distributor may instead receive a total packaged weight that includes several complete polymer rollers. Keep that figure for the transport purpose it serves. Dividing it by the roller count without knowing the package contents does not establish the confirmed weight of each assembly. Ask for separately identified unit information where the customer’s equipment review needs it.

For an access-constrained replacement, the complete roller’s shape also remains relevant alongside its weight. Project planning should use the accepted assembly with its projecting ends, not a simplified cylinder representing only the body. A lower stated mass does not settle the physical access question. The responsible installation review needs the actual offered dimensions and unit, while the supplier’s commercial record should preserve that reference.

A contractor evaluating restricted access needs the actual offered assembly dimensions and relevant weight information. The project should assess its handling arrangements using that identified unit. This article does not prescribe lifting equipment, manual handling limits or an installation method.

For a distributor planning transport, keep the individual roller weight distinguishable from the proposed packed consignment. Ask the supplier to define the actual package and its contents. A body-only value cannot establish the transport weight of several complete rollers and their packing.

Consider a mixed dispatch containing short polymer rollers and longer steel units. The receiving team needs the accepted item references and actual quantities, not an average weight that obscures different assemblies. Preserve the supplied construction identities with any agreed package grouping.

If a quotation changes from tube to solid-bar construction after the weight comparison, review whether the figure still concerns the current offer. The same outside diameter does not establish an unchanged complete assembly. Keep the revised reference with the value used in the project’s assessment.

The same principle applies when end components change while the polymer body remains. Ask for information that identifies the revised complete roller. The buyer should not use an earlier value as though it were automatically confirmed for every later assembly revision.

Accept a polymer alternative whose complete construction, duty and comparison basis are identifiable. If lighter weight matters to the project, use an actual complete-unit value for that decision. Keep capacity, running behaviour and noise requirements separate so the chosen material is not asked to prove properties that its name alone cannot establish.

Black nylon conveyor belt roll positioned on industrial belt handling equipment

The belt carries a fertilizer product without an obvious problem, then its surface changes after the cleaning routine is revised. Purchasing only around the process material can miss the second exposure. A chemical resistant conveyor belt supplier needs the production and cleaning conditions described separately before proposing a construction. GRAM’s belt range includes chemical-resistant belting for processing, fertilizer and mining contexts. Start with that route and its rubber constructions, but obtain a proposal for the identified substances and conditions rather than accept a blanket acid-or-alkali claim.

A chemical resistant conveyor belt supplier should see the entire contact cycle

Follow what contacts the belt during production, after discharge, during cleaning and at restart. Those stages can involve different substances and contact times. Describe the actual sequence so the supplier’s proposal can be assessed against the complete duty the plant intends.

During production: identify the carried product and whether it reaches the belt as dry material, wet feed or a changing mixture.

Between batches: describe the residue remaining on the belt and whether moisture can change its contact with the rubber.

During cleaning: identify the cleaning product, its concentration in use and how long it remains in contact before removal.

For a processing plant using the same belt through several product campaigns, list each relevant exposure rather than supply only the largest-volume feed. A construction suitable for one documented condition is not automatically accepted for every batch or cleaning product. Keep unresolved conditions visible in the proposed duty statement.

Dry fertilizer and wet residue are separate exposure descriptions

A fertilizer conveyor may carry predominantly dry product but also experience damp feed, humid storage or wet cleaning. Tell the supplier which condition reaches the belt and when. Do not describe the chemical only by its commercial product name if its constituents or contact conditions are needed for assessment.

GRAM’s chemical-resistant range description makes this a relevant purchasing discussion, but it does not provide a universal concentration or temperature limit. The offered cover needs supporting information applicable to the actual exposure. A general reference to fertilizer duty cannot resolve a wet-residue question for an unspecified compound.

The cleaning agent belongs in the chemical-resistant belt proposal

The cleaning product can be different from the substance transported. Identify it separately, including the concentration used at the conveyor rather than only the concentration in the purchased container. Describe the temperature and duration of its actual contact with the belt.

Habasit’s material information explains that chemical assessment depends on the substance, concentration, temperature and exposure period. Its material tables concern other belt constructions and must not be transferred to GRAM rubber belting. The relevant lesson here is to define the conditions, not borrow a compatibility result.

A new detergent can change an otherwise unchanged conveyor duty

For a maintenance buyer replacing a belt after the site changes its detergent, provide both the previous and intended cleaning conditions. The carried product, frame and belt width may be unchanged while the chemical contact has changed. Reordering from the previous belt description alone can leave that difference outside the replacement assessment.

Have the proposed rubber construction assessed for the intended routine before release. The plant should agree how a cleaning change is reviewed in future, so a later substitution of cleaning product does not rely on an earlier acceptance for another substance. A broad chemical-resistant label is not a standing permission to change the exposure.

Rubber conveyor belt roll illustrating the construction to assess against process and cleaning contact
The offered rubber needs an identified exposure assessment. The appearance of a roll does not demonstrate chemical compatibility.

Fabric belt layers meet different parts of the cleaning cycle

GRAM’s fabric belt construction separates an upper cover, textile carcass and lower cover. That arrangement helps identify where each substance contacts the proposed belt. It also prevents the buyer from treating one exposed-face description as proof of compatibility for the entire construction.

Cleaning runoff can involve the lower cover and belt edges

The upper face may receive the cleaning product directly, while runoff or retained liquid can reach other regions. Describe those paths from the actual cleaning arrangement. A proposed upper-cover assessment does not automatically answer what happens at the lower face or an exposed edge.

Ask the supplier to identify the covers and edge arrangement in the offered construction, and explain which exposure its evidence addresses. Do not assume every fabric belt has the same edge protection. If the order changes an edge or cover detail, keep that change in the chemical-contact review rather than treating it as an unrelated manufacturing option.

EP yarn identity cannot establish cover compatibility

The EP route describes polyester longitudinal yarns and nylon transverse yarns. These are reinforcement details. They do not identify the rubber compound or establish its compatibility with the plant’s cleaning liquid.

For a retained EP conveyor, state whether the reinforcement designation and dimensions are to remain while the cover is reviewed. If another construction is proposed, obtain its actual details for the mechanical assessment as well. Keep the chemical decision and conveyor-fit decision connected without allowing one to stand in for the other.

NN fabric needs its own finished-belt assessment

GRAM’s NN construction uses nylon in both fabric directions. That is a different textile arrangement, not a chemical-resistance class. A proposal based on NN still needs an identified cover and an exposure statement for the complete offered belt.

A buyer should not change from EP to NN solely because the inquiry emphasizes chemicals. Ask what part of the construction the proposed change addresses. If the reason concerns the outer rubber, a change in yarn arrangement is not, by itself, an answer to the compound-compatibility question.

Wet residue before restart should remain in the belt assessment

Restart can introduce a condition different from either normal production or direct cleaning. Record whether residues remain, whether the belt has been rinsed and what material first reaches the cleaned surface. These are conditions to establish from the plant’s routine, not a universal cleaning instruction.

A contractor commissioning a replacement belt should obtain the intended production-and-cleaning description from the operator. The installation team can confirm mechanical fitting, but fitting successfully does not establish chemical acceptance. Make sure the supplied construction is the one reviewed for the operator’s stated exposure.

Steel reinforcement cords illustrating why reinforcement identity is distinct from rubber chemical resistance
Reinforcement descriptions answer structural questions. They cannot substitute for the rubber’s exposure assessment.

Where the site sees swelling, surface change or separation, preserve the affected region’s location and operating history for technical assessment. Do not assign a cause from appearance alone. A changed cleaning routine is relevant evidence, but other contacts and operating conditions may still require investigation.

Accept the chemical-resistant belt against stated conditions, not a broad promise

The final proposal should identify the finished construction and the process and cleaning conditions it addresses. Any limits or exclusions should be understandable to the operator. If the supplier’s evidence concerns a different concentration or temperature, obtain the required clarification before the belt is accepted for the intended duty.

Where a practical assessment is required, agree the proposed sample or construction and the exposure conditions with the responsible reviewer. A rubber sample can answer a defined material question but cannot automatically establish the behavior of a complete moving, tensioned belt. Keep those assessment scopes separate. Do not turn a favorable observation on one cover sample into a promise about the fabric carcass, edges or installed joint without the applicable supporting information.

Receiving records should preserve that construction identity. If multiple fabric belts arrive together, keep the chemical-duty order distinguishable from a general-purpose replacement of similar width. Agree identification and package protection for the supplied belt; do not infer a special packaging system or delivery commitment from the chemical-resistant description.

The existing fertilizer and processing overview provides the broader selection discussion. For a line whose cleaning routine is changing, carry the separate contact cycle into the actual offer first. Approve a defined construction for defined conditions, and reopen that assessment when the substance or routine changes.

FR Rubber Belt for Fire-Resistant Coal Mining Applications

Two conveyors carrying coal can require different purchase approvals when one is a surface transfer and the other serves a different mine or plant environment. A buyer evaluating a coal handling conveyor belt supplier should give the supplier the route’s mechanical requirements and its actual fire-related requirements together. GRAM’s mining belt range and FR rubber belt route are relevant starting points. Neither a coal application description nor an FR label establishes every installation’s approval.

For engineering buyers, power-station maintenance teams and distributors, the first task is to identify where the belt will operate and who sets the acceptance requirements. Then declare the reinforcement, cover, width, length and joining arrangement. Fire and static requirements should remain attached to the offered complete belt, rather than being treated as a separate marketing claim.

A coal handling conveyor belt supplier needs the route boundary

Describe the loading and discharge locations, the material stream and the operating environment. A general coal conveyor name can conceal differences in transfer arrangement, mechanical duty and required documents. Give the supplier the specification for the intended location rather than a combined list that assumes all coal equipment is interchangeable.

Surface coal transfers should have their own approval record

A power station may buy belts for unloading, storage and onward conveying within one procurement project. Keep the duty and requirements of each route identifiable. A common material stream does not establish that every belt needs the same reinforcement or cover construction, and it does not remove the need to confirm the applicable fire-related acceptance criteria.

If the project combines plant and mine equipment, separate the installation locations in the item list. The responsible site team should establish the relevant requirements for each. Do not extend a document supplied for one application to another merely because both belts carry coal.

Fire and static requirements need a named test and offered-belt identity

Ask the site to specify the required evidence, then ask the supplier for documentation tied to the actual offered product. The required test method, sample construction and applicability should be clear. A generic FR description is not a substitute for the documents needed by the project’s engineering or compliance review.

GRAM has an FR rubber belt product route, but this does not by itself establish a particular mine approval or certificate for every belt in the range. No underground approval, regional certification or antistatic performance should be assumed without the relevant current product evidence. Keep that distinction visible in the purchase documents.

Coal conveyor belt selection must also define the mechanical construction

Fire-related suitability does not replace the reinforcement decision. GRAM offers EP rubber belts, NN rubber belts and steel-cord belts. These routes need to be assessed against the approved conveyor duty and installation.

EP reinforcement identifies polyester warp and nylon weft

The EP construction described by GRAM uses polyester in the warp and nylon in the weft. That identifies the fabric route, not the complete belt specification. The offered reinforcement details and cover arrangement still need to be declared. Provide the retained conveyor requirements so the supplier can propose a construction against an actual mechanical basis.

If the existing belt has unclear markings, obtain the original equipment records or a suitable assessment of the sample. A black rubber surface cannot identify the internal fabric or establish the required strength. The purchase should end with an explicit offered construction that the responsible designer can review.

NN construction should be assessed with the retained conveyor arrangement

GRAM describes NN reinforcement with nylon in both warp and weft. If this route is proposed, have the complete belt checked against the conveyor’s tension, pulley, take-up and joining requirements. The material name alone cannot establish that it is interchangeable with an existing EP or steel-cord belt.

A distributor should keep the reinforcement description attached to any fire-related product documents. Otherwise, a repeat offer can appear to preserve the FR requirement while changing the mechanical construction. The buyer needs both aspects to remain identifiable on the actual supplied belt.

Steel-cord belts require their own splice and route assessment

Steel-cord reinforcement runs longitudinally in the GRAM product description and is associated with demanding conveying. It can be considered where the approved coal route calls for that mechanical construction. Its presence does not establish the belt’s fire or static performance.

Have the joining arrangement and complete conveyor requirements reviewed with the proposed steel-cord belt. A reinforcement change should not be selected simply because the route is long or the handled material is coal. The responsible designer needs the full duty, while the supplier identifies the offered belt and applicable evidence.

Longitudinal steel reinforcement cords illustrating a mechanical belt construction separate from fire-related cover requirements
Reinforcement selection and fire-related evidence are separate parts of the same coal belt approval.

Keep the coal belt document set linked to the offered item

Approval subject Information that must remain identifiable Common incomplete substitute
Installation location Actual conveyor route and site requirements A generic coal application label
Mechanical construction Declared reinforcement and complete belt arrangement EP, NN or steel cord without further specification
Fire-related requirement Required method and applicable offered-product evidence FR wording alone
Delivery and joining Supplied form, length and approved joining responsibility An unidentified stock roll

The fire and static document discussion is relevant when the buyer checks this identity. The document should concern the belt being supplied, not an unspecified product from the same general range. Record any construction changes between the submitted evidence and final offer.

External Continental mining belt literature distinguishes constructions and application-specific solutions. It provides professional context for a detailed coal enquiry. Its models, certificates and performance claims remain Continental’s and should not be transferred to GRAM.

Coal moisture and transfer changes belong in the cover enquiry

A mechanically suitable construction still needs an appropriate working cover. Describe whether the belt receives dry coal, wet fines or another credible condition. Include the loading arrangement and cleaning exposure. The supplier should identify the actual cover offered rather than assuming one coal description defines every material-contact requirement.

If the plant changes the material supply or drainage condition, update the enquiry before reordering. More carryback or a different deposit pattern may change the maintenance and cleaning discussion even when the conveyor dimensions remain the same. Keep those conditions separate from the fire-related documentation so neither requirement disappears inside the other.

Also identify any credible thermal upset through the site’s responsible assessment. An FR description should not become a numerical heat-service rating. Ask for the applicable information on the offered belt where temperature matters, and do not infer it from a different product family’s general description.

Wrapped conveyor belt rolls that require identification of reinforcement, cover and supplied form
A delivered roll must remain traceable to the approved mechanical and application requirements.

Coal belt substitutes must preserve the approved route identity

Coal-route substitutions should preserve both the construction and the required documents

A supplier may propose an alternative when the originally requested construction is not available for the desired delivery. Identify exactly what changes. A similar fabric name or FR description is not enough to establish equivalence. The responsible project team should compare the alternative with the approved mechanical duty and required fire-related evidence before accepting it.

If the offered document refers to a different cover or complete construction, obtain clarification of its applicability. Do not assume that a product family name connects every item in the range to the same result. The purchase record should let the buyer identify the actual belt and the evidence used for its approval.

For a distributor supplying several coal customers, keep site-specific requirements with each approved item. A certificate requested by one installation should not become a generic claim on every coal belt in stock. Likewise, a mechanically suitable roll should not be sent to a different environment before that customer’s actual acceptance requirements are checked.

Route revisions deserve the same attention. If the conveyor location, operating duty or retained equipment changes after the initial enquiry, update the specification before final approval. A nearly unchanged installed length can conceal a different mechanical or application requirement. Mark which route revision the offered belt serves.

Document control should support that practical identification rather than create an unrelated paperwork collection. Keep the offered construction, required evidence and final supply form together. The crew and receiving team need to be able to connect the delivered roll to the approved coal route without guessing from its external appearance.

Agree whether the order concerns an open length, completed loop or another defined form, and identify the joining responsibility. The final delivered length should account for that approved arrangement. Ask how the actual belt will be packed and handled at the site, without assuming stock availability, a standard reel or a guaranteed lead time.

At receipt, compare the supplied identification and documents with the approved construction. Inspect accessible surfaces and edges for damage under the agreed handling procedure. Where a required product document is missing or concerns a different item, resolve that mismatch before the belt is accepted for the intended route.

Give the coal belt supplier one coordinated requirement: the named route, approved mechanical construction, required fire-related evidence and defined delivery form. A valid offer answers all four. If the paperwork or construction belongs to another belt, retain the purchase hold on that item until the identity is clear.